Optimizing Order Fulfillment Velocity with Gravity Carton Live Storage
In modern e-commerce fulfillment, omnichannel distribution centers, pharmaceutical hubs, and automotive manufacturing lines, split-case picking accounts for upwards of 55% to 65% of total warehousing operational labor costs. Conventional static shelving forces human order pickers to travel excessive distances through miles of aisles, constantly navigating around replenishment forklifts and pallet jacks. A Carton Flow Racking System (also referred to across global logistics as a carton live storage or gravity roller rack) solves this critical bottleneck by replacing static decking with inclined roller or skate-wheel beds that harness natural gravity.
Manufactured with high-grade structural Q235B cold-rolled steel by Guangzhou Heda Shelves Co., Ltd., each carton flow level features precision roller tracks inclined typically between 2.5° and 5° (a 4% to 8% slope). Cartons, plastic totes, and bins are introduced from the rear replenishment aisle and smoothly glide toward the front picking face under controlled kinetic motion. As the frontline order picker removes the foremost carton, the trailing units automatically advance forward into position. This mechanical First-In, First-Out (FIFO) cadence eliminates pick-face stockouts, reduces picker travel paths by up to 75%, and completely segregates stock loading traffic from pick-and-pack workflow.
Recommended Configurations
Carton Flow Racking Architectures Engineered for Diverse SKUs
Different warehouse topologies, tote dimensions, and item velocities demand purpose-built gravity flow configurations. We manufacture four primary structural formats tailored to specific operational payloads and building volumes.
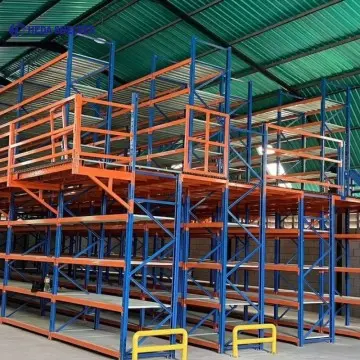
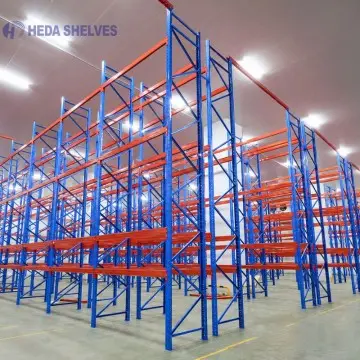
Combines high-density split-case carton picking at lower accessible tiers while maintaining multi-tier pallet storage reserves overhead on heavy structural beam levels.
Standard 50mm pitch beam adjustment
Direct drop-in roller track brackets
Pallet Rack Integrated Flow
Fast Fulfillment
Dedicated standalone dynamic shelving units with 3 to 7 tiers of roller tracks, ergonomic knuckle pick trays, and variable full-width divider guides for assembly lines and e-commerce pack hubs.
Polypropylene wheels or full-width steel rollers
Adjustable inclination angle from 2.5° to 6°
Standalone Modular Flow Racks
Maximum Density
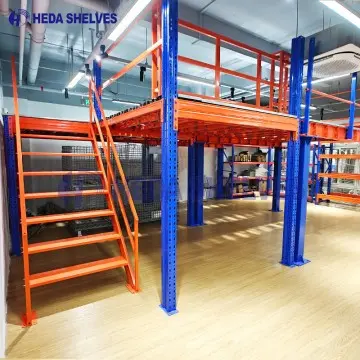
Integrates multi-level carton live beds into high-bay warehouses, creating 2 to 4 vertical working floors connected with integrated gravity chutes, spiral conveyors, and catwalks.
Multiplies vertical cubic storage area by 300%
Heavy structural mezzanine upright loading
Multi-Tier Flow Mezzanine
Industrial Kitting
Reinforced roll-formed steel channel tracks designed for manufacturing lineside kitting, storing heavy stamped steel bins, engine components, and casting totes up to 1,200 kg per bed level.
Precision zinc-plated steel ball-bearing rollers
Built-in mechanical end stop impact plates
Heavy-Duty Component Flow
Engineering Specifications & Structural Data
Technical Parameters: Carton Flow vs. Conventional Storage Media
Global supply chain directors require hard metrics before approving capital expenditure. The following comparative data highlights the technical boundaries and performance differentials across common picking architectures.
Specification Attribute
HEDA Carton Flow System
Static Longspan Shelving
Selective Pallet Picking Floor
Inventory Rotation Logic
Strict Mechanical FIFO (Gravity)
Typically LIFO (Manual Pushback)
Random Access / Mixed FIFO
Picker Travel Path Reduction
Up to 70% – 75% Reduction
Baseline (High walking fatigue)
Very Low (Wide forklift aisles)
Replenishment Interference
Zero (Separate Rear Loading Lane)
High (Same aisle blocks pickers)
Severe (Forklifts cross walking lines)
Floor Space Utilization
80% – 85% Active Storage Footprint
40% – 45% (Interspersed aisles)
35% (Demands wide reach truck lanes)
Standard Shelf Pitch & Gradient
2.5° to 5.0° (Engineered by package type)
Horizontal (0°)
Horizontal Floor Slab (0°)
Surface Pretreatment & Coating
Pickled, Phosphated & Electrostatic Powder
Basic Spray or Galvanized
Standard Liquid/Powder Paint
Market Intelligence & Forecasts
Future B2B Procurement Trends in Carton Flow Systems
Global supply chain disruptions, soaring logistics square footage leasing costs, and chronic warehouse labor shortages are shifting how multinational procurement executives source gravity flow systems.
Demand for Agility & Drop-In Modularity
Procurement teams are moving away from rigid, proprietary welded beds. Modern facilities require universally adjustable hanger brackets and snap-in roller tracks that can be reconfigured within minutes when SKU box dimensions evolve.
Resilient Protective Metallurgy
With increasing shipments into tropical coastal regions, cold chain facilities, and damp port zones across Africa and Southeast Asia, buyers now mandate strict multi-stage pickling and phosphating before electrostatic epoxy coating to prevent corrosion.
Landed Cost & Container Nesting
Ocean freight fluctuations make nested container packing critical. Guangzhou Heda Shelves Co., Ltd. designs precision knock-down profiles that maximize 40HQ container volumetric capacity, driving down the landed shipping cost per picking SKU location.
Technological Roadmap
Product Development Trends Shaping Next-Gen Carton Live Storage
Carton flow racking is evolving from passive metal shelving into a highly responsive, digitally integrated mechanical node within automated warehouse ecosystems.
Zero-Emission Passive Physics
As industrial facilities aim for carbon neutrality and contend with unstable power grids, carton flow requires zero kilowatt-hours of electrical energy. Gravity provides perpetual propulsion without motorized drives.
Pick-to-Light & Sensor Ready
Front knuckle trays and discharge beams are engineered with snap-in channels that protect fiber-optic Pick-to-Light (PTL) displays, barcode scanners, and wireless infrared carton detection sensors.
Autonomous Mobile Robot (AMR) Interfacing
Engineers design discharge presentation shelves with exact positional tolerances so that Autonomous Mobile Robots (AMRs) and automatic guided picking carts can dock and load totes without human handling.
Ergonomic Knuckle Pick Shelves
Angled discharge presentation trays (tilting outward by 15° to 20°) offer unobstructed visibility into open totes, drastically cutting worker bending strain and accelerating piece-picking cycle times.
Why Global Industrial Buyers Partner with Guangzhou Heda Shelves Co., Ltd.
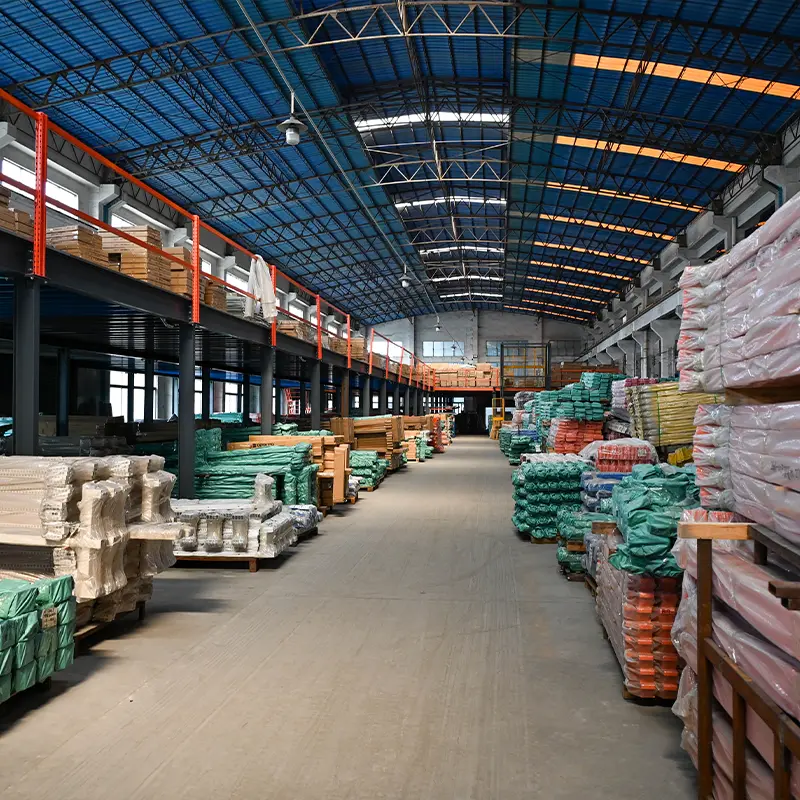
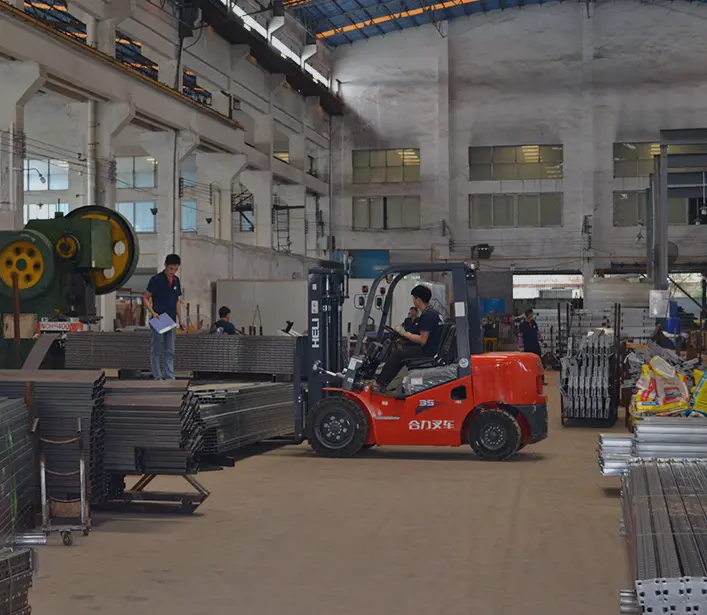
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international leader in heavy-duty warehouse racking and automated dynamic storage systems. Operating from our modernized 30,000 square-meter production headquarters in Guangzhou, China, we produce over 30,000 tons of structural cold-rolled steel racking monthly for clients across 120+ nations.
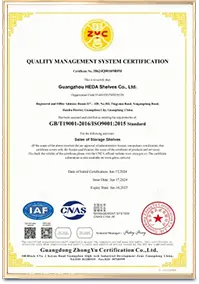
Every upright frame, support beam, connector bracket, and roller track channel is rolled, punched, welded, pretreated, and coated in-house under strict ISO 9001:2015 quality surveillance. When sourcing from Guangzhou Heda Shelves Co., Ltd., procurement teams work directly with senior structural design engineers—avoiding middlemen markups, receiving fully certified structural load calculations, and gaining complete accountability from coil to container.
25 Years ExperienceEstablished in 2001 with 10,000+ completed projects worldwide
Free 3D & CAD DesignComplimentary CAD floor plans, load analysis & 3D renders in 24 hours
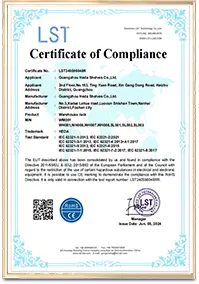
CE & ISO CertifiedCE No. 2435-CPR-8605159 and ISO 9001:2015 accredited production
Direct Export PackagingContainer-optimized knockdown bundling for fast ocean shipping & port customs
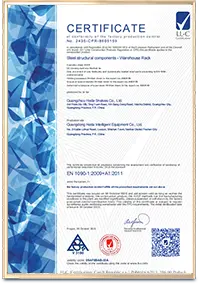
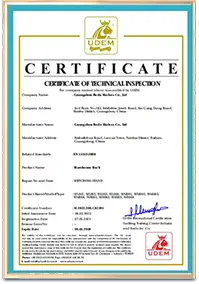
Project safety and building code verification are mandatory for enterprise supply chain contracts. Our carton flow racks and industrial storage solutions adhere strictly to global engineering standards.
CE Certification: No. 2435-CPR-8605159Certified European structural conformity for load performance
ISO 9001:2015 Management: No. 18624Q00169R0MAudited production process control valid through June 2027
What is the optimal incline slope angle for a carton flow roller track?
Standard engineering practice recommends an inclination angle between 2.5 degrees and 5.0 degrees, which translates roughly to an 8% gradient or a drop of 40mm to 50mm per meter of lane depth. The exact angle depends entirely on package contact dynamics. Rigid polypropylene plastic totes roll smoothly on lower inclines (2.5° to 3.5°), whereas corrugated cardboard cartons—especially those storing heavy or uneven internal contents that cause slight bottom deflection—require a steeper incline (3.5° to 5.0°) or closer roller center-to-center pitch. Guangzhou Heda Shelves Co., Ltd. supplies multi-position mounting brackets enabling quick pitch adjustment.
How does a carton flow system prevent cartons from getting stuck or colliding violently?
Flow reliability is controlled through three critical engineering parameters: wheel/roller pitch, lane dividers, and impact braking. We space rollers so that each carton is supported by at least three consecutive roller axles at all times to prevent sag. For long deep-lane tracks (exceeding 4 meters), integrated speed controllers and centrifugal brake rollers are installed along the track to regulate descending speed. At the discharge pick face, heavy gauge steel stop trays absorb impact energy without crushing carton edges.
Can carton flow tracks be retrofitted into our existing pallet racks?
Yes. Guangzhou Heda Shelves Co., Ltd. manufactures universal drop-in carton flow hanger brackets and customized shelf beds engineered to clamp directly onto standard step beams, box beams, or structural roll-formed profiles. This enables warehouse operators to upgrade their lower tiers into high-velocity split-case carton pick faces while keeping their upper beam levels for bulk reserve pallet storage, without purchasing entirely new upright frames.
What are the differences between plastic skate-wheel tracks and full-width steel roller tracks?
High-density plastic skate-wheel tracks (made of durable POM or high-impact polypropylene with aluminum alloy side frames) are lightweight, cost-effective, and provide exceptional flexibility for multi-lane configurations handling uniform plastic containers. Full-width zinc-plated steel rollers provide superior durability for irregular packaging, soft-bottom corrugated cartons, heavy automotive castings, and environments subject to rough impacts or temperatures ranging from -30°C cold storage to +50°C dry heat.
How much can carton flow racking reduce operational picking costs?
Time-motion industrial warehouse studies demonstrate that picking labor consists of roughly 60% walking, 20% searching, 15% physical retrieval, and 5% administration. By bringing all active pick faces to a single condensed pick line and physically separating replenishment stocking into the rear aisle, a carton flow racking system cuts worker walking and search travel by up to 75%. This frequently yields an operational return on investment (ROI) within 8 to 14 months of deployment.
How does Guangzhou Heda Shelves Co., Ltd. support global assembly and installation?
All carton flow units are manufactured with modular boltless drop-in connectors and labeled components. Every international consignment includes exhaustive CAD assembly schematics, component manifests, step-by-step video tutorials, and dedicated live remote technical video guice with our engineering team to ensure rapid, error-free on-site installation by your local workforce.
Consult a Senior Racking Engineer Get customized carton flow lane calculations, track pitch recommendations, and structural CAD blueprints tailored to your building parameters.
Direct Factory Collaboration
Request Your Complimentary 3D CAD Layout & Project Quotation
Share your carton dimensions, building clear heights, and throughput targets. Our engineering team at Guangzhou Heda Shelves Co., Ltd. provides a verified CAD layout and transparent factory-direct pricing within 24 hours.
 Heavy Hybrid