Engineered Warehouse Shelving & Industrial Racks
Discover high-load industrial rack architectures manufactured from cold-rolled Q235B/Q355B structural steel, tested to European FEM & EN standards for maximum structural reliability.
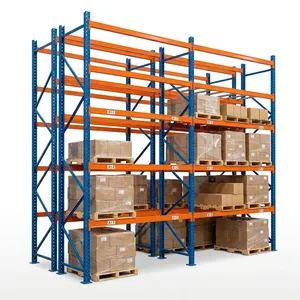
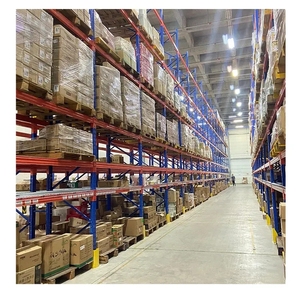
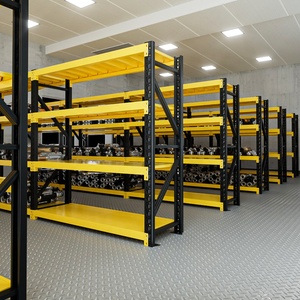
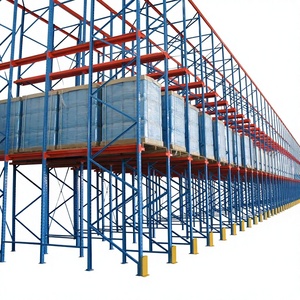
Engineering Standards for CE Certified Heavy-Duty Racking Systems
Modern warehouse logistics require structural storage solutions that balance extreme dead-weight tolerance, dynamic impact resistance, and maximum floor-space utilization. Procuring industrial warehouse shelving is a critical infrastructure decision that impacts workplace safety, compliance liability, and asset longevity. Certified manufacturers adhere strictly to European Norms (EN) including EN 15512 (Adjustable pallet racking systems – Principles for structural design), EN 15620 (Tolerances, deformations and clearances), and EN 15629 (The specification of storage equipment).
1. Metallurgy, Cold-Bending Forming, and Deflection Limit Criteria
The primary load-carrying frames of heavy-duty warehouse shelving are roll-formed from premium certified cold-rolled structural steel coils, primarily grades Q235B and Q355B (conforming to international standard structural equivalents S235JR and S355JR). The yield strength criteria ($f_y \ge 355\,\text{MPa}$) determine the resistance to micro-buckling and frame twisting under asymmetric seismic and impact loads.
In selective and high-bay drive-in racking frameworks, allowable vertical beam deflection is strictly capped at $\delta \le L/200$ (where $L$ is the clear span distance between upright columns) under full design working load. Upright columns feature continuous micro-pitch adjustability (typically 50mm or 75mm increments) cold-punched via multi-station automated hydraulic lines to maintain cross-sectional consistency without introducing micro-fractures along profile bends.
| Racking Architecture | Structural Steel Grade | Unit Bay Capacity | Aisle Clearance Req. | Primary Sector Application |
|---|---|---|---|---|
| Selective Pallet Racking | Q235B / Q355B Cold Formed | 1,000 kg – 4,500 kg / level | 3,000 mm – 3,400 mm | FMCG, General 3PL, Multi-SKU Distribution |
| Drive-In / Drive-Through | Heavy Q355B Structural | 1,200 kg – 2,000 kg / pallet | Forklift Entry Lanes | Cold Storage, Batch Food & Beverage |
| Radio Shuttle High-Density | Q355B Galvanized Rails | 500 kg – 1,800 kg / pallet | Single Transfer Aisle | Automated Buffer, Cold Rooms, Grain Hubs |
| Cantilever Rack Profiles | Hot-Rolled H-Section Steel | 500 kg – 3,000 kg / arm | Variable / Side-Loader | Timber, Steel Rebar, Long Extrusions |
| Multi-Tier Mezzanine Floors | Q235B Uprights + Steel Deck | 300 kg – 1,000 kg / m² | Stairwell & Pallet Gates | E-commerce Piece Picking, Auto Spare Parts |
2. Advanced Surface Passivation & Powder Coating Chemistry
Industrial warehousing environments frequently present aggressive ambient factors, including high humidity, marine salt mists in coastal ports, and temperature cycling in multi-temperature refrigeration facilities. Premium manufacturing incorporates an automated 8-stage pickling and phosphating pretreatment cycle that chemically degreases and strips iron oxides before electrostatically applying heavy-duty thermosetting epoxy-polyester powder coats.
Cured at 180°C to 200°C, the resulting cross-linked protective barrier achieves a continuous coating thickness of 60 to 90 microns ($\mu\text{m}$), demonstrating exceptional cross-hatch adhesion (DIN EN ISO 2409 Level 0) and salt-spray corrosion resistance exceeding 500 hours (ASTM B117). For sub-zero cold rooms (-30°C) and semi-open loading docks, hot-dip galvanization (ISO 1461) provides zinc-alloy metallurgical bonding that permanently suppresses oxidation creep.
Future Trends in Warehouse Shelving Procurement (2025–2030)
Forward-thinking supply chain directors and facility managers must evaluate long-term shifts in materials handling, automation interfaces, and environmental regulations when deploying storage capital.
1. Autonomous AGV/AMR Interface Compatibility
As distribution networks automate, standard manual racking is transitioning to robotic-ready layouts. Modern upright baseplates and lower guide rails are now engineered to integrate optical path reflectors, floor QR-grid fiducials, and millimeter-level tolerances required by Autonomous Mobile Robots (AMRs) and automated stacker cranes (AS/RS).
2. Decarbonization & Circular LCA Procurement
Corporate ESG mandates require verified Product Carbon Footprint (PCF) disclosures for structural warehouse steel. Procurement teams prioritize suppliers employing electric arc furnace (EAF) steel with recycled scrap inputs, non-toxic heavy-metal-free powder chemistries (RoHS compliant), and demountable boltless components engineered for secondary re-use.
3. Volumetric Freight Optimization (KD Shipping)
Volatile ocean freight and landed costs dictate modular Knock-Down (KD) hardware architectures. Forward-looking shelving systems are engineered to nest tightly into 40-foot High Cube (40HQ) sea containers, achieving up to 26–28 metric tons of volumetric density without wasted headspace or risk of transit bending.
Enterprise Strengths: Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a global leader in designing, engineering, and manufacturing heavy-duty industrial shelving, pallet racking, and structural mezzanine platforms.
Operating from a vertically integrated 30,000 square meter manufacturing base in Guangzhou, China, our team of over 300 experienced engineers, structural designers, and certified welders controls every millimeter of the supply chain. From high-grade raw steel slitting to automatic cold-roll forming, robotic welding, surface passivation, and automated packaging, all processes occur in-house to guarantee flawless structural repeatability.
Our facility operates under ISO 9001:2015 Quality Management Certification (Certificate No. 18624Q00169R0M) and holds official European CE Conformity Certification (No. 2435-CPR-8605159) alongside RoHS compliance credentials. We provide comprehensive OEM/ODM partnerships, enabling global importers, engineering procurement contractors (EPCs), and logistics brands to customize upright profiles, hole-pitch designs, powder coating RAL colorways, and safety accessories to precise regional market codes.
Our 10-Stage Precision Manufacturing Process
Raw Material Inspection
Mill certificate validation, ultrasonic flaw detection, and tensile yield testing of incoming Q235B/Q355B coil steel.
Precision Slitting
Automated uncoiling and CNC longitudinal shearing to micro-tolerances for upright and beam profile feeds.
CNC Hole Punching
Continuous hydraulic stamping of teardrop, butterfly, or diamond pitch holes with zero mechanical burrs.
Cold Roll-Forming
Multi-stand continuous roller profiling forming rigid Omega ($\Omega$) upright profiles with 8+ load-bearing folds.
Profile Interlocking
High-frequency seam closing and box-beam step interlocking to ensure structural torsional stability under dynamic loads.
Robotic Welding
Multi-axis automated pulse-MIG welding joining beam end-connectors with deep, porosity-free weld penetration.
Mechanical Polishing
Shot blasting and edge de-burring to remove slag, preparing steel micro-surfaces for uniform chemical bonding.
Pickling & Phosphating
Automated 8-tank chemical dipping to strip oil, acid-etch surface scale, and deposit an anti-rust phosphate film.
Powder Coating
Electrostatic application of non-toxic epoxy-polyester powder baked at 200°C for superior impact resilience.
QA & Containerization
Thickness gauging, batch load-press testing, component numbering, and cushioned bundle packing for export.
Frequently Asked Questions on Heavy-Duty Shelving Procurement
Direct answers from our senior engineering group addressing common technical hurdles, certification protocols, and international shipping logistics.
What specific technical data is required to calculate load ratings and structural drawings?
How does CE certification (EN 15512) protect buyers compared to non-certified shelving?
What surface treatment is best for humid maritime ports or cold-chain storage?
How do you optimize container packing to reduce international ocean freight costs?
Can local warehouse crews perform the installation, and what documentation is provided?
What is the standard production lead time and factory warranty coverage?
Optimize Your Warehouse Footprint Today
Send your building dimensions, clear roof heights, and pallet specifications. Our certified structural engineers will deliver a comprehensive 2D CAD layout, 3D visualization, and structural load analysis within 24 hours.