Engineered Industrial Racking & Unit Load Solutions
Precision-manufactured selective, dynamic gravity flow, and dense automated systems certified under European and International quality benchmarks.
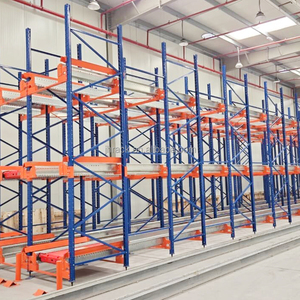
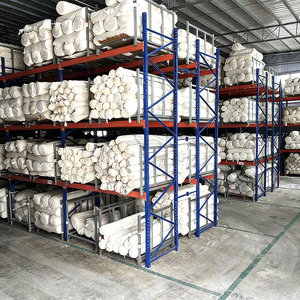
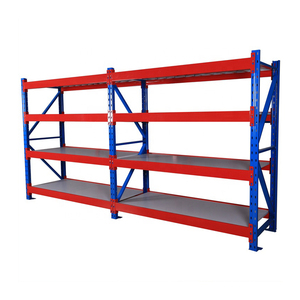
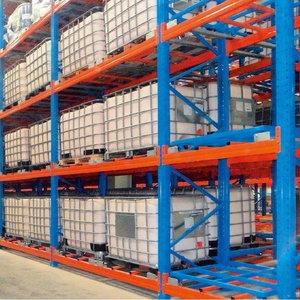
Engineering Mechanics of High-Density Carton Flow Systems
Carton flow racking systems operate on an unpowered dynamic principle: gravity-driven inclined roller tracks or skate-wheel tracks feed split-case and full-carton merchandise seamlessly from an intake (loading) aisle to an extraction (picking) aisle. By maintaining an inclination gradient between 2.5% to 5.0%, cartons glide downstream at controlled velocities, eliminating operator deadhead travel and enforcing strict FIFO (First-In, First-Out) inventory rotation.
Constructed utilizing certified structural Q235B cold-rolled carbon steel, our upright frames deliver high shear and flexural rigidity. Cold-formed intermediate tracks leverage engineered polycarbonate or steel skate wheels mounted along heavy-gauge galvanized channels, ensuring sustained resilience against dynamic shock loads common to fast-moving distribution hubs, e-commerce fulfilment centres, and automotive assembly lines.
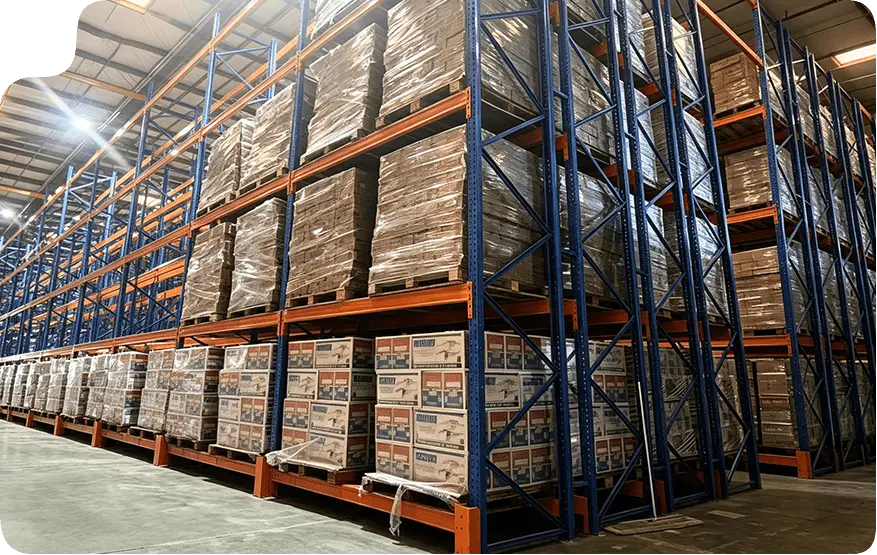
Future Procurement Trends in Carton Flow & Dynamic Storage
In-depth insights into global supply chain redesigns, lean picking automation, and total cost of ownership (TCO) benchmarks shaping cross-border rack procurement.
Pick-to-Light & AMR Integration
Procurement criteria have transitioned from static track shelving to modular architectures that integrate directly with Pick-to-Light (PTL) sensor profiles and Autonomous Mobile Robots (AMRs). Future-ready carton flow tracks are pre-drilled to host cabling channels, wireless pick-sensors, and optical verification brackets without requiring field hot-work.
Variable Slope & Universal Wheel Tracks
Due to shifting consumer packaging from rigid corrugated boxes to sustainable recycled tote bins and polybags, procurement teams increasingly favor full-width steel roller tracks and adjustable drop-in dividers over rigid, fixed-width skate-wheel tracks. This flexibility eliminates lane redesign expenditures when SKU dimensions fluctuate.
Micro-Fulfilment & Multi-Tier Mezzanines
Urban real estate constraints require vertical space optimization. Global operations are transitioning from single-floor manual picking lanes to rack-supported multi-tier mezzanine picking towers with integrated carton flow levels, reducing picking footprints by up to 65% while multiplying SKU density per cubic metre.
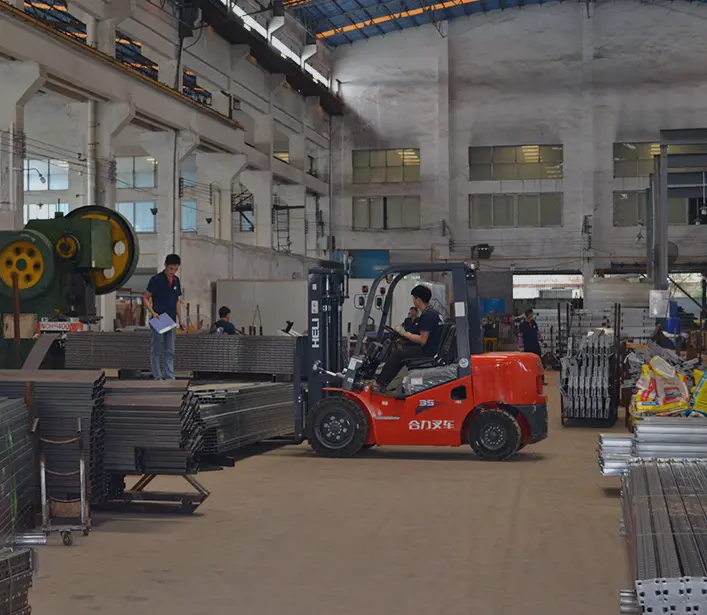
Guangzhou Heda Shelves Co., Ltd. Manufacturing Infrastructure
Operating a modernized 30,000 m² heavy-industrial production facility in Guangzhou, China, HEDA Shelves enforces vertical manufacturing integration. From cold-roll profile extrusion and automated multi-station punching to pickling, phosphating, and automated electrostatic powder coating, all engineering phases are monitored under stringent ISO 9001:2015 quality standards.
Holding validated CE Certification (Certificate No. 2435-CPR-8605159) and RoHS compliance, our structural designs align strictly with EN 15512 European standards and RMI (Rack Manufacturers Institute) deflection limits. Our dedicated structural engineering team provides custom 3D CAD modeling, finite element stress analysis, and load-bearing verification to ensure structural integrity across seismic, ambient, and temperature-controlled facilities.

1. Certified Steel Stock

2. CNC Precision Cutting

3. Automated Punching

4. Continuous Roll-Forming

5. Polymer Powder Coating
Frequently Asked Questions on Carton Flow Racking Procurement
Authoritative technical guidance compiled by senior warehouse design engineers to facilitate informed capital expenditure decisions.
What is the optimum pitch or slope angle for industrial carton flow tracks?
Can carton flow beds be retrofitted into existing selective pallet rack systems?
How does HEDA prevent corrosion during high-humidity ocean shipping and in coastal facilities?
What are the maximum load ratings supported per shelf level in carton flow racks?
What documents and design specifications are required to receive a customized 3D CAD layout?
Accelerate Your Order Picking Efficiency Today
Partner directly with an established ISO 9001 and CE certified manufacturer. Request our comprehensive carton flow technical catalog, sample roller profiles, and full structural layout support.
Get Catalog