High-Density Storage & Industrial Racking Portfolios
Explore our certified heavy-duty storage product lines engineered with premium high-yield steel coils, custom-stamped upright geometries, and rigorous automated quality assurance standards.
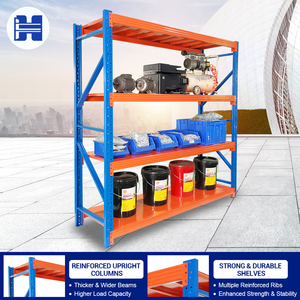
200kg Modular Metal Frame Garage & Parts Storage Shelf
Boltless interlocking assembly designed for small-parts organization, maintenance workshops, and light-industrial picking bays.
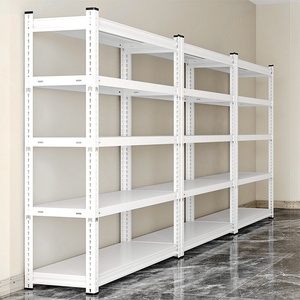
Heavy Duty Adjustable Industrial Warehouse Pallet Racking
Electrostatic epoxy-coated heavy beam shelving supporting up to 3,000kg per level, engineered for harsh logistics terminal operations.
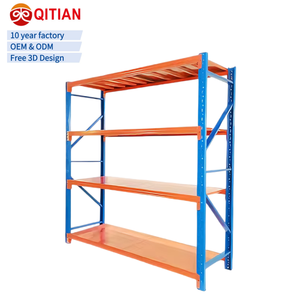
200kg 4-Tier Anti-Rust Boltless Steel Warehouse Storage Rack
Cold-rolled Q235 steel construction featuring pickling and phosphating pre-treatment for superior humidity resistance.
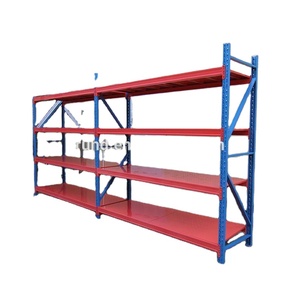
300kg Industrial Metal Iron Stacking Racks & Shelves
Flexible modular stacking post pallets engineered to eliminate structural aisle loss for seasonal crop and bulk staging demands.
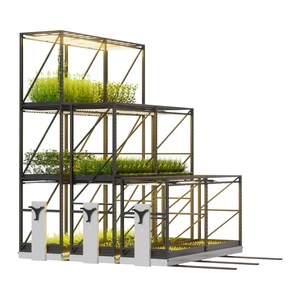
High-Density Movable Vertical Compactor Racking System
Precision-guided track mobility that compresses storage footprints by 50% for indoor agricultural and high-density archives.
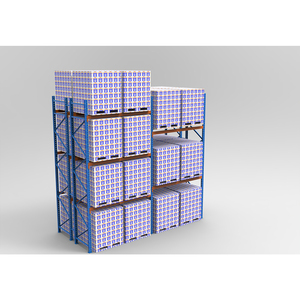
Double Deep 6-Meter High Heavy Duty Pallet Racking
Specialized deep-reach configuration balancing high pallet density with rapid multi-bay reach truck accessibility.
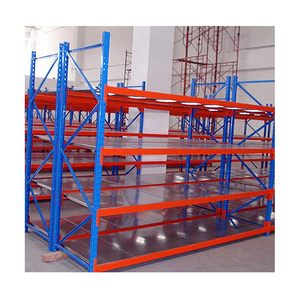
Selective Heavy Duty Vertical Steel Pallet Racking System
100% immediate individual pallet selectivity with multi-tier vertical flexibility conforming to FEM 10.2.02 and EN 15512 codes.
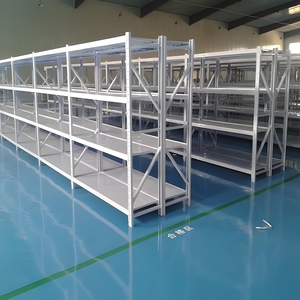
Medium Duty Longspan Industrial Metal Storage Shelving
Versatile step-beam profile with heavy steel decking inserts, ideal for manual fulfillment distribution centers and intermediate parts storage.
Structural Anatomy of High-Density Drive-In Racking Systems
Drive-In and Drive-Through racking configurations represent the most cost-effective solution for high-density pallet consolidation, capable of reclaiming up to 75% to 85% of dead aisle space compared with conventional selective pallet racking. Engineered specifically for homogeneous stock with low SKU variations and massive pallet throughput, the architecture eliminates intermediate forklift operating aisles by allowing standard counterbalanced or narrow-chassis reach trucks to drive directly into the racking storage lanes.
Unlike standard cross-beam racks, pallets in a Drive-In system rest directly upon continuous structural cantilever support rails mounted to one-piece formed arm brackets. The structural frames are subjected to both horizontal dynamic impact forces and vertical dead weights, necessitating strict engineering calculations according to EN 15512 and RMI MH16.1 specifications. To prevent structural lateral drift and progressive frame collapse, a certified Drive-In structure integrates rigid top portal tie beams, horizontal top bracing trusses, and rear vertical cross-bracings (in single-entry LIFO systems).
| Component | Engineering Material | Design Criteria |
|---|---|---|
| Upright Columns | Q235B / Q355B Cold-Formed Steel | 55–120mm web profile, 1.8–3.0mm gauge thickness |
| Cantilever Support Arms | Heavy Stamped Steel (Single/Double) | Welded double-lug engagement, high moment resistance |
| Pallet Guide Rails | Continuous Roll-Formed Galvanized Steel | Flanged load lip with integrated entry lead-in funnels |
| Ground Floor Guide Tracks | Structural Angle / Embedded Channel | Absorbs truck steering shock, prevents column collision |
| Top Tie Portal Beams | Box Beam / Interlocking Twin C-Beam | Resists longitudinal torsion and lateral seismic shear |
LIFO vs. FIFO Rotation Mechanics
Drive-In operations leverage Last-In, First-Out (LIFO) inventory cycles via single-side entry, making them ideal for cold-storage blast freezers, raw materials, and seasonal goods. Drive-Through configurations utilize dual entry portals to establish true First-In, First-Out (FIFO) batch management across food, dairy, and beverage distribution lines.
Impact Protection & Floor Anchorage
Because forklifts maneuver inside the rack matrix, structural columns are vulnerable to mast bumping. HEDA reinforces front uprights with wrap-around anchor guards, heavy-gauge rubber-cushioned deflectors, and continuous floor-mounted guide rails that mechanically channel forklift tires with 100mm precision tolerance.
Cold Storage & Blast Freezer Optimization
Refrigerated warehouse space costs up to 4.5 times more to operate than ambient space. Drive-In racking compresses thermal volume, minimizes unused air pockets, and utilizes special low-temperature epoxy powder formulations or ISO 1461 hot-dip galvanization to resist embrittlement at operational temperatures down to -35°C.
Guangzhou HEDA Shelves: 25+ Years of OEM/ODM Excellence
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates a state-of-the-art 30,000 m² heavy-duty racking fabrication base in Guangzhou, delivering certified structural warehouse systems to over 120 nations worldwide.
10-Stage Precision Manufacturing & Pre-Treatment Process
Every structural Drive-In upright, beam, and cantilever rail undergoes complete internal lifecycle fabrication to ensure metallurgical integrity and millimeter-accurate slot pitching.

Certified Raw Steel Coils

CNC Precision Slitting & Cutting

Multi-Station Pitch Punching

Precision Cold Bending Forming

Continuous Roll Profile Forming

Automated Polishing & Deburring

Robotic Gas-Shielded Welding

Pickling & Phosphating Wash

Electrostatic Powder Coating

QC Deflection & Container Shipping
Future Procurement Trends in High-Density Warehouse Racking
Strategic supply chain leaders are shifting procurement criteria from simple per-pallet hardware costs to lifecycle structural resilience, green logistics compliance, and automation readiness.
Total Cost of Ownership (TCO) vs. Initial CapEx
Modern B2B buyers now calculate the 10-year Total Cost of Ownership rather than immediate material invoice costs. Procurement contracts increasingly evaluate upright steel yield strength (e.g., Q355B vs standard mild Q235), certified paint scratch resistance to prevent coastal corrosion, and replaceable bolted upright insert shoes that slash localized repair downtime by 80% without dismantling entire bays.
Container Freight Optimization & Knock-Down Geometry
With volatile maritime shipping rates between Asia, the Middle East, Africa, and the Americas, structural engineering must integrate container packaging algorithms. HEDA utilizes nested cold-formed upright profiles and detachable cantilever arms, elevating 40HQ container volumetric pack efficiency to over 95% and lowering landed freight cost per pallet location by up to $18–$25 per position.
Hybrid Retrofit Architecture (Shuttle Readiness)
Forward-thinking supply chain directors demand modular systems capable of evolving from standard manual forklift Drive-In lanes to semi-automated Radio Shuttle operations. HEDA's proprietary pallet rail geometry supports retrofittable drop-in shuttle runners, allowing enterprises to automate high-velocity storage bays in phased capital deployment stages without tearing down vertical steel frames.
Seismic Compliance & Non-Linear FEM Modeling
Stringent building codes (including Eurocode 3, EN 15512, and US RMI MH16.1) now mandate finite element structural modeling of pallet racks under dynamic seismic loads. Procurement teams increasingly reject generic fabricators in favor of OEM factories possessing in-house finite element software capable of verifying structural safety under regional seismic accelerations up to 0.4g.
Engineering Trajectory: Material Innovation & Smart Diagnostics
The convergence of advanced metallurgical alloys, automated robotic fabrication, and structural health sensors is redefining reliability standards in heavy industrial storage.
Advanced Metallurgical & Mechanical Developments
- Ultra-High-Strength Micro-Alloyed Steels: Transitioning to cold-rolled micro-alloyed boron and manganese steels achieves yield strengths above 420 MPa, allowing for lighter column profiles that withstand higher torsional dynamic shear without buckling.
- Dual-Stage Electrostatic Thermosetting Powders: Applying heavy zinc-rich primer baths underneath TGIC-free polyester powders ensures 1,000+ hours of continuous salt-spray corrosion resistance (ASTM B117), critical for humid maritime distribution hubs.
- Low-Friction UHMW-PE Guide Liners: Integrated ultra-high-molecular-weight polyethylene wear strips mounted to steel pallet runners reduce pallet friction coefficients, virtually eliminating timber slivers and pallet jamming during forklift extraction.
- Digital Twin & IoT Deflection Telemetry: Pilot projects utilize wireless piezoelectric strain gauges embedded inside critical portal tie joints to broadcast real-time structural overload alerts directly to warehouse management software (WMS).
Custom OEM/ODM Engineering: Tailoring Systems to Operational Realities
No two warehouse logistics topologies are identical. As a dedicated OEM/ODM manufacturer, Guangzhou Heda Shelves adapts Drive-In systems to non-standard inventory specifications. Whether dealing with irregular four-way entry wooden pallets, plastic beverage skid configurations, chemical drums on secondary spill basins, or steel bins, our engineering design team delivers tailored CAD arrangements that guarantee structural equilibrium.
Our bespoke engineering capabilities extend to structural anchor optimization. Depending on your building slab's concrete compressive strength (e.g., C20/25 to C35/45) and rebar placement, HEDA calculates custom expansion anchor depths or resin-bonded chemical anchor arrays to prevent catastrophic floor spalling under heavy operational cyclic loads.
Frequently Asked Questions on Drive-In Racking Procurement
Comprehensive engineering, operational, and commercial answers written by HEDA's Senior Warehouse Systems Directors.
What warehouse slab specifications are required for heavy Drive-In systems?
How do Drive-In systems withstand severe -30°C cold storage temperatures?
What are the critical clearance tolerances between forklifts and Drive-In lanes?
Why is top and rear bracing structurally mandatory in Drive-In configurations?
How does HEDA Shelves protect knock-down components during ocean transit?
What international manufacturing and structural certifications does HEDA hold?
What is the typical production lead time for an OEM/ODM Drive-In project?
Can Drive-In racking be installed by local warehouse contractor crews?
Request a Free 3D CAD Warehouse Layout & Structural Calculation
Collaborate directly with our senior racking structural engineers. Submit your warehouse architectural layout, pallet dimensions, and forklift lift profile to receive a complimentary load capacity analysis and cost optimization blueprint within 24 hours.
- Free 2D/3D CAD Layout Blueprints
- CE & ISO 9001:2015 Structural Compliance
- Direct 30,000 m² Factory Wholesale Pricing
- Container Packaging & Ocean Freight Optimization
Start Your Project Consultation
Speak with our technical engineering division now to discuss structural parameters, lead times, and factory-direct commercial terms.
Get a Quote