Featured OEM/ODM Movable & High-Density Racking Systems
Direct factory fabrication engineered for maximum volumetric density, dynamic ground load distribution, and rapid forklift cycle efficiency across global logistics hubs.
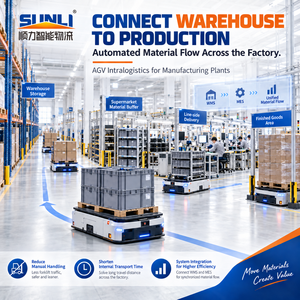
SUNLI Pallet AS/RS Smart Warehouse Automated Storage And Retrieval System With WMS/WCS Stacker Crane Racking
- Payload:500 - 2,500 kg/pallet
- Drive:Automated Stacker / Shuttle
- Standard:FEM 9.831 / EN 528
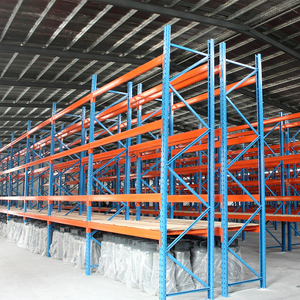
Industrial Rack Manufacture Heavy Duty Adjustable Steel Storage Shelving Rack For Warehouse Stacking
- Bay Load:Up to 4,500 kg/level
- Upright:Cold-rolled Q235B / Q355B
- Pitch:50mm / 75mm Adjustable
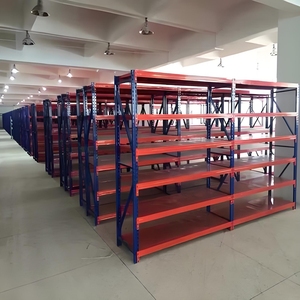
Adjustable 5-Layer Steel Metal Stacking Racks & Shelves Anti-Rust Efficient Warehouse Storage Solution
- Capacity:800 - 1,200 kg/tier
- Pretreatment:9-Stage Zinc Phosphating
- Finish:Powder Coat 80-120μm
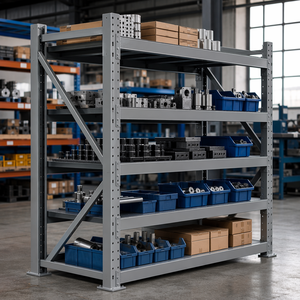
Custom OEM Storage Rack Frame | Heavy Duty Steel Welded Fabrication for Warehouse Pallet Racking
- Material:Certified High-Yield Steel
- Welding:Robotic CO2 Shielded Arc
- Custom:Custom Section Depths
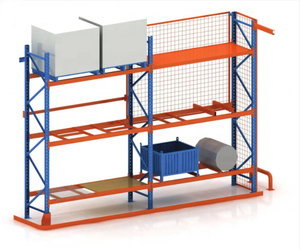
Mobile Base Movable Selective Pallet Rack System Flexible Layout Industrial Storage Space Optimization
- Space Gain:+85% Pallet Capacity
- Mobility:Motorized Chassis / Guide Rail
- Safety:Photoelectric Optical Barriers
Industrial Stacking Racks Shelves-Mobile Durable Alloy Steel 15000kg Load Capacity Storage System
- Total Stack:15,000 kg Rated Tier
- Interlock:Forged Cup Post Alignment
- Flexibility:Forklift Transportable
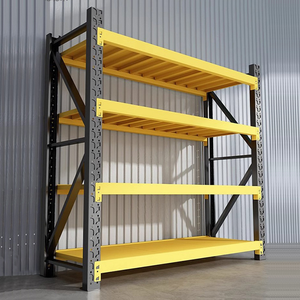
Warehouse Storage Stacking Movable Metal Steel Truck Tire Post Pallet Tyre Stillage Racking
- Application:Radial & OTR Tire Cargo
- Feature:Fold-Flat Knockdown Design
- Stack Height:4 - 6 Units High
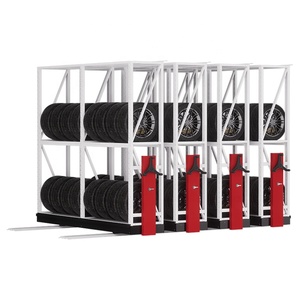
Compact Mobile Cabinet Steel Manual Mass Shelving System for High-Density Movable Racking
- Mechanism:Mechanical Assist / Handwheel
- Track:Flush-Embedded Steel Rail
- Use Case:Automotive & Heavy Archives
Engineering Architecture & Load Dynamics of Movable Warehouse Racking
Understanding the mechanical, structural, and electrical interlocking principles that transform static warehouse footprint into dynamic high-density storage space.
Sub-Floor Rail Geometry & Leveling Tolerance
Movable pallet racks transmit concentrated dynamic wheel loads up to 120 kN per wheel directly to concrete foundation slabs. High-precision cold-drawn steel rails (C45 or 42CrMo) are recessed into the concrete floor using adjustable leveling plates anchored with epoxy chemical anchors.
Heavy Motorized Bogies & Synchronized Drive
Each mobile base unit is fabricated from heavy structural rectangular box beams fitted with forged steel travel wheels. Decentralized helical gear-motors with Variable Frequency Drives (VFD) guarantee smooth acceleration and soft-stop decelerations, eliminating pallet slippage or inertia tilt.
Dual-Zone Optical Safety & Emergency Braking
Safety systems conform to European standard EN 15095 for power-operated movable shelving. Continuous infra-red light barriers create an optical perimeter at floor level and pedestrian chest height. If any obstacle breaks the beam, mobile bases halt in under 250 milliseconds.
High-Density Warehouse Systems: Comparative Technical Analysis
Comparing space utilization, operational selectivity, capital expenditure (CAPEX), and cold store thermal savings.
| Racking Architecture | Floor Space Utilization (%) | Direct Pallet Accessibility | Cycle Picking Speed | Cold Store Energy Savings | Relative CAPEX / Position |
|---|---|---|---|---|---|
| Motorized Movable Pallet Racks | 85% – 90% (Ultra High) | 100% (Individual Aisle Open) | Moderate (Aisle opens in 25-35s) | 40% – 50% Reduction | Moderate - High |
| Standard Selective Racking | 40% – 45% (Low - Static Aisles) | 100% (Instant Direct Access) | High (Free Forklift Passage) | Baseline Reference (0%) | Economical (Low) |
| Drive-In / Drive-Through Rack | 65% – 75% (High Density) | Low (LIFO / FIFO Bulk Lane) | Slow (Forklift enters rack lane) | 20% – 25% Reduction | Moderate |
| Radio Shuttle Cart Racking | 75% – 85% (High Density) | Batch Selective (FIFO / LIFO) | High (Cart runs internally) | 30% – 40% Reduction | High |
| Very Narrow Aisle (VNA) | 55% – 60% (Moderate High) | 100% (Turret Truck Needed) | High (Wire-guided transit) | 10% – 15% Reduction | Moderate - High |
Future Procurement Trends in Movable Warehouse Racking
Strategic procurement officers are shifting from static storage procurement to dynamic space-saving capital assets driven by soaring industrial land lease rates and strict ESG climate standards.
Urban Industrial Land Inflation
With prime logistics real estate in port regions and city peripheries commanding historical price peaks, logistics operators cannot afford to allocate 60% of their floor plate solely to forklift transit lanes. Motorized movable racking consolidates 8-12 aisles into 1 single floating working aisle, slashing real estate footprint requirements by half without sacrificing inventory SKU direct accessibility.
Cold Chain Thermal Efficiency
Cold storage warehouses operating at -20°C to -35°C consume exorbitant electrical power to cool dead ambient airspace. Movable racks allow cold store operators to double pallet storage capacity within the identical refrigerated building volume, lowering cooling refrigeration power expenditure per pallet position by 35% to 50%, guaranteeing faster capital investment payback.
AMR & AGV Fleet Integration
Procurement teams are prioritizing dynamic movable racking with standardized API, OPC-UA, and dry-contact relay interfaces that link directly with automated Warehouse Management Systems (WMS). Automated Guided Vehicles (AGVs) communicate with mobile racks wirelessly to open designated pick-aisles automatically upon approach, eliminating operator idle times and streamlining automated picking cycles.
Container-Optimized Knockdown Freight
Surging international sea freight costs mandate clever boltless, modular knockdown racking profiles. Global buyers require racking designs where structural upright columns, horizontal bracing, box beams, and motorized bogies nest flat into 40HQ sea containers, boosting container cube utilization by over 40% and drastically reducing landed cost per pallet location.
Technological Innovations in Movable Racking Engineering
From variable torque synchronization to algorithmic aisle night-parking routines, modern mobile storage systems have evolved into sophisticated automated mechatronic platforms.
Intelligent Variable Frequency Speed Profiling
Early mobile racks experienced mechanical jerks during startup and braking, risking load displacement. Contemporary OEM motorized platforms utilize multi-axis synchronized frequency inverters that execute customized S-curve motion profiles. Acceleration and deceleration curves are managed dynamically based on onboard weight sensors, ensuring 100% vibration-free traversal even under maximum 800-ton aggregate block loads.
Night Parking & Cold Circulation Modes
During off-peak hours or facility shutdown, the rack control system activates an automatic "Night Parking Mode." Racks automatically distribute themselves across the floor with uniform 300mm air circulation gaps between each mobile block. In cold storage facilities, this eliminates thermal pockets, prevents frost buildup, and balances air conditioning airflow without requiring manual human intervention.
Anti-Seismic Overhead Lock & Floor Dampers
Installing mobile racks in high-risk seismic zones (PGA > 0.3g) historically raised safety concerns. Modern high-density engineering integrates seismic shock-absorbing floor track dampers, anti-derailment double-flanged guide wheels, and optional automatic mechanical overhead locking claws that latch opposing rack tops together when seismic P-wave sensors detect initial underground tremors.
Guangzhou HEDA Shelves: 25 Years of Precision Storage Manufacturing
Founded in 2001, Guangzhou HEDA Shelves operates a specialized 30,000 square meter industrial manufacturing base. With vertically integrated roll forming, laser cutting, automated robotic welding, and internal 9-stage phosphating finishing lines, we engineer heavy movable systems for industrial distributors across 120+ countries.
In-House Structural Engineering
Our team of over 30 structural engineers delivers custom CAD layout design, full 3D visual renderings, and structural finite element analysis (FEA) load calculation reports compliant with EN 15512 and RMI specifications before manufacturing commences.
Pretreatment & Anti-Corrosion Defense
Steel profiles undergo automated pickling, degreasing, and a 9-stage zinc-iron phosphating immersion bath before electrostatic powder coating. This prevents coastal corrosion, peeling, and rust creeping, meeting demanding ASTM B117 salt spray standards for humid and cold room climates.
Audited Global Certifications
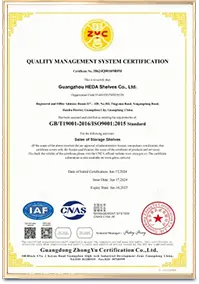
Guangzhou HEDA Shelves maintains independently verified compliance: European CE Certification No. 2435-CPR-8605159, ISO 9001:2015 Quality Management Certification No. 18624Q00169R0M (valid through June 2027), and strict RoHS raw material verification.
Our 10-Stage Quality-Controlled Fabrication Process
Prime Steel Inspection
Certified Q235B/Q355B coils verified via tensile & chemical spectrometry.
Precision Slitting
High-speed CNC slitting lines trim coil margins within ±0.1mm tolerance.
Automated Punching
Continuous mechanical punch press lines stamp 50mm/75mm diamond pitch holes.
Multi-Pass Roll Forming
Cold-roll forming through 18-24 rollers ensures zero residual stress.
Robotic Laser & Cut
Fiber laser cutting machines chamfer beam connectors and baseplate tabs.
Robotic Arc Welding
CO2 shielded automated robot cells execute deep weld penetration on connector brackets.
9-Stage Bath Phosphating
Complete immersion cleaning, derusting, acid pickling, and protective phosphating.
Electrostatic Coating
Swiss Gema automatic spray guns apply heavy epoxy powder cured at 200°C.
Deflection Testing
Sample beam batches undergo 1.5x proof loading to verify L/200 deflection limits.
Flat Container Packing
Knockdown components are strapped with steel bands and dunnage for damage-free transit.
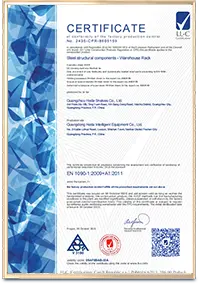
CE Cert No. 2435-CPR-8605159
ISO 9001:2015 Quality Verified
Structural Deflection Compliance
RoHS Compliant Finishing
Frequently Asked Questions for Movable Racking Procurement
Straightforward engineering answers on slab requirements, retrofitting, seismic safety, and international container delivery.
Can motorized movable racking be installed on existing warehouse concrete floors?
1. Flush-Channeled Installation: 150mm wide x 120mm deep floor channels are diamond-sawed into the existing slab. Track rails are set on adjustable leveling bolts, laser-aligned, and backfilled with high-strength non-shrink grouting mortar (60+ MPa compressive strength). This leaves the floor totally smooth for standard counterbalanced forklifts.
2. Surface-Mounted Ramped Track: For leased premises where trenching is prohibited, low-profile guided rails are anchored on top of the concrete, accompanied by chamfered aluminum or steel approach ramps.
What floor leveling tolerances are strictly required for heavy mobile racking?
How do mobile racking systems operate during sudden utility power failures?
• Manual Ratchet Drive: Every motorized bogie includes a dedicated mechanical hex-drive socket allowing operators to move carriages manually using a mechanical hand ratchet bar during emergencies.
• Auxiliary Battery Backup (UPS): Optional onboard 24V battery systems maintain optical safety circuits, PLC state memories, and brake release mechanisms.
• Generator Integration: Master control panels are equipped with automatic transfer switch (ATS) inputs for immediate emergency generator startup.
How does mobile racking withstand sub-zero cold room environments?
• IP65/IP67 rated gearmotors packed with synthetic low-temperature food-grade grease rated to -45°C.
• Internal thermal trace heaters in PLC and electrical cabinets to prevent condensation during defrosting cycles.
• Cold-impact resistant structural steel (Q355D/E) that eliminates brittle-fracture risks.
• Heavy-duty siliconized optical cabling designed to resist stiffening and cracking during flex cycles.
What are typical OEM/ODM lead times and container loading specifications?
Every shipment is optimized for knockdown flat packing: structural upright frames are transported fully bolted or knock-down nested, beams are strapped in wood-cushioned bundles with corner protectors, and motorized bogies are packed inside steel-reinforced maritime crates. A typical 40HQ container accommodates 22 to 26 metric tons of certified racking steelwork.
What design inputs are required from the buyer to generate a free layout and load calculation?
1. Building CAD DWG: Length, width, clear height beneath roof trusses, and column spacing grids.
2. Pallet Unit Parameters: Length x Depth x Height, plus gross pallet weight (including overhang).
3. Forklift Equipment: Model, maximum mast reach height, turning radius, and aisle width requirement.
4. Throughput & SKU Count: Total pallets to house, daily pallet turnover rate, and FIFO vs LIFO priority.
Ready to Double Your Warehouse Storage Density?
Consult directly with HEDA Shelves senior structural racking engineers. Submit your warehouse floor plan today for a complimentary 3D layout design, finite element load calculation, and factory-direct quotation.