800kg Load
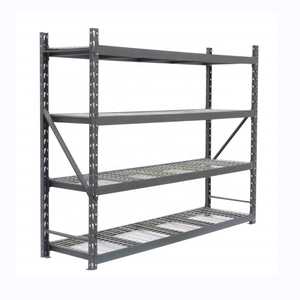
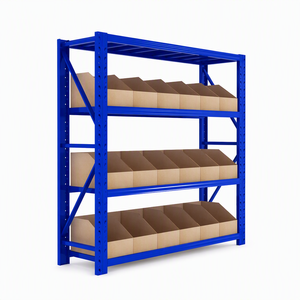
KINDE Steel Rack Heavy Duty Industrial Fruit Rack Warehouse Storage Pallet Racking 800kgs
- Perforated upright post profile
- Cold-storage moisture protection
Engineered cold-rolled structural systems manufactured to ISO 9001:2015 and CE standards. Choose from our specialized configurations for automated pallet transport, selective handling, and heavy-duty industrial picking.
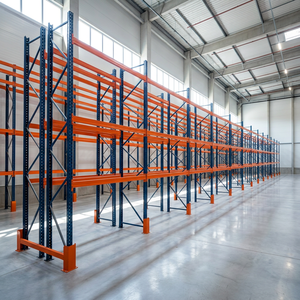
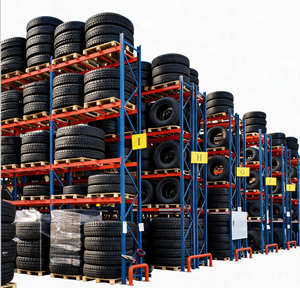
In modern supply chain engineering, warehouse real estate costs and temperature-controlled storage overhead dictate maximum cubic volume utilization. Traditional static selective pallet racking requires dedicated access aisles for every double rack run, resulting in a floor area space efficiency of merely 35% to 45%. The remainder is consumed by dormant circulation corridors.
Movable pallet racking systems (commonly referred to in automated intralogistics as Motorized Mobile Racking or MOVO) revolutionize this spatial geometry. By mounting heavy-duty racking superstructures onto electronically synchronized, rail-guided mobile bases, static access aisles are eliminated. A single variable operational aisle is opened only where and when pallet retrieval is demanded—either through Radio Frequency Identification (RFID), forklift truck remote terminals, or automated warehouse control system (WCS) triggers. This mechanism elevates floor surface space utilization up to 85% to 90% while doubling storage capacity within identical warehouse footprints.
The following analytical index evaluates the world's leading motorized mobile racking manufacturers and structural rack suppliers based on metallurgical compliance (EN 15512, RMI MH16.1), drive system design, in-floor guide rail tolerances, and integration capabilities for cold chains.
| Manufacturer / Brand | HQ / Primary Standard | Base Drive Technology | Payload Rating (Tons/Bay) | Cold-Chain Integration | Distinct Engineering Advantage |
|---|---|---|---|---|---|
| HEDA Shelves Direct Factory | China (CE / ISO 9001 / EN 15512) | Multi-motor synchronized shaft drive | Up to 36 Tons / Mobile Chassis | Fully Rated (-30°C to +40°C) | Complete OEM/ODM customization, rapid CAD FEA design, high container loading compaction |
| SSI SCHAEFER EU Standard | Germany (DIN EN / FEM) | Decentralized helical geared motor | Up to 32 Tons / Base Run | Specialized Cold Store Line | Proprietary WAMAS WCS automated integration, sophisticated laser proximity arrays |
| Dexion Storage Solutions Global Tier | Norway / UK (FEM / SEMA) | Direct flange-mounted gear motors | 24–30 Tons / Chassis | Standard -25°C package | Deep European field history, high-spec fail-safe safety interlocks and photoelectric curtains |
| Mecalux (Movirack) EU / US | Spain (EN / FEM / RMI) | Dual-wheel synchronized drive wheelsets | Up to 28 Tons / Base | Equipped with PLC heater kits | Turnkey integration with Easy WMS, robust mechanical rack collision bumpers |
| Stow Group EU Standard | Belgium (EN 15095 / FEM) | Variable frequency inverter drive | Up to 30 Tons / Unit | Anti-condensation drive housing | High precision profile roll-forming, competitive standard base modularity |
| Jungheinrich AG Intralogistics | Germany (EN 15095) | Electric drive networked to AGV | 24–32 Tons / Chassis | Low-temp drive lubricants | Native interface with Jungheinrich narrow-aisle electric forklifts and auto-dispatch |
| BITO-Lagertechnik EU Standard | Germany (DIN / FEM) | Modular drive bogie shafts | Up to 24 Tons / Bay | Pharma & cold room ready | Specialist for combined piece-picking and heavy pallet mobile carriage systems |
| Frazier Industrial US Standard | United States (RMI / ANSI MH16.1) | Heavy-duty electro-mechanical drive | Up to 40 Tons (Custom) | Structural channel design | Structural steel C-channel construction resisting high forklift impact damage |
| Interlake Mecalux Pan-American | USA / Mexico (RMI / AISC) | Floor-embedded rail electric system | 25–30 Tons / Base | Food processing cold storage | Extensive North American supply logistics, robust industrial steel upright columns |
| Redirack UK Specialist | United Kingdom (SEMA) | Motorized continuous wheel chain | Up to 24 Tons / System | Standard industrial | Recognizable sacrificial column base design, heavy welded beam connectors |
With a 30,000 m² automated production facility and 30,000 tons monthly throughput, HEDA Shelves engineers heavy-duty motorized mobile racking bases certified under CE (2435-CPR-8605159) and ISO 9001:2015. HEDA's proprietary bogie transmission and cold-rolled Q235B upright beams provide maximum payload integrity for industrial distribution, cold stores, and export logistics.
SSI Schaefer's motorized mobile racking delivers ultra-reliable automated controls, multi-level optoelectronic sensor barriers, and seamless linkage with automated guided vehicles (AGVs). Their heavy-duty carriage assemblies handle pallet positions exceeding 15 meters in height with micron-level rail alignment.
Pioneering mobile racking under the MOVO trade name, Dexion's systems utilize modular bogie architectures driven by continuous drive axles. They feature programmable variable speed profiles (soft start/stop) to guarantee zero pallet tip-over during high-acceleration transit.
Mecalux Movirack is designed to eliminate static aisles while offering standard PLC control enclosures on mobile headers. The system features dual emergency trip-wires, exterior light curtains, and integrated floor heating channel integration for harsh sub-zero freezing applications.
Stow's mobile racking systems feature automated roll-formed uprights and high-section-modulus beams. Their mobile base frames use CNC-machined wheelsets that glide across flush-mounted floor rails, eliminating trip hazards and minimizing wear on industrial forklift poly tires.
Jungheinrich merges high-density movable pallet racking with smart material flow equipment. Their systems synchronize with truck terminal communications, enabling the reach truck or VNA operator to open the destination storage aisle before arriving at the bay block.
BITO specializes in modular mobile pallet racking designed for high-density document archives, pharmaceutical warehouses, and parts logistics hubs. Their systems feature whisper-quiet mechanical transmissions and lower power requirements per mobile metric ton moved.
Renowned across North America for heavy structural steel channel manufacturing, Frazier equips mobile carriages with structural I-beams and channel uprights. These units provide supreme structural defense against harsh forklift impacts in high-velocity 3PL operations.
Delivering large-scale logistics installations across the United States, Mexico, and South America, Interlake Mecalux merges US seismic engineering standards with automated European mobile carriage drive engineering.
Distinguished by its sacrificial heavy welded base profiles, Redirack crafts robust motorized mobile units that optimize floor area in UK logistics hubs. Their drive systems incorporate redundant chain-and-shaft mechanisms that ensure smooth operations under continuous duty cycles.
Movable pallet racking is a precision electro-mechanical system where mechanical structural engineering directly intersects with industrial automation. Sizing, wheel load dissipation, and floor slab stabilization require rigorous analysis before fabrication.
Movable bases ride upon ground-embedded steel rails. High-load systems utilize a dual-rail design: flat guide rails to transfer purely vertical dynamic wheel loads, and grooved center rails to constrain horizontal lateral thrust forces. Floor flatness tolerances must comply strictly with DIN 18202 or Concrete Society TR34 (Class DM2 or superflat) to prevent motor stall and chassis skewing.
Rather than relying on a single central motor, modern movable bases feature decentralized electric geared motors distributed every 10–15 meters along the chassis run. Controlled by variable frequency drives (VFD), these units accelerate smoothly at 0.05 m/s² up to a cruising speed of 4.5 to 5.0 m/min, preventing load shifts on high upright pallet configurations.
Compliant with EN 15095 regulations, every movable racking bank incorporates: continuous photoelectric access light curtains across the main aisle entrance, chassis-mounted optical distance sensors, continuous emergency foot trip wires, and localized manual emergency stop mushroom buttons on every column header.
Purchasing movable pallet racking requires foresight into automated warehouse workflows. In the 2026–2030 horizon, four dominant macro-engineering trends are dictating global procurement specifications:
Traditional mobile racking relied on manual forklift operators pulling RF chords or pushing remote buttons. Next-generation systems interface directly with autonomous mobile robots (AMRs) and automated reach trucks via REST API and industrial OPC-UA protocols. The WMS orchestrates mobile aisle opening 30 seconds prior to AMR arrival, boosting pallet turnover speed by 42%.
In cold-storage warehouses (-25°C to -30°C), cooling an empty cubic meter wastes extensive energy. By eliminating aisles, movable racking slashes refrigerated building volume by 45% for identical pallet counts. This translates to an ongoing 35% to 50% power reduction on refrigeration compressors, drastically lowering ESG Scope 2 carbon footprints.
Upright columns and mobile wheel bogies are now outfitted with vibration and torque IoT sensors. Real-time telemetry detects early micro-misalignments, wheel bearing friction rises, or structural deflection from forklift bumps before mechanical binding or motor over-current tripping can shut down operations.
Since 2001, Guangzhou Heda Shelves Co., Ltd. has stood as a premier Chinese industrial racking manufacturer. Operating our own 30,000 m² factory in Guangzhou, we provide complete, integrated structural steel fabrication—from raw coil slitting, cold roll-forming, and automated CNC column punching to robotized welding and 10-stage electrostatic powder coating.
In-house manufacturing ensures total metallurgical control, certified Q235B cold-rolled steel, and 30,000 metric tons monthly output capacity.
Strictly compliant with CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Quality Management No. 18624Q00169R0M.
Specialized knockdown nesting and palletizing engineered to fit 20GP & 40HQ maritime containers, slashing landed ocean freight per pallet position.
Our senior engineering department delivers structural load calculations, AutoCAD layout plans, and full 3D BIM models within 24 to 48 hours free of charge.
Technical guidance compiled by our senior structural engineers to assist warehouse developers, operations directors, and logistics procurement teams.
Send us your warehouse CAD floor plan or pallet dimensions today. Guangzhou Heda Shelves Co., Ltd. provides customized structural layout engineering, structural load capacity calculations, and factory-direct pricing within 24 hours.