Featured Industrial Pallet Racking & Warehouse Systems
Engineered for high-bay consolidation, severe pallet loadings, seismic durability, and direct containerized export. Review our precision-formed structural steel configurations below.
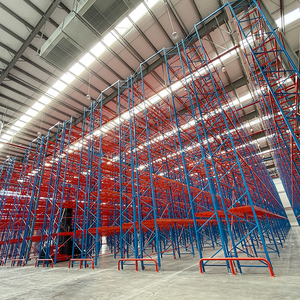
- FEM 10.2.02 & EN 15512 Certified
- 100% Direct SKU Selectivity
- Capacity: Up to 4,500 kg / Tier
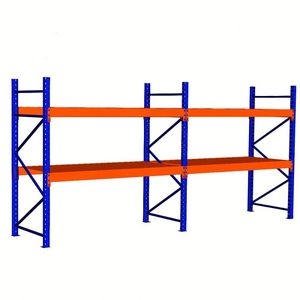
- Dual Pickling & Phosphating Finish
- 50mm / 75mm Adjustable Pitch
- High-Moisture & Coastal Defenses
- Sendzimir Galvanized Protection
- Cold Room & Freezer Engineered
- Modular Structural Interlock
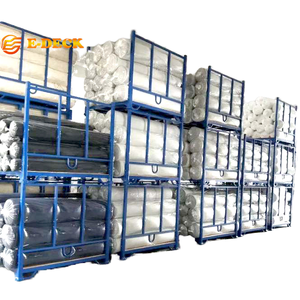
- Long-Roll & Fabric Storage Rails
- Reinforced Nested Base Plates
- High Space Volumetric Efficiency
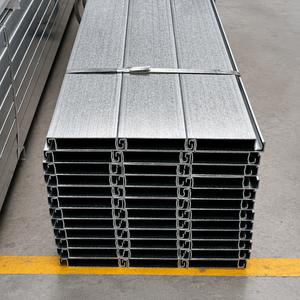
- Zero Concrete Pouring Required
- Heavy Axle Load Capacity
- Rapid Fast-Track Installation
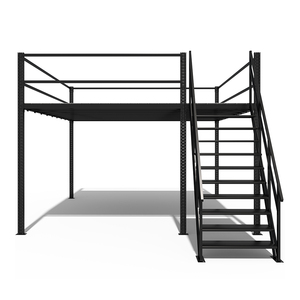
- Doubles / Triples Available Height
- 300 to 1,000 kg/m² Uniform Load
- Integrated Safety Gates & Stairs
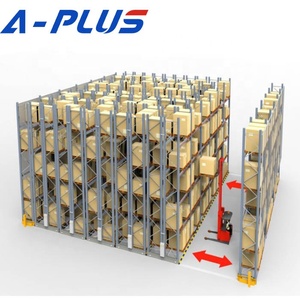
- PLC Touch-Screen Logic Control
- Consolidates 80% Aisle Space
- Optical Photoelectric Safety Stops
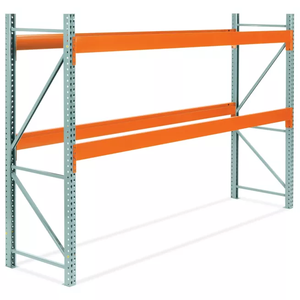
- ANSI MH16.1 RMI Standard Fit
- Universal Interlocking Tear-Drop
- 2-Inch Vertical Height Increments
Engineering Principles of Modern Heavy-Duty Pallet Shelving
Procuring pallet racking is not merely a purchase of formed metal; it is the commissioning of a primary load-bearing structural system inside your facility. A failure in structural calculation or material specification introduces severe human and financial risks.
Steel Metallurgy (Q235B vs Q355B vs ASTM A36)
Structural yield strength dictates deflection limits under load. While commercial shelving uses low-tensile coils, premier manufacturers roll heavy uprights from certified Q355B / S355JR or ASTM A1011 Grade 50 steel. This guarantees a guaranteed minimum yield strength of 355 MPa, preventing catastrophic column buckle under dynamic impact.
Deflection Tolerance & FEM 10.2.02 Standards
The international engineering standard requires a beam deflection ceiling of strictly L/200 (length divided by 200) under full design load. Under European EN 15512 rules, live load factors of 1.4 to 1.6 are applied to dead and dynamic weight, incorporating moment-rotation connection tests to certify upright-to-beam connection stiffness.
Seismic Engineering & Second-Order Effects
In seismic territories or high-bay installations exceeding 10 meters, racking designs must counter lateral drift and P-Delta effects. Custom baseplates with dual concrete mechanical or chemical resin anchors transmit torsional forces evenly down to the slab, preserving system alignment during ground motion.
Top 10 Pallet Shelving Racks Manufacturers & Manufacturing Leaders
An objective, technical evaluation of the world's premier pallet rack fabrication powerhouses. Each vendor is scored on fabrication precision, structural certifications, steel processing depth, and global logistics capability.
Founded in 2001, HEDA Shelves has emerged as an elite direct-to-enterprise structural racking fabricator. Operating out of a massive 30,000 m² state-of-the-art facility producing over 30,000 tons monthly, HEDA integrates custom roll forming, laser cutting, and dual-cure electrostatic powder coating under one roof. Holding CE certification No. 2435-CPR-8605159 and ISO 9001:2015, HEDA excels at providing bespoke structural layout engineering, free 3D CAD stress simulations, and knock-down container shipping optimization to over 120 nations.
- Core Specialization: Turnkey Selective, Radio Shuttle, Mezzanine, Drive-In & Cantilever
- Logistics Competency: Sea-freight cubic optimization for 20GP/40HQ containers
- Value Index: Industry-leading price-to-performance ratio; factory direct
A global benchmark in automated storage and retrieval systems (ASRS) and complex intralogistics. SSI Schaefer manufactures high-bay silo clad rack structures and automated shuttle frameworks designed to interface with proprietary software suites. Suited for Fortune 500 mega-fulfillment centers with extensive capex allocations.
- Core Specialization: Clad-rack buildings, automated miniload & pallet high-bays
- Key Advantage: Total turnkey intralogistics with in-house WMS/WCS software
Holding substantial fabrication assets across both Europe and the Americas, Interlake Mecalux produces an extensive range of standard roll-formed teardrop and bolted pallet racking systems. Their automated high-density pallet shuttle systems enjoy strong market penetration across 3PL logistics networks.
- Core Specialization: Conventional selective, drive-in, live pallet racking
- Key Advantage: Broad North American distributor network and RMI compliance
The inventor of the slotted angle concept in 1947, Dexion (now under Gonvarri Material Handling) remains a foundational pillar of European intralogistics. Their P90 selective pallet racking system is widely recognized for rigid engineering tolerances, modular adaptability, and strict EN 15512 compliance.
- Core Specialization: P90 multi-bay racking, mobile pallet racking (MOVO)
- Key Advantage: Proven longevity across automotive and aerospace assembly plants
Consistently ranked among the world's highest-revenue material handling system suppliers, Daifuku specializes in ultra-dense, crane-served rack structures engineered to sub-millimeter tolerances. Primarily recommended for mission-critical cold chain hubs, pharmaceutical manufacturing, and automated semiconductor storage.
- Core Specialization: Unit-load automated storage, crane-integrated structures
- Key Advantage: Flawless reliability in extreme-temperature environments (-30°C)
Renowned for both industrial forklift truck manufacturing and comprehensive storage systems engineering. Jungheinrich provides a unified approach where racking dimensions, narrow aisle profiles (VNA), and wire guidance systems match their material handling equipment with absolute precision.
- Core Specialization: Very Narrow Aisle (VNA), drive-in, dynamic push-back
- Key Advantage: Seamless integration between mast clearances and rack apertures
Operating dedicated fabrication hubs across Europe, Stow is a heavy-tonnage manufacturer of static pallet racks and robotic sub-systems through their 'Movu Robotics' division. Their Stow Atlas pallet shuttle is a widely deployed deep-lane pallet consolidation tool.
- Core Specialization: Stow Atlas 2D shuttles, heavy-duty cantilever racks
- Key Advantage: Extensive European production capacities and standardized profiles
One of the largest producers of warehouse pallet racks in North America, manufacturing over 100 million pounds of structural and roll-formed steel products annually. Famous for rigid hook-and-slot beam connections, structural channel columns, and high-impact seismic bases.
- Core Specialization: Structural steel pallet rack, push-back cart systems
- Key Advantage: Superior forklift impact resistance in high-throughput docks
Metalsistem specializes in prime cold-profiled galvanized structural steel racking systems, represented prominently by their Superbuild and Unirack lines. Using closed tubular profiles with grooved upright ribs, their products offer exceptional torsional rigidity while remaining rustproof without paint.
- Core Specialization: Sendzimir continuous-process galvanized racks, multi-tier platforms
- Key Advantage: Complete corrosion resistance for external yards and chillers
Recognized as the primary pioneer of 100% hot-rolled structural steel channel racking in North America. Unlike standard light-gauge sheet steel formed into uprights, Frazier utilizes structural C-channels that resist corner tearing and puncture from heavy counterbalanced forklifts in demanding heavy industrial facilities.
- Core Specialization: Heavy-duty hot-rolled structural C-channel storage systems
- Key Advantage: Unmatched structural impact absorption and low lifecycle repair incidence
| Manufacturer | Primary Steel Grade | Connection Architecture | Standard Certifications | Max Bay Load Rating | Best Fit Application |
|---|---|---|---|---|---|
| HEDA Shelves | Q235B / Q355B Cold Rolled | Euro Teardrop / 50-75mm Boltless | CE, ISO 9001:2015, RoHS | Up to 25,000 kg | Direct Import, 3PL, FMCG, Cold Chains |
| SSI Schaefer | High Tensile European Coil | Proprietary Integrated Wedge | EN 15512, DIN EN ISO 9001 | Up to 30,000 kg | Fully Automated High-Bay ASRS |
| Interlake Mecalux | ASTM A1011 / Structural | Standard Teardrop / Bolted | RMI MH16.1, ISO 9001 | Up to 22,000 kg | Mid-to-Large Retail Distribution |
| Dexion | S355MC Micro-Alloyed | P90 Hook-In Claw | EN 15512, FEM 10.2.02 | Up to 24,000 kg | Automotive Parts & Pallet Handling |
| Daifuku | JIS G3101 SS400 / SPHC | Robotic Flange Interlock | JIS, ISO 14001, CE | Custom Engineered | Ultra-Dense Automated Crane Silos |
| Metalsistem | 3.1 Certified High-Yield Galv | Reversible Ribbed Clip | TUV Rheinland, EN 15512 | Up to 20,000 kg | Corrosive, Refrigerated & Outdoor Yards |
| Frazier Industrial | Hot-Rolled ASTM A36 Channel | Heavy Bolted Structural Joint | RMI, AISC Structural Spec | Up to 35,000 kg | Severe Forklift Impact & Heavy Beverage |
Engineering Infrastructure of Guangzhou Heda Shelves Co., Ltd.
Why leading distributors, general contractors, and warehouse operators across Europe, the Americas, the Middle East, and Africa source directly from our industrial fabrication campus in Guangzhou.
Fully Integrated Factory
With 30,000 square meters of operational workshop floor space, every phase of production—including CNC precision slitting, multi-roller profiling, robotic welding, and powder polymerization—is retained in-house without sub-contractor variability.
Container Freight Math
International logistics costs can break a project budget. HEDA's logistics engineers utilize bespoke knock-down packing algorithms to stack upright frames and nest box beams, achieving over 95% cubic capacity inside 40ft High Cube containers.
Verified Certifications
All structural profiles carry accredited credentials: CE Certification No. 2435-CPR-8605159 for load structural compliance, ISO 9001:2015 Quality Management No. 18624Q00169R0M (valid through 2027), and verified RoHS finishes.
Complimentary 3D CAD
Our engineering department delivers full CAD floor layouts, clear-height aisle cross-sections, pallet placement matrices, and finite element load calculations within 24 to 48 hours of initial warehouse structural drawing submission.
The 10-Stage Precision Production Flow
How raw cold-rolled steel coils are transformed into certified, defect-free warehouse pallet racking:
Prime Coil Inspection
Spectrometric tensile & thickness verification of certified Q235B/Q355B coils.
Precision Slitting
Automated longitudinal shearing to sub-millimeter beam & post width tolerances.
Continuous Punching
High-speed CNC stamping for 50mm, 75mm, or teardrop pitch hole matrices.
Cold Roll Forming
Progressive 18-to-24 pass roll forming stations create multi-bend omega uprights.
Interlock Seam Welding
Robotic continuous CO2 shielded welding of interlocking twin-C box beam sections.
Connector Coupling
High-strength weldment of multi-claw connectors with integral safety lock pin ports.
Acid Pickling
Complete immersion tanks remove mill scale, surface rust, and rolling grease.
Phosphating Wash
Chemical conversion coating creates a crystalline microscopic bonding foundation.
Electrostatic Powder
Robotic automated spray guns coat thermoset epoxy polyester resin (60-80 microns).
Curing & Packing
200°C tunnel curing followed by steel-banded, foam-cushioned container bundle packaging.
Procurement Trends & Future Technological Evolution (2026–2030)
How intralogistics managers, 3PL executives, and global supply chain directors are modernizing pallet storage architectures to address labor shortages, land costs, and energy restrictions.
Trend 1: Rise of Radio Shuttle & Semi-Automation
Traditional drive-in racking is increasingly replaced by Radio Shuttle Racking Systems. Pallet shuttles run on internal rails powered by quick-charging lithium iron phosphate (LiFePO4) batteries. This setup reduces forklift transit cycle times by 50%, eliminates equipment collisions with upright posts, and maximizes volumetric storage in sub-zero refrigerated environments.
Trend 2: Micro-Alloyed High-Tensile Steel Profiles
Rising international ocean freight and metal commodities have accelerated the adoption of high-yield cold-formed steels (S355MC and Q355B). By executing advanced finite element optimization on post geometry, structural engineers reduce total steel weight per pallet location by 12% to 18% while simultaneously raising allowable load capacity.
Trend 3: Smart Sensing & Overload Monitoring
Smart warehousing demands structural transparency. Modern installations are integrating piezoelectric impact sensors and optical deflection monitors along critical lower rack tiers. If a forklift impacts a column or an unapproved double-pallet overload breaches the L/200 deflection ceiling, automated alerts notify maintenance supervisors via MQTT and warehouse management protocols.
Trend 4: Dark Warehouse & AMR Compatibility
Autonomous Mobile Robots (AMRs) and automated reach trucks require tighter floor-level aperture tolerances and non-reflective anti-glare floor channel coatings. Uprights must now incorporate barcode/QR alignment targets directly stamped into the metal during cold-rolling, enabling robotic LiDAR guidance without manual retrofitting.
Trend 5: Climate-Engineered Coastal Finishes
With maritime trade corridors growing rapidly across Africa, Southeast Asia, and Latin America, standard thin powder coating fails under coastal salt fog. Buyers now demand minimum 7-stage pre-treatment, hot-dip galvanizing, or specialized marine thermoset powders exceeding 1,000 hours in neutral salt spray testing (ASTM B117).
Trend 6: TCO-Driven Strategic Sourcing
Procurement teams evaluate total cost of ownership rather than initial invoice price. Over 15 years, a high-quality factory-direct racking system with verified steel certifications and modular expansion capability saves up to 40% in structural repairs, operational downtime, and facility re-layout expenses.
Industrial Pallet Shelving Racks: Technical Procurement FAQ
Direct answers to the most critical mechanical, structural, regulatory, and logistics queries encountered by facility managers during pallet rack procurement.
Plan Your Storage Project with Certified Structural Engineers
Whether optimizing an existing regional distribution hub, planning a cold chain freezer warehouse, or outfitting an international multi-tier mezzanine installation, our technical team provides free 3D CAD design, structural load calculations, and competitive factory-direct quotations.