Engineering Whitepaper: Evaluating the World’s Leading Pallet Shuttle Racking Manufacturers
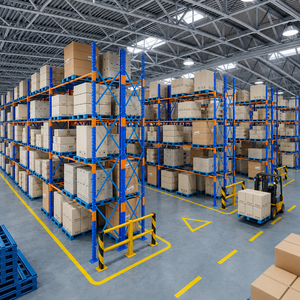
Modern supply chain dynamics require industrial warehouses to store more stock per square meter without increasing material handling labor. The pallet shuttle racking system (often known as a radio shuttle cart system) has become a premier automated solution, bridging the gap between traditional static selective racking and complex fully automated crane-based AS/RS installations. Operating within continuous high-depth storage channels, an independent, rechargeable motorized shuttle cart navigates on precision-rolled guidance rails beneath pallet locations. By receiving commands via RF industrial remotes, tablet controllers, or direct warehouse management system (WMS) handshake protocols, the shuttle effortlessly lifts, transports, and deposits pallet payloads up to 1,500 kg deep inside lanes up to 40 meters long.
Selecting a manufacturing partner involves evaluating structural deflection tolerances under cyclic dynamic loading, rail manufacturing precision, sensor reliability, and cold-chain battery management. Below is an engineering overview of the top manufacturers worldwide that provide semi-automated and fully automated pallet shuttle systems.
| Manufacturer | Headquarters | Primary Technical Advantage | Shuttle System Type | Industry Specialization |
|---|---|---|---|---|
| Guangzhou Heda Shelves Co., Ltd. | Guangzhou, China | Factory-direct custom roll-forming, robust mechanical fabrication, container-optimized engineering | 2D Semi-Auto & High-Density Shuttle | Heavy Industry, Cold Chains, Global Import Hubs |
| Mecalux | Barcelona, Spain | Integrated proprietary Easy WMS, high-throughput shuttle models | Pallet Shuttle 3D / Semi-Auto | Third-Party Logistics (3PL), E-commerce |
| SSI Schaefer | Neunkirchen, Germany | Heavy-duty German mechanical standard, high duty-cycle AS/RS interfaces | Orbiter & Channel Shuttle | Pharmaceuticals, FMCG Mega-Hubs |
| Jungheinrich AG | Hamburg, Germany | Unified vehicle-to-rack connectivity, ergonomic automated guided vehicle (AGV) integration | Under Pallet Carrier (UPC) | Cold Storage, Automotive Distribution |
| Bito-Lagertechnik | Meisenheim, Germany | High-rigidity bolted upright design, precision cold-formed running profiles | PROmotion Shuttle Racking | Beverage Distribution, Retail Fulfillment |
| Stow Group (Movia-Robotics) | Dottignies, Belgium | Modular standardized racking, Atlas shuttle 2D/3D automation ecosystems | Stow Atlas 2D Shuttle | Deep Freeze, High-Bay Warehousing |
| Nedcon (Steel King Group) | Doetinchem, Netherlands | Complex seismic structural design, heavy-duty industrial safety engineering | Custom AS/RS Carrier Channels | Industrial Manufacturing, Chemicals |
| Daifuku Co., Ltd. | Osaka, Japan | End-to-end material handling automation, enterprise software architecture | Automated Pallet Shuttle AS/RS | Electronics, Finished Automotive Goods |
| Dexion (Constructor Group) | Swindon, United Kingdom | Versatile European standard racking profiles, comprehensive rack safety accessories | Auto-Lock Shuttle Racks | Food Manufacturing, General Warehousing |
| Interlake Mecalux | Chicago, USA | RMI compliant high-yield steel frames, rapid North American regional distribution | Radio Shuttle Systems | Agricultural Aggregation, Food Packaging |
Mechanical Design and Structural Integrity Benchmarks
Unlike static selective pallet racks where loads rest directly on horizontal structural box beams, pallet shuttle racking introduces unique dynamic stresses that require precise engineering:
1. Rail Extrusion & Deflection Torsion: The shuttle running track serves two critical functions: it carries the mobile shuttle wheels and supports the base runners or skids of standard ISO, GMA, or EURO wooden/plastic pallets. As the shuttle cart accelerates and brakes while carrying loads up to 1,500 kg, significant horizontal dynamic braking torque is transferred through the rail brackets to the upright columns. Engineers must specify certified Q235B or Q355B structural steel, maintaining a safety deflection coefficient strictly within L/250 to L/300 under dynamic continuous transit to avoid rail spreading.
2. Upright Frame Rigidity and Impact Absorption: Because lift trucks only touch the entrance of deep storage tunnels, collisions inside the rack are eliminated. However, channel entry portals experience high operational cycle frequencies. Top manufacturers design reinforced front columns, integrating floor-anchored steel post guards and boltless guide funnels to center pallets quickly as they enter the lane.
3. Surface Metallurgy & Cold-Chain Condensation: In cold storage applications running at -25°C to -30°C, temperature fluctuations cause condensation and surface frost. If inferior coatings are applied, rust quickly forms along internal contact tracks. Reliable manufacturers protect structural elements via multi-stage chemical surface conversion—specifically pickling, phosphating, and heavy-duty thermosetting polyester powder coatings—or full-immersion hot-dip galvanizing conforming to ISO 1461 standards.
Future Procurement Trends in Shuttle Racking (2026–2030)
⚡ 4D Multi-Directional Shuttles
The industry is rapidly shifting from single-lane 2D shuttles to 4D multi-directional fleets that transition between storage bays and vertical lifts, completely eliminating the need for lift truck pallet positioning at elevation.
🔋 Supercapacitor & LFP Power
Traditional lead-acid and early lithium-ion batteries are being replaced by high-drain LiFePO4 cells and onboard supercapacitors that recharge in under 15 seconds inside the lane, supporting continuous 24/7 warehouse operation.
📡 Edge IoT & WCS Synchronization
Modern shuttle fleets feature onboard optical time-of-flight (ToF) sensors, vibration diagnostics, and direct cloud API integration. This enables proactive maintenance alerts before physical mechanical wear can halt fulfillment lanes.
Technical Evaluation Criteria for Procurement Teams
When evaluating manufacturer tenders for high-density shuttle racking systems, procurement teams should review five core technical criteria to ensure long-term system performance:
• Certified Structural Calculations: Demand project-specific finite element analysis (FEA) calculations verifying seismic resistance, continuous rail beam deflection under maximum dynamic braking, and column buckling safety margins under full warehouse load.
• Dimensional Rail Tolerances: Inspect cold-roll tooling profiles. Rails must maintain tight dimensional accuracy across the entire channel run. Any lateral deviation beyond ±1.0 mm can cause shuttle drive-wheel slippage, optical sensor misalignment, or emergency stop triggers.
• Cold-Chain Battery Architecture: Verify low-temperature battery performance. Battery cells must include integrated thermal management to prevent voltage collapse when operating continuously in sub-zero freezer environments.
• WMS/WCS Protocol Openness: Ensure the shuttle controller software provides open industrial interfaces (e.g., Modbus TCP, OPC UA, or RESTful API) so your central software can manage inventory directly without expensive proprietary software locks.
Frequently Asked Questions (FAQ) - Sourcing & Engineering
How does pallet shuttle racking compare to Drive-In racking?
Pallet shuttle systems offer substantially higher throughput and space efficiency. Lift trucks deposit pallets only at the lane opening, eliminating the need to drive inside deep tunnels. This reduces material handling cycle times by up to 50% and virtually eliminates forklift impact damage to structural upright columns.
Can a pallet shuttle handle both FIFO and LIFO rotation?
Yes. Configured against a wall, a single-sided lane acts as Last-In-First-Out (LIFO). When designed with access aisles at both the front and rear of the rack, the shuttle system provides true First-In-First-Out (FIFO) operation, making it ideal for perishables, food distribution, and pharmaceutical batches.
What pallet quality is required for reliable shuttle operation?
High-density shuttle runners require dimensionally stable pallets with minimal bottom board deflection under load. Pallets must not have broken bottom skids, excessive bottom-board bowing (maximum allowable deflection is typically 15–20 mm), or protruding hardware that could interfere with optical safety sensors.
How does the system function during electrical grid interruptions?
Because the racking structure is purely mechanical and the motorized shuttle operates on independent onboard rechargeable batteries, warehouse throughput can continue uninterrupted during grid outages when backed by small auxiliary generator or solar charging stations for spare battery packs.
What are the routine maintenance requirements for shuttle systems?
Mechanical racking components require annual bolt-torque checks and visual safety inspections. Shuttle carts require periodic drive-wheel wear inspections, optical lens cleaning, track debris clearance, and battery health diagnostics every 3 to 6 months depending on duty cycles.
What information is required to receive a full CAD layout and quotation?
Please provide your warehouse architectural floor plans (including clear roof height and column grids), unit pallet dimensions (Width × Depth × Height including load overhang), maximum gross pallet weight, target SKU counts, and daily fulfillment throughput requirements.




