Engineered Warehouse & Rolling Storage Product Portfolio
Explore our certified cold-rolled steel heavy-duty racking, mobile wire container units, and dynamic load-bearing systems built for high-throughput logistics hubs.
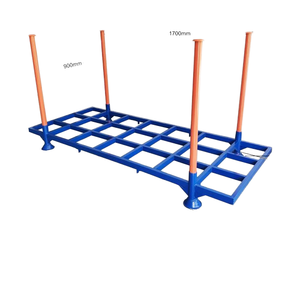
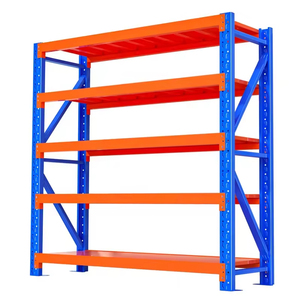
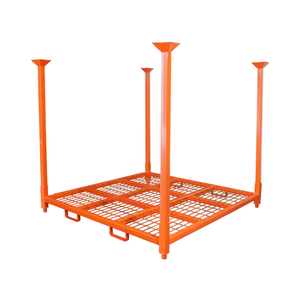
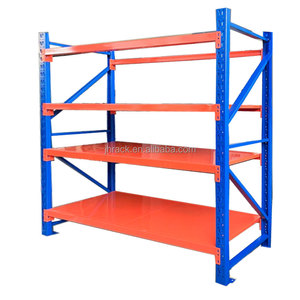
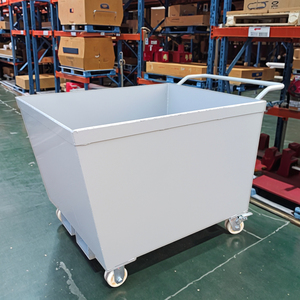
Executive Technical Overview: The Rise of Dynamic & Rolling Pallet Racks
A deep engineering and market analysis on mobile base pallet racking, dynamic gravity roller systems, and mechanical compact storage.
Modern supply chain infrastructures face severe pressures from soaring industrial real estate rates, escalating cold chain electricity consumption, and intense SKU diversification. In this landscape, rolling pallet racks—encompassing motorized mobile racking (MOVO), gravity roller flow racking, and deep-lane rolling cart systems—have transitioned from luxury niche installations into mainstream logistical imperatives. By eliminating static forklift aisles and converting wasted cubic volume into accessible storage density, rolling pallet systems can expand storage capacity by 85% to 100% across existing building envelopes without costly structural expansions.
Whether actuated by floor-embedded rail carriages or driven by gravitational force gradients, rolling pallet racking configurations require exceptional metallurgical integrity, precise rail alignment, and flawless mechanical tolerances. The failure of a single guide roller or carriage bogie under a 30-ton rack block can halt distribution operations completely. Consequently, global enterprise buyers must benchmark manufacturers not merely on nominal price per pallet location, but on structural engineering credentials, seismic design compliance (FEM 10.2.02, RMI, EN 15512), rail guidance metallurgy, and certified surface treatment durability.
Comparative Technical Analysis: Top 10 Rolling Pallet Racks Manufacturers & Suppliers
To assist logistics directors, supply chain VPs, and third-party logistics (3PL) engineering consultants in strategic vendor selection, our industrial analysis team has assessed the leading 10 manufacturers of rolling and dynamic pallet rack solutions worldwide based on manufacturing volume, technological innovation, structural longevity, and global customer support.
| Manufacturer / Brand | Headquarters | Primary Rolling Technology | Core Industrial Application | Compliance Standards | Global Supply Rating |
|---|---|---|---|---|---|
| Guangzhou Heda Shelves Co., Ltd. | Guangzhou, China | Motorized Mobile, Push-Back & Gravity Roller Systems | Cold Storage, 3PL Warehousing, FMCG, Mining | CE (2435-CPR-8605159), ISO 9001:2015, RoHS | Tier-1 Direct OEM |
| SSI SCHAEFER | Neunkirchen, Germany | Heavy-Duty Electric Mobile Racking (MOVO) | Automated Mega-Hubs, Deep Freeze Logistics | EN 15512, FEM 10.2.02, DIN EN ISO 9001 | Global Integrator |
| Mecalux, S.A. | Barcelona, Spain | Movirun Motorized Mobile Racking & Pallet Flow | Pharmaceuticals, Industrial Spares, Perishables | CE, ISO 9001, ISO 14001, RMI Standard | Global Major |
| Dexion (Constructor Group) | Castrup, Denmark | Electric Mobile Pallet Racking & Roller Beds | European Distribution Hubs, Heavy Manufacturing | FEM 10.2.07, EN 15620, ISO 9001 | European Specialist |
| Interlake Mecalux | Chicago, IL, USA | Deep-Lane Gravity Flow & Mobile Push-Back Carts | High-Throughput Grocery Wholesale, Beverage Bottlers | RMI (Rack Manufacturers Institute), ANSI MH16.1 | Americas Major |
| Stow Group | Dottignies, Belgium | Mobi-Stow Heavy Duty Mobile Bases & Shuttles | Heavy Raw Materials, Cold Storage, Agro-Chemicals | EN 15512, ISO 9001:2015, VDI 2690 | Global Fabricator |
| Bito-Lagertechnik Bittmann | Meisenheim, Germany | Dynamic Pallet Flow Lanes & Mobile Superstructures | E-commerce Buffer Stores, Automotive Sequenced Staging | RAL-RG 614, DIN EN 15512 | Specialized Tier-1 |
| Jungheinrich AG | Hamburg, Germany | Integrated Multi-Bay Mobile Pallet Racks | Intralogistics Turnkey Facilities, Bonded Ports | CE Marking, EN 15635, ISO 9001 | Turnkey System Provider |
| Frazier Industrial Company | Long Valley, NJ, USA | Structural Steel Glide-In & Mobile Pallet Bases | Heavy Impact Warehousing, Cold Rooms, Beverage | AISC, RMI Certified Structural Tubing | North America Leader |
| Daifuku Co., Ltd. | Osaka, Japan | Mobile Racking Systems & High-Bay Dynamic Units | Electronics, High-Density Clean Rooms, Auto Assemblies | JIS Standards, ISO 9001, ISO 14001 | Asia-Pacific Giant |
Detailed Supplier Profiles: Capabilities & Structural Distinctions
1. Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves): Operating from an expansive 30,000 square-meter precision manufacturing facility in Guangzhou, China, Heda Shelves has delivered more than 10,000 global warehouse projects across Africa, Southeast Asia, South America, and Europe since 2001. HEDA specializes in heavy-duty rolling and mobile racking systems tailored for harsh operating environments, seismic zones, and tropical coastal moisture conditions. With automated continuous roll-forming lines, automated punch presses, ultrasonic weld testing, and an integrated pickling-phosphating surface preparation line prior to electrostatic powder coating, HEDA provides complete OEM/ODM engineering from free 3D CAD design simulations to container-maximized ocean freight logistics.
2. SSI SCHAEFER: The German intralogistics powerhouse is globally celebrated for its motorized mobile racking system (MOVO). Designed for extreme space consolidation in cold storage (-30°C), MOVO features modular wheel assemblies, electronic synchronous motor drives, optical obstacle avoidance safety curtains, and seamless connectivity to Siemens PLC architectures.
3. Mecalux, S.A.: With operations spanning over 70 countries, Mecalux provides Movirun mobile racking systems that leverage multi-wheel flanged chassis driven by decentralized variable-frequency geared motors. Their designs excel in mid-to-large distribution facilities requiring dense pallet grouping with moderate selective access.
4. Dexion: Dexion holds extensive European market share with specialized mobile bases engineered to roll over heavy floor tracks embedded in fresh concrete or retrofitted onto existing warehouse slabs using low-profile leveling grouts. Their carriages feature robust remote radio control options.
5. Interlake Mecalux: The North American arm delivers premier gravity-based rolling pallet solutions, including push-back nested cart systems and heavy-duty roller-bed flow systems compliant with strict RMI and seismic standards across the western United States and Latin American corridors.
6. Stow Group: Known for its patented Mobi-Stow automated carriage, Stow provides high-rigidity structural uprights engineered for dynamic torsional loads induced during acceleration and deceleration of multiple connected rack rows weighing hundreds of metric tons.
7. Bito-Lagertechnik: Bito focuses on zero-energy gravity rolling lanes and compact mobile bases featuring speed controller rollers, magnetic retarders, and separation separators designed specifically for hazardous materials, cosmetics, and automotive sequenced buffers.
8. Jungheinrich AG: Integrating German-engineered reach trucks, AGVs, and mobile pallet racks, Jungheinrich delivers integrated smart warehouse ecosystems. Their mobile racks feature lighting synchronization that illuminates only the active working aisle to minimize energy overheads.
9. Frazier Industrial: Distinguishing itself through 100% hot-rolled structural steel construction (channel uprights and beams), Frazier's rolling and glide systems offer exceptional resistance to forklift impacts in heavy manufacturing, beverage keg distribution, and lumber yards.
10. Daifuku Co., Ltd.: Daifuku provides ultra-precise rolling and automated mobile rack installations, particularly for electronics assembly facilities and cold supply networks across Japan, South Korea, and the Pacific Rim, incorporating seismic base isolation mechanisms.
Architectural Breakdown: Mechanical vs. Motorized Rolling Pallet Racks
Selecting between motorized electric mobile racking and mechanical gravity rolling pallet racking depends on throughput dynamics, power availability, and capital allocation:
Electric Mobile Racks (MOVO)
Mounts standard selective pallet racks onto heavy motor-driven carriages moving along ground guide rails. Single access aisle opens upon electronic command. Maximizes cubic floor space by up to 90%, ideal for cold chain facilities where refrigerated volume costs are paramount.
Gravity Flow Rolling Racks
Utilizes inclined roller tracks (2.5° to 3.5° slope) with mechanical speed controllers and entry-exit separators. Operates purely on gravity via FIFO (First-In, First-Out) rotation. Requires zero electrical power, functioning uninterrupted during grid outages or power instability.
Mobile Push-Back Cart Systems
Features nested wheeled carriages running on inclined structural channels. Forklifts push front pallets back to expose lower carts (LIFO rotation). Delivers high density up to 6 pallets deep per lane while isolating wheel mechanisms from debris inside protected steel tracks.
Procurement & Technological Trends: 2025–2030+
Key evolutionary vectors shaping industrial tender specifications, engineering compliance, and operational automation worldwide.
AMR & AGV Interoperability
Rolling pallet carriages are increasingly designed with automated optical markers, RFID checkpoints, and zero-latency wireless mesh controllers to synchronize aisle opening with Autonomous Mobile Robots (AMRs) and automated reach trucks.
Grid-Independent Reliability
Emerging industrial hubs in Africa, Latin America, and Southeast Asia specify dual-power or fully mechanical fail-safe designs. Gravity roller flow racks and hybrid battery-buffered mobile carriages prevent production stoppages during municipal power shedding.
IoT Structural Health Sensors
Next-generation mobile carriages integrate real-time piezoelectric load cells, wireless tilt sensors, and bogie bearing vibration monitors that alert maintenance managers of floor subsidence, rail misalignments, or overload hazards before mechanical binding occurs.
Green Steel & Eco-Coatings
Global ESG mandates require documented Life Cycle Assessments (LCAs). Manufacturers adopt low-carbon scrap-electric-arc-furnace steel coils (Q235B/Q355B), solvent-free electrostatic powder coatings, and heavy pickling-phosphating treatments that eliminate toxic effluents.
Why Enterprise Buyers Partner with HEDA Shelves
A proven manufacturing foundation built upon rigorous structural calculations, certified European production standards, and transparent container shipping.
Verified Certifications & Traceability
Guangzhou Heda Shelves Co., Ltd. maintains active CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Management Systems (No. 18624Q00169R0M) valid through June 2027, and full RoHS compliance. Every production batch is certified with raw material chemical and tensile mill test sheets.
Complimentary 3D CAD & Load Modeling
Before any steel is cut, our structural engineering department produces full AutoCAD layouts, 3D photorealistic spatial renderings, and finite element stress models. We evaluate forklift turning radiuses, building column clearances, and floor slab load distributions free of charge within 24 hours.
Container-Optimized Ocean Logistics
Exporting to over 120 nations—including key transport corridors such as Lagos, Tema, Mombasa, Dar es Salaam, Durban, Alexandria, and Rotterdam—we utilize custom nesting packaging jigs that maximize volumetric loading inside 20GP and 40HQ shipping containers, saving up to 28% in ocean freight costs.
Frequently Asked Questions: Rolling Pallet Racks Specification
Comprehensive technical and commercial answers addressing structural engineering, floor tolerances, moisture protection, and installation logistics.