High-Density Storage & Dynamic Live Racking Portfolio
Explore our certified heavy-duty gravity flow racking, teardrop industrial systems, multi-tier mezzanines, and high-bay warehouse configurations manufactured directly under CE and ISO 9001:2015 standards.
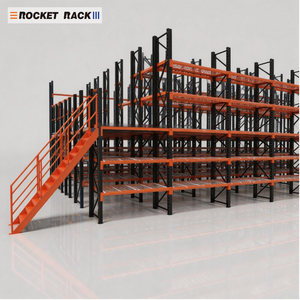
2 Layers Certified High Density Steel Mezzanine Rack 500kg/sqm Load
- Load Capacity: 500 kg/sqm
- Anti-Corrosion Powder Coating
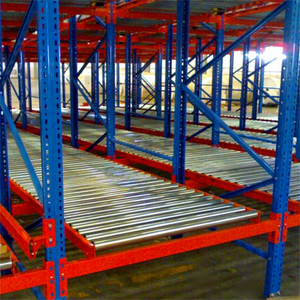
Heavy Duty Live Rack Pallet Flow Racking Cargo Gravity Roller Equipment
- Dynamic Gravity Brake Rollers
- Strict FIFO Stock Rotation
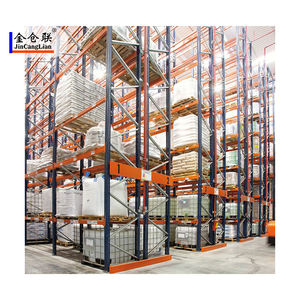
Longspan High Bay Industrial Pallet Rack Wire Mesh Deck Cold Rolled Q235
- Capacity: 1,500 - 4,500 kg
- Universal Teardrop Uprights
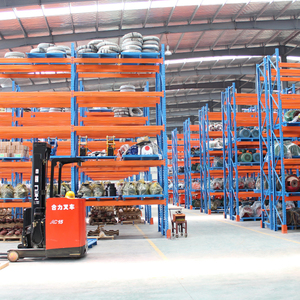
Best Selling Customized Warehouse Drive in Rack Steel Pallet Racking
- High Density LIFO Channel
- Reinforced Guide Rails
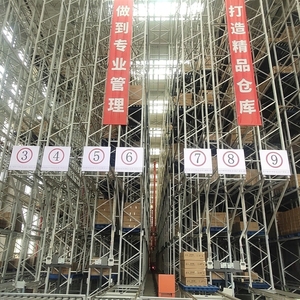
Wholesale Metal Frame High-bay Pallet Modular Flow Racking System
- Modular Expansion Tracks
- Cold-Rolled Structural Uprights
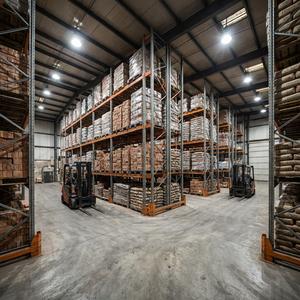
Heavy Duty Adjustable Pallet Rack Warehouse Storage Shelving System
- 50mm / 75mm Pitch Adjustable
- 100% Direct Selective Access
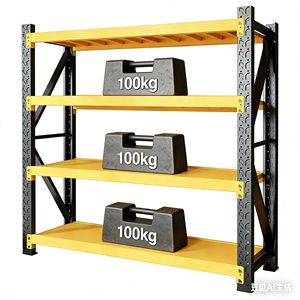
Steel Heavy Duty Foldable Adjustable 4-Layer Boltless Shelving Units
- Rapid Boltless Assembly
- Light Industrial & Garage Storage
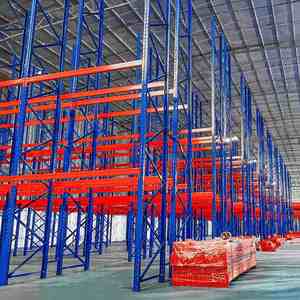
OEM ODM Heavy Duty Pallet Racking System Adjustable Beam High Load
- Custom Beam Sections & Gauge
- Direct Factory Export Stacking
Engineering Principles of Case Flow Gravity Racking Systems
A comprehensive examination of track gradient optimization, roller compound friction coefficients, split-case ergonomics, and zero-energy dynamic fulfillment.
Gravity Track Gradients & Pitch Precision
Case flow racks utilize inclined roller tracks (typically set between 2.5° to 5.0° (3% to 8% grade)) to advance cartons smoothly from the rear charging aisle to the front picking face. The precise pitch angle is calibrated according to tote weight, cardboard deformation index, and ambient temperature to prevent velocity runaway while ensuring zero stalls.
Polypropylene vs. Steel Roller Bed Engineering
Choosing between high-density polypropylene (PP) plastic wheels and galvanized steel skate wheels determines acoustic impact and dynamic longevity. PP wheels with stainless steel axles minimize ambient operational noise below 62 dB(A), while cold-rolled steel roller tracks provide extreme shear resistance for metal totes and heavyweight industrial components.
Ergonomic Knuckle Pick Shelves & Presentation Trays
To maximize human order picking accuracy, front picking beams are configured with downward-angled knuckle pick trays (15° to 30° tilt). This provides direct sightlines into carton contents, eliminating repetitive strain injuries (RSI) and cutting split-case order picking cycle times by up to 35% compared with flat static shelf layouts.
Comparative Performance: Dynamic Storage Architectures
Understand the quantitative operational trade-offs between static industrial shelving, gravity carton flow, pallet live racking, and automated pick systems.
| Storage Metric / Architecture | Case Flow Racking (Carton Flow) | Standard Static Shelving | Heavy Pallet Flow Racking | Vertical Carousels / AS/RS |
|---|---|---|---|---|
| Stock Rotation Principle | Strict 100% FIFO | LIFO / Random (Prone to Expiry) | Strict 100% FIFO | System Dependent FIFO/LIFO |
| Pick Face SKU Density | High (Up to 40 SKUs per Bay) | Low (Aisles required both sides) | Medium (1-2 Pallet SKUs per Bay) | Ultra High (Single Point Pick) |
| Picker Travel Reduction | 65% – 80% Reduction | Baseline Reference (0% Travel Cut) | 40% – 50% Reduction | 90% Reduction (Goods-to-Person) |
| Energy Consumption | Zero kWh (Pure Gravity Power) | Zero kWh | Zero kWh | High Electrical Consumption |
| Throughput (Picks/Hour) | 250 – 400 Picks / Man-Hour | 60 – 110 Picks / Man-Hour | 40 – 70 Pallet Moves / Hour | 350 – 550 Lines / Hour |
| Initial Capital Cost (Capex) | Moderate (Rapid 9–14 mo ROI) | Low Initial Capex | Moderate to High | Extremely High Capex |
Future Procurement & Technological Trends in Case Flow Racks
Market intelligence and technological foresight for procurement managers designing future-proof distribution centres over the coming decade.
1. Hybrid AMR & Carton Flow Synergy
The leading procurement trend across Tier-1 3PLs is pairing carton flow discharge zones with Autonomous Mobile Robots (AMRs). Rather than picker carts travelling hundreds of meters per shift, Case Flow units serve as the high-density stationary buffering nexus where human pickers remain stationary, placing sorted products straight onto autonomous bot transfer points.
2. Plug-and-Play Pick-to-Light (PTL) Integration
Modern factories now design flow bed profiles with pre-molded mounting channels for digital wireless Pick-to-Light and Put-to-Light modules. This visual confirmation eliminates paper pick lists, pushing pick error rates below 0.01% and enabling immediate onboarding of seasonal warehouse labor without lengthy software orientation.
3. Cold-Chain & Humidity Proof Formulations
With global pharmaceutical and frozen food cold-chain expansion, procurement specifications increasingly mandate anti-freeze polymer formulations for rollers that resist embrittlement down to -35°C. Concurrently, track assemblies utilize zinc-plated or high-phosphated powder finishes to eliminate oxidation caused by condensation during rapid freeze-thaw loading cycles.
Engineered for Precision, Delivered Worldwide
Founded in 2001, Guangzhou HEDA Shelves Co., Ltd. has grown into one of Asia’s preeminent heavy-duty storage manufacturing enterprises. Spanning a state-of-the-art 30,000 square meter production complex in Guangzhou, China, our manufacturing facilities process more than 30,000 tons of structural steel per month.
Unlike trading intermediaries, HEDA controls 100% of the cold-rolling, precision punching, profile bending, robotic welding, and pickling-phosphating electrostatic coating process under a single roof. This guarantees that your case flow and pallet live storage racks arrive on-site with zero dimensional tolerance errors, pristine corrosion protection, and comprehensive structural load validation.
Exporting directly to over 120 nations across the Americas, Europe, Southeast Asia, the Middle East, and Africa (Nigeria, Kenya, South Africa, Ghana, Egypt, and beyond).
4-Stage Precision Manufacturing & Testing Protocol
How HEDA guarantees structural integrity from certified Q235B raw steel coils to the final containerized ocean shipment.
Raw Steel Testing
Mill-certified cold-rolled Q235B and Q355B coils undergo ultrasonic thickness inspection and yield-strength tensile testing before entering automated slitting lines.
Continuous Roll-Forming
Dedicated multi-station roll-forming lines shape upright posts and side frame channels with continuous pitch hole punching tolerances held strictly within ±0.1mm.
Anti-Corrosion Pretreatment
Components pass through an automated 7-stage immersion: degreasing, ultrasonic water rinsing, acid pickling, phosphating, and 200°C baked polyester powder coating.
Dynamic Gravity Validation
Assembled case flow beds are pre-tested with maximum dead weight and dynamic slope rolling trials to verify zero track deformation and flawless roller spin velocity.
Frequently Asked Questions on Case Flow Racking
Detailed technical answers to common queries raised by supply chain executives, facility project managers, and logistics design engineers.
Modernize Your Order Picking & Storage Density Today
Connect directly with Guangzhou HEDA Shelves' lead intralogistics engineers. We analyze your throughput volumes, SKU velocity profiles, and warehouse CAD floor layout to formulate a customized, high-density case flow racking blueprint with turnkey factory pricing.