Founding Year
Factory Footprint
Monthly Steel Output
Global Projects
Export Nations
Skilled Engineers
Engineered Warehouse Storage Racks & Systems
Manufactured in full compliance with FEM 10.2.02 and ANSI MH16.1 structural steel standards. High-density cold-rolled profiles engineered for extreme seismic stability, dynamic warehouse throughput, and maximum vertical volumetric efficiency.
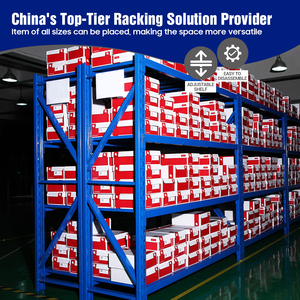
Light-Duty Commercial Stockroom Shelving System
Versatile boltless steel shelving engineered for parts stockrooms, automotive retail, archives, and multi-tier fulfillment hand-pick bays.
- Shelf Capacity: 100 - 300 kg/tier
- Assembly Mode: Boltless Plug-In
- Surface Coating: AkzoNobel Powder
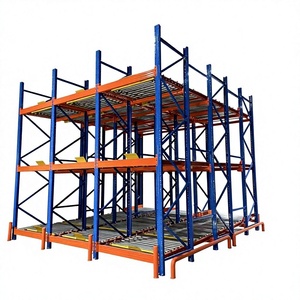
Gravity Pallet Flow Racking High-Density System
Automatic FIFO rotation powered by gravity flow roller beds with integrated centrifugal brake rollers and entry guides for zero-energy operations.
- Pallet Load: 500 - 1,500 kg/pallet
- Rotation Mode: Strict FIFO Gravity
- Roller Steel: Galvanized High-Torsion
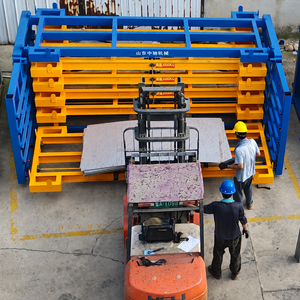
Heavy-Duty Sheet Metal Pull-Out Drawer Rack
Crank or mechanical slide-out drawer shelving designed for heavy industrial sheet metal, steel molds, dies, and plate fabrication stockrooms.
- Drawer Rating: 1,000 - 3,000 kg/level
- Extraction: 100% Full Extension
- Safety System: Mechanical Interlock
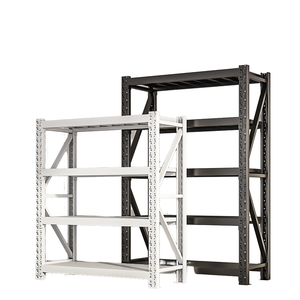
Multi-Layer Industrial Heavy-Duty Storage Rack
Custom structural steel pallet racking with reinforced box-beam profiles and step beams, accommodating standard wooden, plastic, or steel pallets.
- Bay Capacity: Up to 5,000 kg/level
- Steel Alloy: Q235B / Q355B Prime
- Pitch Adjust: 50mm / 75mm Perforated
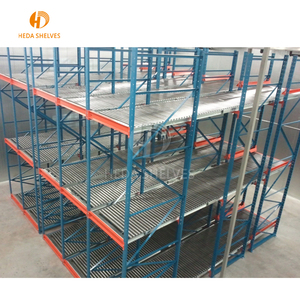
Dynamic Gravity Carton Flow Order Picking Rack
Engineered aluminum track roller lanes ideal for split-case picking, assembly line replenishment, and integrated pick-to-light fulfillment centers.
- Track Load: 50 - 150 kg/line
- Lane Divider: Full Adjustable Steel
- Efficiency Gain: Up to 40% Speedup
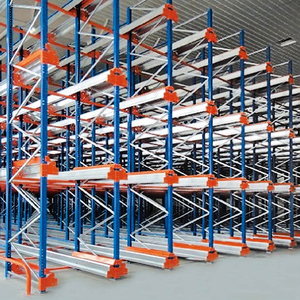
Cold Storage Radio Shuttle Deep-Lane System
Specialized anti-condensation sub-zero metallurgy designed for frozen cold chain logistics down to -30°C with automated semi-robotic shuttle carts.
- Temp Rating: -30°C to +40°C
- Battery Tech: LiFePO4 Internal Heater
- Finish Type: Hot-Dip Galv / Cryo-Epoxy
Industrial Heavy-Duty Radio Shuttle Pallet Rack
Maximizes clear building height by eliminating forklift operational aisles. Shuttles navigate pallets inside high-density channels via remote radio control.
- Lane Depth: Up to 50 Pallets Deep
- Drive Speed: 0.8 - 1.2 m/s Autonomous
- Space Gain: Up to 80% Footprint Use
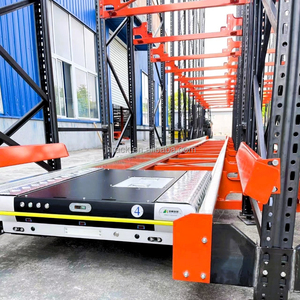
Automated Warehouse Shuttle ASRS Storage System
Intelligent turn-key shuttle warehousing integrates with warehouse management software (WMS/WCS) for automated pallet lifting, positioning, and retrieval.
- Automation: WMS / WCS Interfaced
- Positioning: Laser & Encoder Sensors
- Throughput: Continuous High-Cadence
Comprehensive Engineering Selection Matrix for Industrial Warehouses
When procuring warehouse infrastructure, senior logistics engineers must balance spatial volumetric efficiency against SKU selectivity, forklift compatibility, and structural deflection thresholds under full seismic load combinations.
Deflection Tolerance & Structural Metallics
Industrial pallet rack integrity relies strictly on cold-formed thin-walled steel standards (EN 15512 / ANSI MH16.1). Upright columns manufactured from prime Q235B and Q355B coils exhibit exceptional yield strength under concentrated axial loading.
- Beam vertical deflection strictly maintained below L/200 under maximal working load
- Cold-rolled omega profile uprights with multi-bend ribbing for torsional rigidity
- Automatic 5-hook connector brackets with dual safety locking pins preventing accidental dislodgement
Substandard manufacturers utilize uncertified scrap re-melt with uneven carbon distributions, triggering catastrophic column buckling during forklift contact.
Corrosion Kinetics & Pre-Treatment Technology
Warehouse longevity depends on surface preparation before electrostatic coating. Atmospheric moisture, aggressive chemicals, and coastal salinity induce severe micro-crevice oxidation inside bolt holes and welded joints.
- 9-stage chemical pre-treatment incorporating hot degreasing, pickling, and zinc phosphating
- Electrostatic polymer thermosetting powder coating applied at 60 to 90 microns thickness
- Rigorous salt-spray resistance verified up to 500 hours without surface blistering (ASTM B117)
Hot-dip galvanized finishes (zinc weight ≥ 450 g/m²) are deployed for sub-zero cold stores and tropical coastal hubs.
Global Shipping Density & TCO Optimization
Cross-border procurement economics hinge on freight container stowage efficiency. Unoptimized pallet frames create dead cubic space, driving up shipping freight costs per pallet storage position.
- Knock-down modular design nested with steel strapping for maximum 40ft HQ container loading
- Volumetric weight engineering yielding up to 26 metric tons net steel per 40HQ container
- Barcoded packaging and color-coded structural markings for error-free job-site sorting
Reduces ocean freight surcharge amortized over the installation lifecycle by 25% to 35% across global ports.
| Storage Topology | Space Utilization | SKU Selectivity | Stock Rotation | Aisle Width (Clearance) | Typical Applications |
|---|---|---|---|---|---|
| Selective Pallet Racking | 40% - 50% | 100% Direct | FIFO or LIFO | 3.0m - 3.8m (Standard FLT) | FMCG, 3PL Distribution, Multi-SKU Hubs |
| Drive-In / Drive-Through | 65% - 75% | 15% - 25% Batch | LIFO (Drive-In) / FIFO | Forklift Drives Inside Lanes | Beverage, Homogeneous Goods, Seasonal Bulks |
| Gravity Pallet Flow | 70% - 80% | 50% Per Lane | Strict FIFO (Gravity) | Separate Loading & Picking Aisles | Perishable Dairy, Pharmaceuticals, Food Batch |
| Push Back Racking | 60% - 70% | 30% - 40% | LIFO (Nested Carts) | Single Access Forklift Aisle | Medium Rotation SKUs, Cold Stores (2-6 Deep) |
| Radio Shuttle Automation | 80% - 90% | Lane-Level Access | Programmable FIFO / LIFO | Narrow Front Aisle (No Rack Entry) | Cold Storage Logistics, Heavy Meat, High-Volume E-com |
| Structural Steel Mezzanine | 100% Floor Gain | 100% Hand Pick | Manual Cart / Conveyor | Flexible Ergonomic Walkways | Apparel, Spare Parts, Packaging, Light Assemblies |
10-Stage Precision Heavy Industrial Manufacturing Process
At Guangzhou Heda Shelves Co., Ltd., certified engineering begins at raw coiled steel coil inspection and continues through robotic laser cutting, multi-station continuous roll-forming, automated CNC punching, and environmentally regulated surface passivation.










Why Global Supply Chains Trust Guangzhou Heda Shelves
Over 25 years of engineering manufacturing excellence. CE certified under CPR-8605159, ISO 9001:2015 quality assurance registered, and fully RoHS compliant.
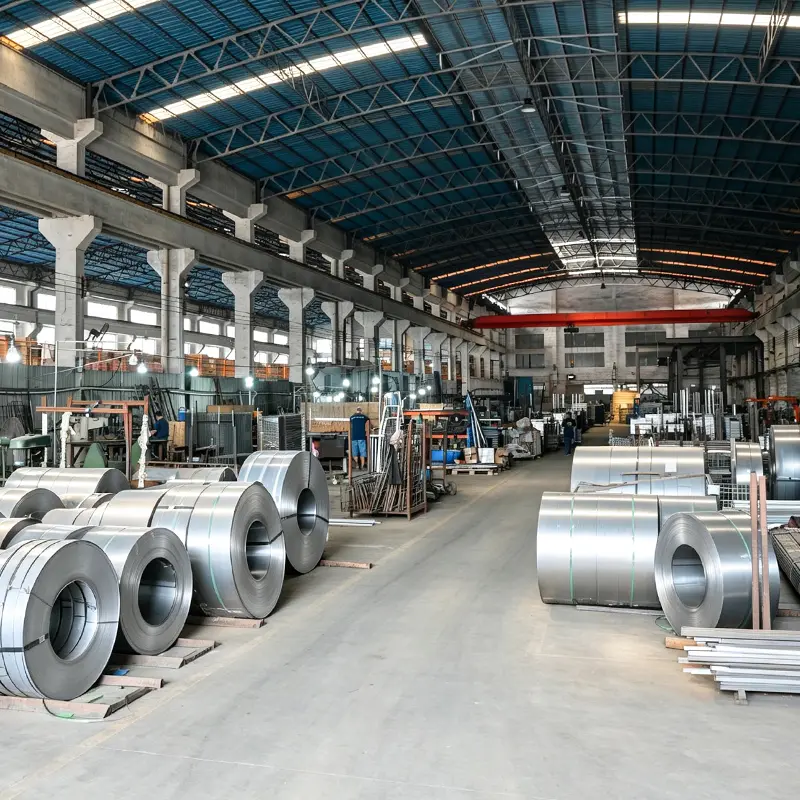
25+ Years Industrial Pedigree
Founded in 2001, providing structural racking design, roll-forming, and seismic engineering for complex 3PL facilities across 120+ destination countries.
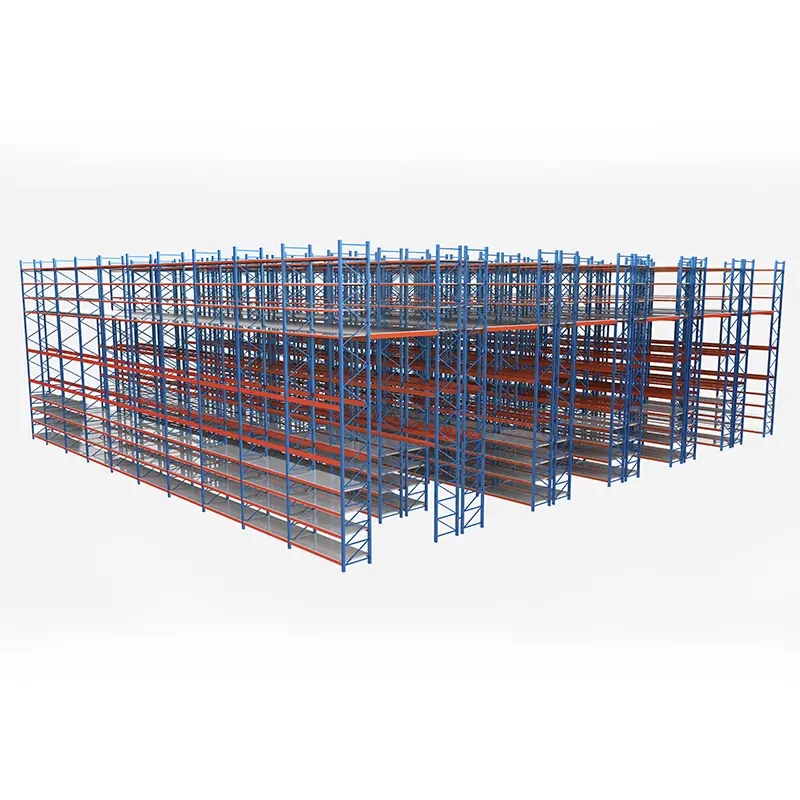
Free CAD & 3D Modeling
Our in-house structural engineers evaluate building column layouts, clear ceiling heights, and forklift turn radii to deliver complimentary CAD/3D blueprints within 24 hours.
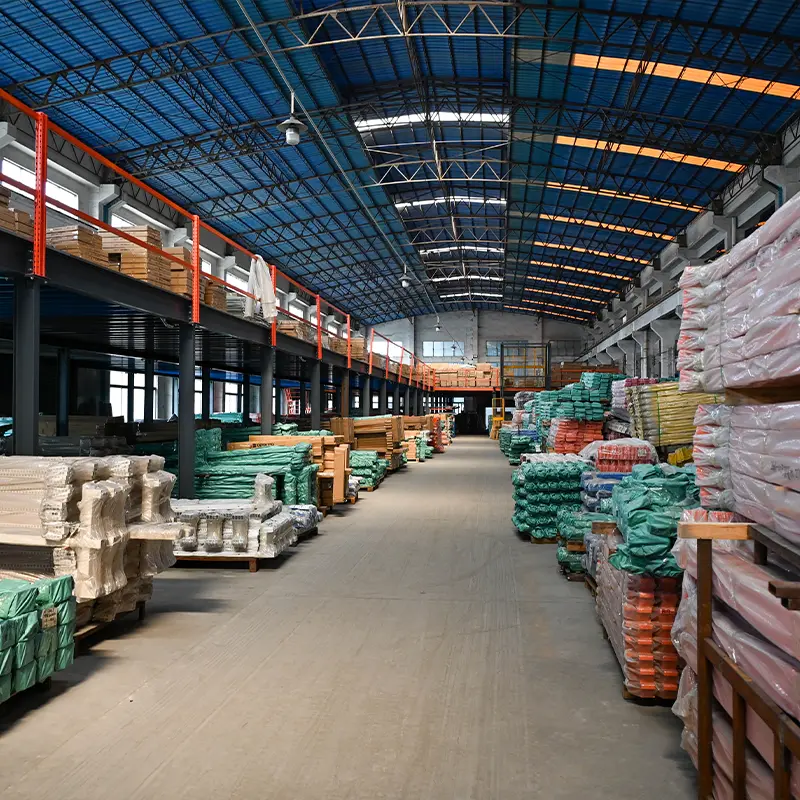
Verified Structural Quality
CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 registration No. 18624Q00169R0M guarantee uniform tensile strength, weld integrity, and safety compliance.
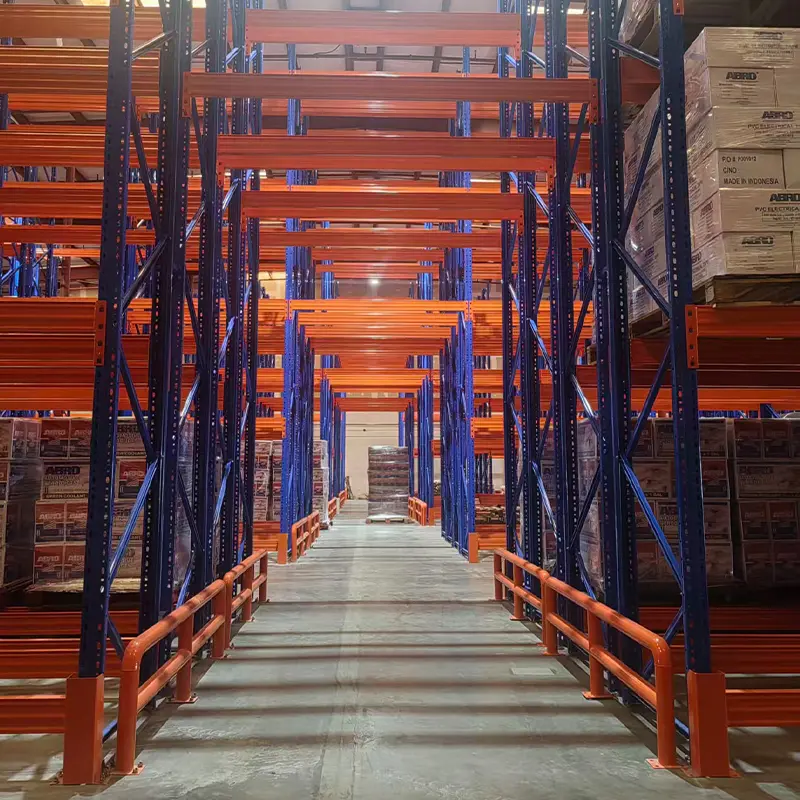
Turn-Key OEM / ODM Delivery
Bespoke upright hole pitches, specialized box-beam gauges, custom RAL brand powder coatings, and container-optimized knock-down packaging tailored to your project.
Future Procurement Trends in Warehouse Storage Infrastructure
Global supply chains are undergoing structural transformations driven by omni-channel fulfillment pressure, land price inflation, labor shortages, and stringent net-zero carbon mandates.
Automation-Ready Racking Topologies (AMR & ASRS)
Traditional static warehouses are transitioning to hybrid automation topologies. Racking structures must now be engineered with tighter dimensional tolerances (within ±1.5mm) to support Automated Guided Vehicles (AGVs), Autonomous Mobile Robots (AMRs), and stacker cranes.
- Laser-aligned rail systems integrated directly into cold-formed base plates
- Floor flatness specifications conforming to DIN 18202 and TR34 (FM1 / Superflat categories)
- Reinforced horizontal bracings absorbing cyclic dynamic braking forces from high-speed robotic shuttles
Low-Carbon Metallurgy & Circular Lifecycle
Corporate Environmental, Social, and Governance (ESG) mandates now scrutinize Scope 3 embedded carbon emissions in logistics capital expenditure. Steel racking foundries are adopting electric arc furnace (EAF) scrap steel coils and volatile organic compound (VOC) free finishing lines.
- Procurement demands documentation of carbon intensity per metric ton of fabricated steel
- Solvent-free electrostatic powder recovery systems reclaiming up to 98% of oversprayed powder
- Full modular demountability allowing 100% material recycling at end-of-life without landfill impact
Predictive Structural Health & IoT Telemetry
Forklift impacts and unrecorded overload events represent the primary risk factors for catastrophic warehouse rack collapses. Future procurement specifications incorporate embedded strain gauges, wireless deflection transponders, and RFID shock impact beacons.
- Immediate real-time alerts dispatched to warehouse management dashboards upon beam yield detection
- Digital twin integration mapping point loads against original FEA structural design models
- Mandatory preventive inspection regimes streamlined through computer-vision drone scanning
Tailored Racking Solutions for Demanding Industries
Different cargo profiles require purpose-engineered rack physics. Review how our technical layouts resolve operational bottlenecks in primary industrial sectors.
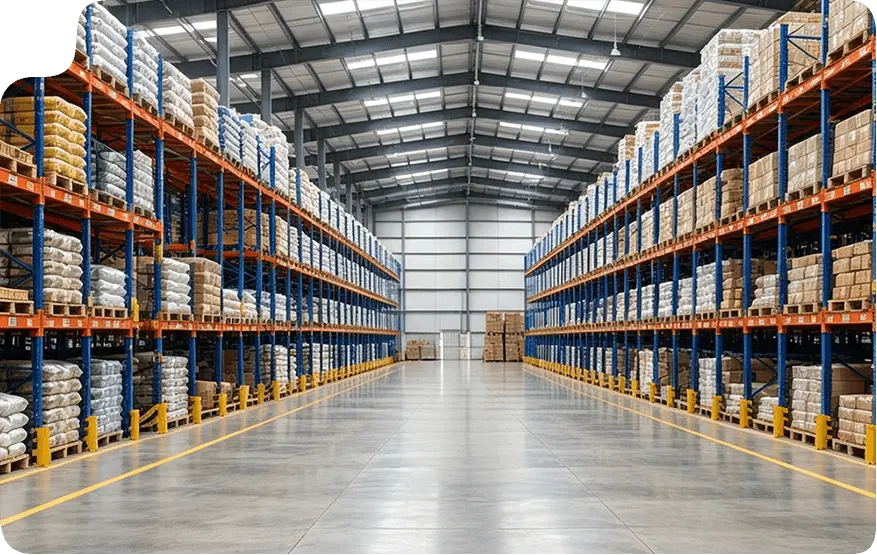
Agro-Processing & Bulk Grain
Floor-Bag Damage EliminationElevates bagged commodities (cocoa, coffee, grain, fertilizer) off floor slabs. Implements deep-lane Drive-In or heavy selective bays with ventilated wire decking to prevent moisture absorption and rodent contamination.
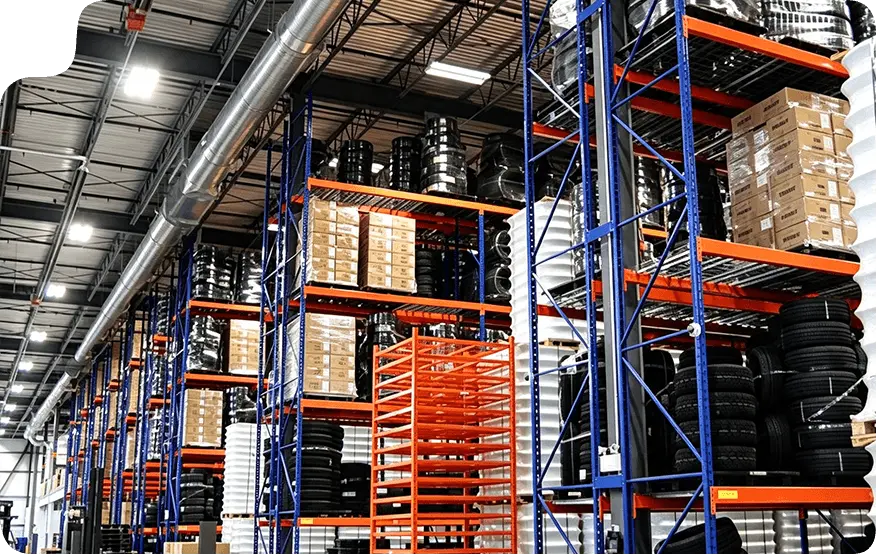
Automotive Spares & Distribution
High-Density Multi-Tier PickingCombines multi-tier rack-supported mezzanines with industrial longspan shelving. Organizes thousands of high-velocity automotive SKUs, body panels, and mechanical components with dedicated bin-box picking locations.
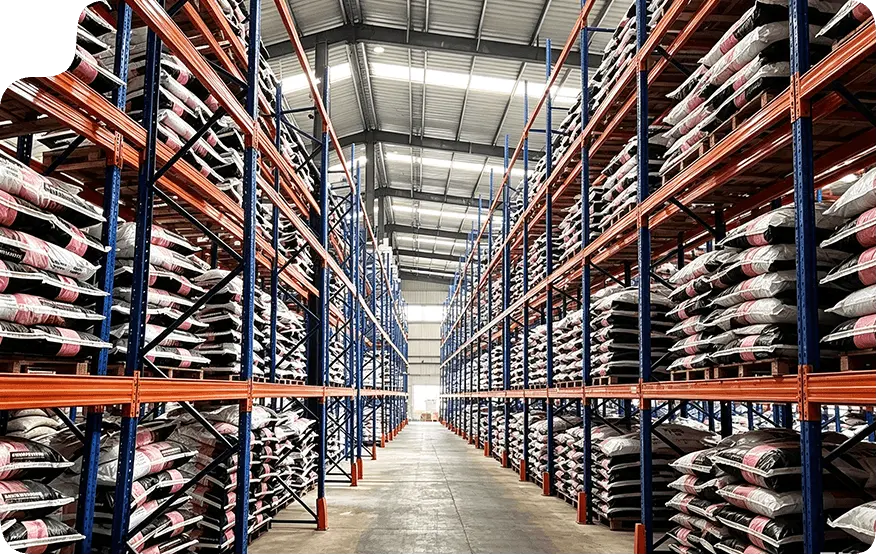
Building Supplies & Timber Yards
Long-Load Cantilever SystemsHeavy-duty structural cantilever arms and columns engineered for steel pipes, PVC conduits, timber bundles, rebar, and drywall sheets. Eliminates front column interference for continuous crane and forklift side-loading.
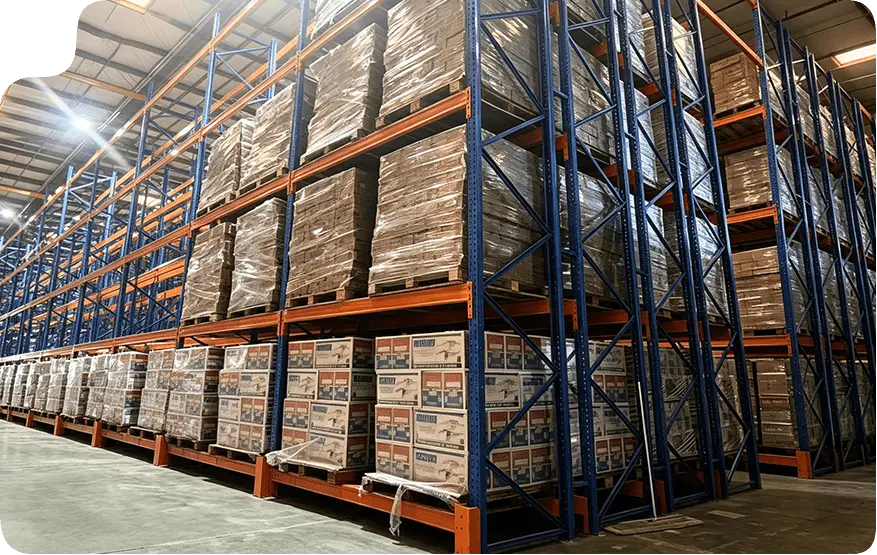
Food, Beverage & FMCG Wholesalers
Zero-Power FIFO RotationHigh-cadence Gravity Pallet Flow and Radio Shuttle racks preventing stock expiration losses. Protects fragile beverage packaging from crushing forces associated with floor-stacked block pallets.
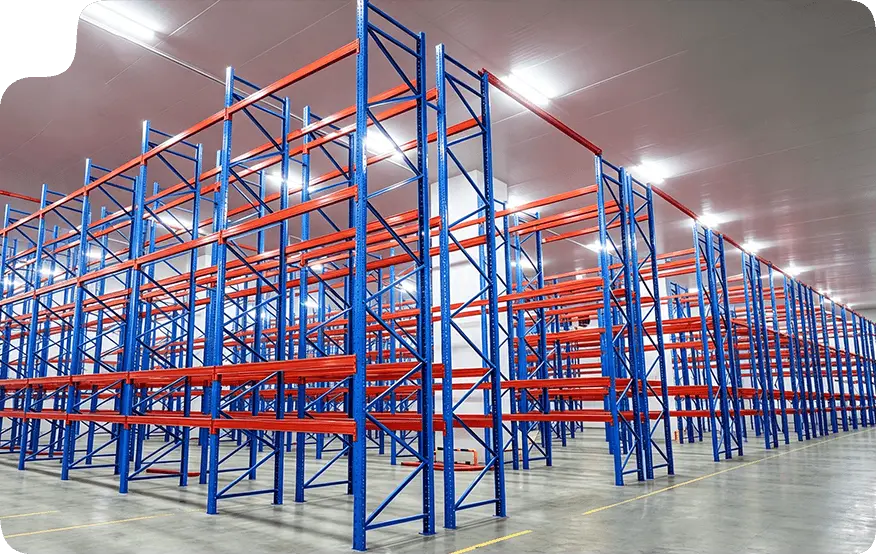
Cold Chain & Sub-Zero Stores
Volumetric Density to -30°CRefrigerated warehouse space incurs severe energy tariffs per cubic meter. High-density Radio Shuttle racks maximize bay density up to 88% cube utilization, lowering refrigeration power overhead per stored pallet.
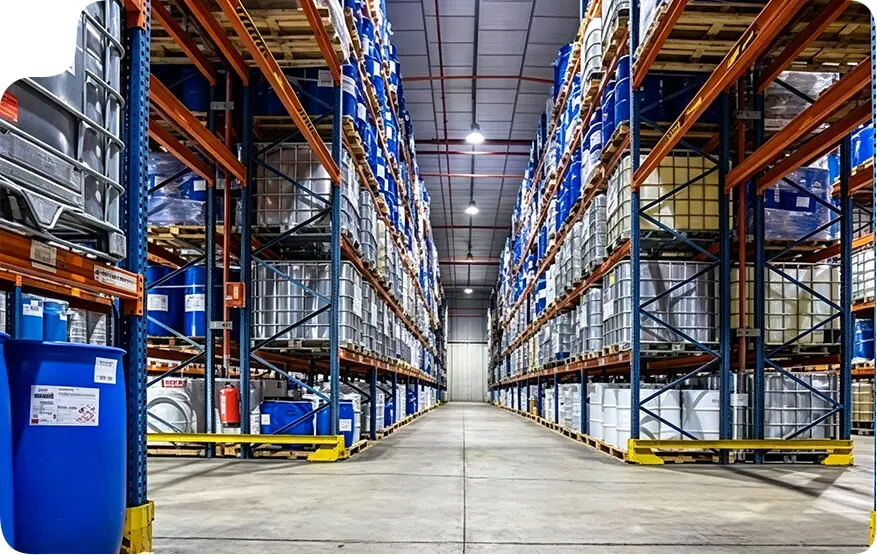
Chemicals, Lubricants & Mining
Spill Containment & Heavy DrumsReinforced pallet bays equipped with contoured barrel cradles, heavy-gauge galvanized wire decks, and column impact bull-guards for safe vertical storage of 200L oil drums and Intermediate Bulk Containers (IBCs).
Frequently Asked Questions by Industrial Warehouse Buyers
Comprehensive engineering insights covering structural safety factors, floor slab requirements, ocean containerization, and seismic load compliance.
What international structural engineering standards do your pallet racks comply with?
Guangzhou Heda Shelves Co., Ltd. designs and manufactures pallet racking in strict conformance with European Standard EN 15512:2020 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design), the British SEMA Code of Practice, and American ANSI MH16.1 / RMI specifications.
Our uprights and load beams undergo continuous finite element analysis (FEA) and physical destructive coupon testing to guarantee a minimum structural safety factor of 1.5 against ultimate yield strength under combined gravity and seismic load configurations.
What warehouse slab specifications are required before anchoring heavy-duty racking?
Standard heavy-duty selective and drive-in pallet racking installations require reinforced concrete industrial floor slabs with a minimum compressive strength of 25 to 30 MPa (C25/30) and a slab thickness of not less than 150mm to 200mm, reinforced with welded steel mesh or rebar.
Floor flatness should conform to standard DIN 18202 or Concrete Society TR34 (Class FM2 for standard reach truck operations; Class FM1 or Superflat for Very Narrow Aisle turret trucks). Each upright footplate is secured with heavy-duty M12 to M16 mechanical expansion anchor bolts or chemical capsule anchors torqued to specified engineering limits.
How do you protect pallet racks from premature corrosion in coastal or high-humidity regions?
We deploy a comprehensive multi-tier corrosion defense system. All cold-rolled steel components pass through a 9-stage automated chemical pre-treatment process comprising alkaline degreasing, acid pickling to eliminate mill scale, and zinc phosphating to create an insoluble crystalline conversion layer that stops micro-underfilm oxidation.
Components are then cured with thermosetting polyester electrostatic powder coatings (60 to 90 microns dry film thickness). For coastal ports with high airborne chloride levels or sub-zero refrigeration cold rooms with condensing moisture, we supply components hot-dip galvanized according to ISO 1461, yielding an ultra-durable zinc barrier exceeding 65 microns thickness.
Which high-density storage systems function reliably during electrical power outages?
If your warehouse operates in developing regions or suffers from unstable power grids, 100% mechanical storage systems are recommended. These include Selective Pallet Racking, Double Deep, Drive-In, Push Back, and Gravity Pallet Flow Racks. None of these configurations require electrical wiring or computerized PLC controllers to store and retrieve pallets.
For operations selecting semi-automated Radio Shuttle Racking, our shuttle carts utilize industrial-grade lithium-iron phosphate (LiFePO4) battery packs delivering 8 to 10 hours of continuous operation. Systems are supplied with auxiliary backup batteries and independent charging docks that can be powered via warehouse diesel generators or solar arrays.
How is ocean container loading optimized to minimize international freight costs?
Freight represents a significant component of cross-border racking procurement. HEDA Shelves utilizes automated 3D container packing software to engineer knock-down nested component bundles. Upright frames are either shipped disassembled with bolted diagonal/horizontal bracings or stacked flat to eliminate void spaces.
Beams, wire decking, and cantilever arms are bundled with high-tensile steel strapping, protective corrugated edge protectors, and specialized wooden skids for rapid forklift devanning at destination container freight stations (CFS). A single 40ft High Cube container typically holds between 22 and 26 metric tons of structural racking.
What engineering documentation is provided to support client warehouse planning?
Prior to contract finalization, our engineering department provides a comprehensive engineering submittal packet free of charge. This includes: (1) 2D AutoCAD floor plans detailing rack coordinates, column grid clearances, and egress aisles; (2) 3D isometric architectural renderings; (3) Structural load rating capacity plaques with calculated allowable load per level; (4) Container stowage plan; and (5) Step-by-step installation manuals with numbered component identification keys.
For customized project layouts or technical inquiries, click below to initiate immediate engineering consultation with our team:
Request Your Free 3D CAD Warehouse Layout & Structural Calculation
Direct communication with certified structural racking engineers, not generic sales brokers. Send your facility parameters for a free, comprehensive warehouse layout and landed freight calculation within 24 hours.
- Facility length, width & clear height
- Pallet size (W x D x H) & max weight
- Forklift make, mast height & turning radius
- Destination port & required delivery terms