Years Manufacturing Excellence (Since 2001)
Automated Heavy Industrial Factory Floor
Turnkey Racking Projects Across 120+ Countries
Monthly Structural Steel Processing Output
Industrial Storage Systems & High-Density Solutions
Precision-engineered pallet racking, gravity flow, multi-tier platforms, and high-density deep-lane storage components manufactured under strict ISO 9001:2015 and CE certification standards.
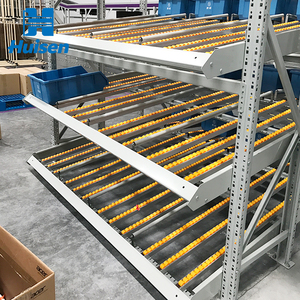
High Density Heavy Duty Steel Durable Corrosion Protection Flow Rack System for Warehouse Storage
- Dynamic Rotation: Strict FIFO Roller Track
- Steel Grade: Q235B High-Tensile
- Braking: Centrifugal Speed Rollers
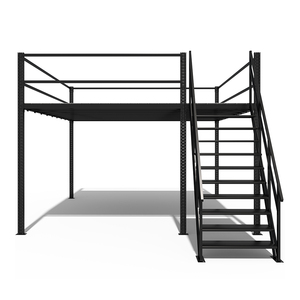
Heavy Duty Rack Industrial Mezzanine Interlocking Floor Rack Attic Racking System For Warehouse Storage
- Space Gain: +100% to +200% Usable Area
- Deck Load: 300–1000 kg/sqm
- Structure: Rack-Supported Interlock
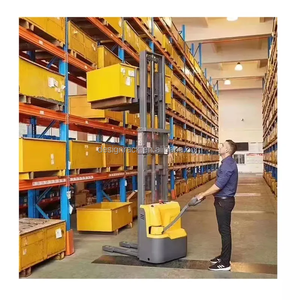
Adjustable Industrial Heavy Duty Racking System Warehouse Steel Metal Rack Storage Racks Shelving Units Boltless
- Level Adjustability: 50mm / 75mm Pitch
- Configuration: Selective Multi-Tier
- Safety Factor: FEM 10.2.02 Compliant
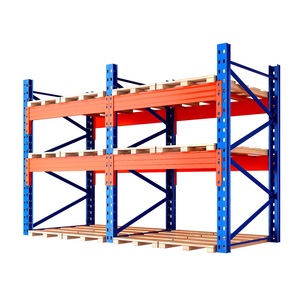
Heavy-Duty Beam-Type Steel Industrial Warehouse Drive-In Storage Racks Detachable Thickened Multi-Tier
- Storage Pattern: LIFO High Density
- Guide Rails: Thickened Continuous Rail
- Pallet Footprint: Up to 80% Aisle Reduction
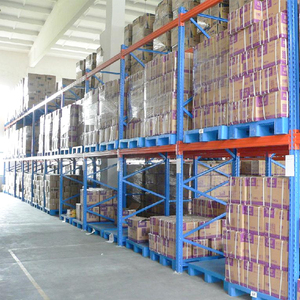
Heavy Duty Rack System For 3 Ton Warehouse Storage Adjustable Pallet Racking Shelf Unit Manufacturer Steel Rack
- Beam Load: 3,000 kg / Tier Uniform
- Upright Profile: Cold-Roll Sigma Channel
- Safety Lock: Spring Auto-Insert Safety Pin
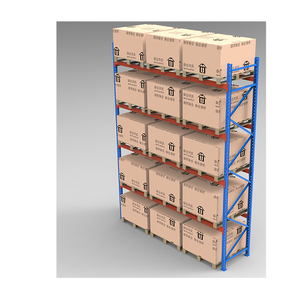
Heavy Duty Adjustable Metal Shelves Racking System Stacking Warehouse Storage Pallet Metal Racking
- Structural Grade: Solid Carbon Steel Plate
- Coating: Electrostatic Thermo-Powder
- Application: Distribution & Heavy Spares
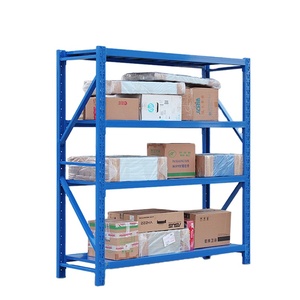
JIAMEI Storage Shelving Warehouse Storage Rack Long Span Shelf Rack
- Handling Mode: Manual Hand Picking
- Deck Type: Steel Panel / Wire Mesh
- Assembly: Hook-In No Bolt Fastener
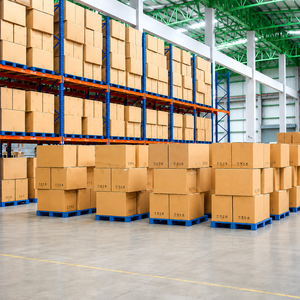
Steel Storage Rack 2000kg Heavy Duty Q235B Pallet Rack Warehouse Storage Rack High Density Industrial Shelving Solution
- Load Rating: 2,000 kg / Layer Rated
- Pretreatment: Acid Pickling & Phosphating
- Certifications: CE & ISO 9001:2015
High-Density Semi-Automated Pallet Shuttle Technology
A comprehensive examination of deep-lane semi-automated intralogistics: resolving the structural bottlenecks of floor stacking, drive-in rack deformation, and astronomical AS/RS capital expenditures.
The Mechanics of Radio Shuttle Automation
Modern distribution centers, food & beverage processing hubs, cold chain terminals, and pharmaceutical warehouses operate under extreme pressure to optimize cubic space while maintaining high cycle throughput. Traditional selective racking provides 100% pallet accessibility but consumes over 60% of warehouse floor footprint in access aisles. Conversely, drive-in racking eliminates aisles but forces forklifts to traverse deep inside structural steel tunnels, causing chronic upright collision, beam fatigue, and slow cycle times.
The Pallet Shuttle Racking System completely resolves this fundamental trade-off. An autonomous, low-profile radio-controlled carriage travels along specialized galvanized running rails embedded within deep storage lanes. Forklifts deposit pallets at the lane entryway, where the shuttle lifts the load using an integrated servo-mechanical or hydraulic platform and carries it smoothly along the channel to the deepest vacant position at speeds up to 1.1 m/s.
By decoupling the lift truck from the storage tunnel, structural racking impact is eliminated by over 92%, forklift operator cycle times drop by 40%–60%, and vertical storage can be safely engineered up to 24 meters high with lane depths exceeding 40 pallet positions.
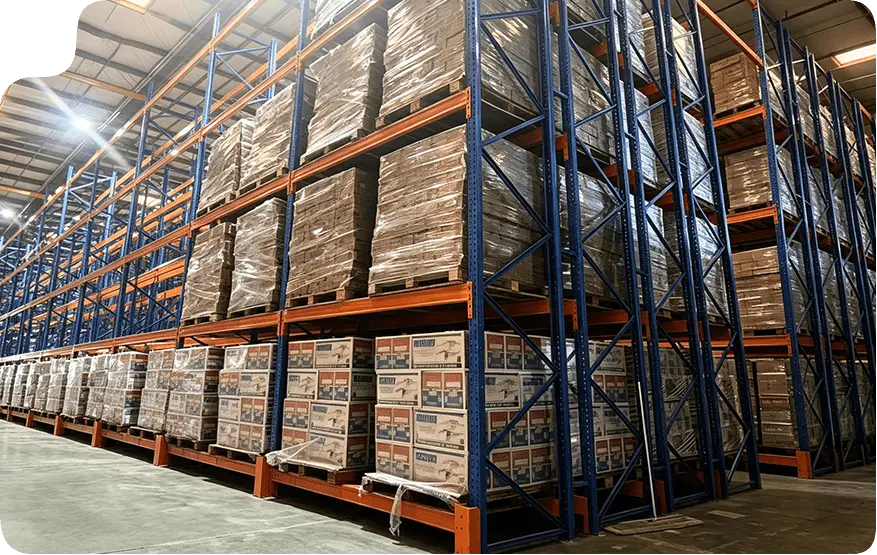
Dual Mode: FIFO & LIFO Execution
Configurable for both First-In-First-Out (essential for perishables, dairy, pharmaceutical cold chain, and batch lot tracking) and First-In-Last-Out (ideal for non-perishables, building materials, raw commodities, and FMCG manufacturing buffer stocks).
Cold Chain Thermodynamics (-30°C)
Equipped with low-temperature rated brushless AC drive motors, sealed IP65 electronic control boxes, condensation-resistant PCB coatings, and advanced lithium iron phosphate (LiFePO4) or lithium titanate (LTO) battery cells functioning reliably from -30°C to +45°C.
Multi-Sensor Laser Safety Arrays
Equipped with front and rear ultrasonic distance sensors, laser end-of-track buffers, pallet overhang photodetectors, rail drop-off mechanical stops, and emergency remote shutdown modules compliant with European CE machinery directives.
Guangzhou HEDA Shelves: Quality Controlled from Coil to Container
Why leading global logistics operators, procurement heads, and EPC warehouse contractors partner directly with Guangzhou Heda Shelves Co., Ltd. for mission-critical warehouse infrastructure.
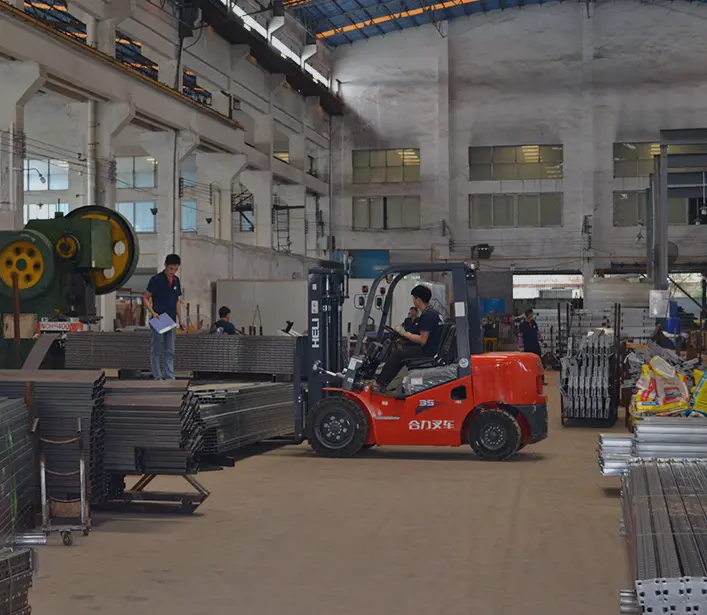
25 Years of Heavy-Gauge Steel Fabrication
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established itself as an authoritative global manufacturer and exporter of heavy-duty pallet racking, automated shuttle racking, industrial mezzanine systems, and high-density warehouse solutions. Our integrated 30,000 m² state-of-the-art production facility operates high-speed continuous cold-roll forming lines, multi-station automated column punching presses, and Japanese OTC robotic welding cells.
Unlike trading intermediaries, HEDA Shelves controls raw material sourcing directly from certified tier-one steel mills (Baosteel, Shougang Group). We engineer all primary load-bearing members using premium Q235B and high-yield Q355B structural steel, delivering certified tensile and yield performance calculated strictly under European FEM 10.2.02, British SEMA, and Australian AS 4084 standards.
The HEDA 10-Stage Precision Manufacturing Protocol
Every upright frame, box beam, shuttle track, and bracing truss undergoes systematic dimensional and metallurgical quality gates prior to export containerization.
Raw Steel QC
Mill certificate verification, ultrasonic thickness testing of Q235B/Q355B coil.
CNC Slitting
Precision coil unrolling and width shearing with ±0.1mm dimensional tolerance.
Auto Punching
High-speed hydraulic progressive punching for 50mm/75mm upright pitch.
Roll Forming
Continuous 24-station cold-roll forming to create rigid omega structural columns.
Beam Locking
Twin C-profile seam interlocking with 3-claw/4-claw drop-forged connector plates.
Robotic Weld
Gas-shielded automatic robotic welding eliminating manual seam imperfections.
Acid Pickling
Full chemical immersion removing rust, scale, and oil residues completely.
Phosphating
Zinc phosphate micro-crystalline barrier providing superior paint adhesion.
Powder Coat
Automated electrostatic epoxy-polyester coating baked at 200°C (60–90μm).
Export Pack
Dunnage protection, steel banding, and CAD-optimized container weight balancing.
Comparative Performance Analysis: High-Density Warehouse Systems
Evaluating capital investment, operational efficiency, floor space utilization, and risk factors across competitive warehouse storage configurations.
| Evaluation Parameter | Pallet Shuttle Racking | Drive-In Racking | Push-Back Racking | Gravity Flow Racking | Fully Automated AS/RS |
|---|---|---|---|---|---|
| Cubic Floor Space Utilization | 85% – 90% (Ultra High) | 70% – 80% (High) | 65% – 70% (Medium) | 75% – 85% (High) | 90% – 95% (Maximum) |
| Forklift Mast Damage Risk | Near Zero (Truck Outside) | High (Truck Enters Rack) | Low (Front Face Only) | Low (Separate Face) | Zero (Unmanned Cranes) |
| Pallet Cycle Throughput Speed | Very Fast (0.8–1.1 m/s) | Slow (Cautious Driving) | Moderate | Fast (Continuous Roll) | Maximum Automated |
| Maximum Lane Depth Allowed | Up to 40+ Pallets | Max 6–8 Pallets | Max 4–5 Pallets | Up to 20 Pallets | Unlimited System |
| Initial Capital Expenditure (CapEx) | Moderate / Highly Scalable | Low (Structural Only) | Medium (Rolling Carts) | Medium-High (Roller Beds) | Extremely High ($$$$) |
| Operational Flexibility (FIFO / LIFO) | Both FIFO & LIFO | Strictly LIFO Only | Strictly LIFO Only | Strictly FIFO Only | Software Controlled |
| Cold Storage Operating Efficiency | Optimal Cube & Power | Acceptable / Chilled | Cart Jamming Risk | Roller Freeze Risk | Excellent but Costly |
Need an objective structural comparison for your facility layout? Our CAD team provides free engineering calculations within 24 hours.
Get a QuoteProcurement Trends & Technological Evolution in Pallet Shuttles
Strategic analysis of global supply chain modernization, warehouse electrification, AI-driven fleet dispatching, and emerging 4-way omnidirectional shuttle developments.
1. Decoupled Modular Automation
Global warehouse operators are pivoting away from monolithic, proprietary automation that requires multi-million dollar initial lock-ins. Pallet shuttle systems allow logistics heads to purchase precision steel racking today and scale their shuttle cart fleet incrementally as throughput volume expands. If a shuttle unit requires preventive maintenance, it is simply swapped with a spare unit in 60 seconds without shutting down the entire warehouse aisle.
2. Transition from 2-Way to 4-Way Shuttles
While traditional 2-way shuttles travel down a single dedicated lane with forklift relocation between tiers, emerging high-throughput distribution centers are deploying 4-way multi-directional shuttles. Coupled with vertical lifters, 4-way shuttles traverse both longitudinal lanes and transverse cross-aisles independently, creating a high-density, fully autonomous 3D grid matrix managed via intelligent Warehouse Execution Systems (WES).
3. LFP Battery Tech & IoT Telemetry
Lead-acid and early nickel-cadmium batteries have been completely superseded by high-density Lithium Iron Phosphate (LiFePO4) and Lithium Titanate (LTO) energy storage modules. Modern shuttles now deliver 8 to 12 hours of continuous operation on a 2-hour rapid recharge cycle. Real-time IoT telematics broadcast wheel wear, motor temperature, acceleration torque curves, and battery cell health directly to maintenance tablets.
Energy Efficiency & Sustainable Logistics Impact
Refrigerated and frozen storage represents one of the most electricity-intensive subsectors of industrial logistics. When a cold room is configured with selective racking, up to 65% of the refrigerated cubic volume is wasted cooling empty forklift driving corridors. Converting to a high-density pallet shuttle system reduces the required cold room refrigeration envelope by 40% for the exact same pallet storage capacity, generating continuous electrical power savings across the 25-year structural lifecycle of the facility.
Containerization Engineering & International Job-Site Support
Safeguarding structural integrity across thousands of ocean miles from Guangzhou port to project hand-over in North America, Africa, the Middle East, Southeast Asia, and Europe.
Cube-Optimized Container Packing
Components are bundled using custom steel chocks, heavy-duty dunnage air bags, and anti-abrasion edge protectors to maximize 40HQ container cube utilization. Beams, uprights, and guide rails are nested precisely to prevent dynamic ocean transit rubbing or powder-coat marring.
Galvanized Tropical Climate Protection
For humid maritime terminals, tropical African coastal facilities (Lagos, Tema, Mombasa, Durban), and sub-zero blast freezers, guide tracks and baseplates undergo continuous pre-galvanization or hot-dip zinc bath treatment achieving zero rust formation even in 95% relative humidity.
Turnkey Field Engineering & Supervision
Every shipment contains complete 3D mechanical assembly manuals, numbered frame schematics, torque specifications for anchor bolts, and laser-guided track alignment blueprints. Our senior project engineers provide on-site supervision or real-time remote video guidance.
Demonstrated Global Provenance: Over 10,000 Deliveries
Chemical distribution in Ghana · Cold storage fruit packing in Kenya · Heavy automotive logistics in Thailand · FMCG wholesale in South Africa
Frequently Asked Questions: Pallet Shuttle Racking Sourcing
Technical, operational, and commercial insights compiled directly by our chief structural engineers to assist procurement committees and supply chain directors.
Q. What warehouse floor tolerances (flatness/levelness) are mandatory for pallet shuttle installations?
Pallet shuttle systems do not require ultra-strict superflat floor tolerances like Very Narrow Aisle (VNA) wire-guided turrets. However, the concrete floor slab must comply with standard industrial warehouse specifications such as DIN 18202 Table 3 Group 3 or ASTM E1155 (F_F 25 / F_L 20). Level deviations are fully compensated during installation via laser-leveled steel shims beneath our heavy-duty column baseplates before mechanical expansion anchoring.
Q. How many radio shuttle carts are required per total pallet capacity?
Unlike fixed crane AS/RS where each aisle requires a dedicated million-dollar stacker, the ratio of shuttle carts to pallet locations is determined solely by hourly peak throughput (pallets in/out per hour), not total static storage volume. A typical 5,000-pallet facility operating at moderate rotation might require only 4 to 6 shuttles. Shuttles are rapidly moved between different lanes and vertical beam tiers by standard counterbalance or reach trucks.
Q. Can the pallet shuttle racking system accommodate irregular, slave, or perimeter pallets?
Yes. Our shuttle carriages and proprietary galvanized guide tracks are engineered to support Euro pallets (800x1200mm), Standard Industrial pallets (1000x1200mm), Australian pallets (1165x1165mm), and custom chemical skids. Shuttles feature adjustable pallet overhang detection sensors. For damaged pallets or bottomless skids, our engineering team integrates secondary sub-lane support channels or rigid steel wire decking beds.
Q. What happens if a shuttle cart suffers a battery drain or sensor fault inside a deep lane?
All HEDA shuttle units are equipped with a redundant fail-safe recovery protocol. In the rare event of complete battery discharge inside a 30-pallet-deep tunnel, a secondary shuttle or motorized recovery carriage equipped with a remote mechanical docking hook is dispatched into the lane to automatically lock onto the disabled carriage and tow it back to the entry aisle for inspection.
Q. How does HEDA Shelves protect structural racking against aggressive maritime and chemical corrosion?
All structural components undergo an intensive multi-stage surface treatment: ultrasonic degreasing, continuous hydrochloric acid pickling, surface conditioning, and zinc-iron microcrystalline phosphating. They are then enveloped in an automated electrostatic booth with premium thermo-hardened epoxy-polyester powder (60–90 microns). For extreme seaside or sub-zero chemical environments, hot-dip galvanizing per ISO 1461 is available.
Q. What international certifications and structural test reports accompany your export shipments?
Guangzhou Heda Shelves Co., Ltd. holds verified CE Certification No. 2435-CPR-8605159 (Construction Products Regulation compliance for structural steel), ISO 9001:2015 Quality Management System Certification No. 18624Q00169R0M (valid through June 2027), and RoHS environmental clearance. All load-bearing beam calculations and deflection ratios (L/200 to L/300) adhere strictly to European FEM 10.2.02 and EN 15512 codes.
Q. What lead time is standard for a 2,000 to 10,000 pallet position turnkey system?
Standard manufacturing fabrication lead time for a complete 2,000–5,000 pallet position project is typically 20 to 30 calendar days from CAD drawing freeze and deposit verification. Shuttles undergo continuous 72-hour burn-in testing and optical sensor calibration prior to wooden crate sealing. Ocean transit times depend on the destination port (e.g., 20–28 days to Western Africa, 14–18 days to the Middle East, 18–25 days to Western Europe).
Q. Can an existing Drive-In racking installation be retrofitted into a Pallet Shuttle system?
Yes. If your existing drive-in upright columns, column spacing, and aisle configurations are structurally sound, HEDA Shelves can engineer retrofit adapter brackets and custom galvanized shuttle rails that mount directly to existing columns. This brownfield upgrade transforms slow, hazardous drive-in tunnels into automated shuttle lanes at approximately 50% of the cost of a complete greenfield installation.
Accelerate Your Warehouse Modernization Project
Share your architectural building dimensions, ceiling clear height, pallet weights, and throughput targets. Our senior racking structural engineers will return a complete 2D CAD floor plan, 3D volumetric rendering, and static load calculation within 24 hours.
- Free 2D CAD & 3D Layout Simulation
- Certified FEM 10.2.02 Load Calculations
- Factory-Direct Competitive Sourcing
- Complete Ocean Containerization Support
Request Technical Layout
Connect with a dedicated intralogistics project engineer immediately.
Get a Quote