Engineered Warehouse Storage Racks & Logistics Space Systems
Precision cold-rolled and automated structural storage architectures engineered for high-bay stability, severe loading criteria, seismic compliance, and high-frequency stock turnover.
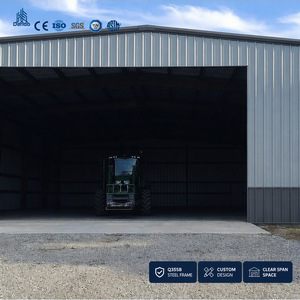
Large Span Warehouse Building Clear Height Storage Facility Pallet Racking System Logistics Space Optimization Design
- Max Span: 4,500 mm beam bay width
- Structural: Q235B / Q355B high-tensile steel
- Standard: EN 15512 & RMI certified
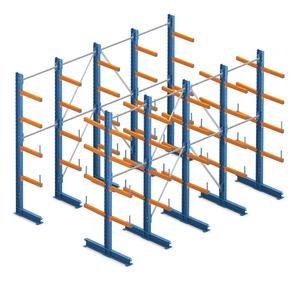
Cantilever Racking Warehouse Storage Rack Steel Assemble Racks
- Capacity: Up to 1,500 kg per cantilever arm
- Configuration: Single & double-sided column
- Application: Rebar, timber, pipes, profiles
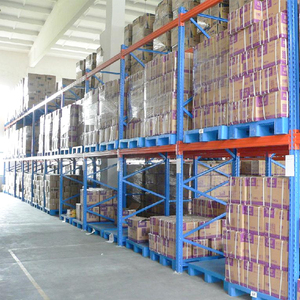
Heavy Duty Rack System For 3 Ton Warehouse Storage Adjustable Pallet Racking Shelf Unit Manufacturer Steel Rack
- Payload: 3,000 kg / beam level rating
- Pitch: 50mm / 75mm adjustable increments
- Safety Factor: 1.5 structural limit multiplier
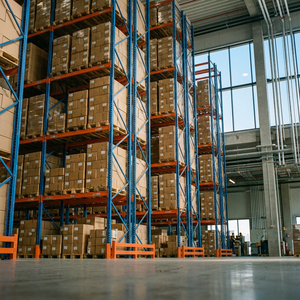
Customized Heavy Duty Pallet Racking System Warehouse Storage Rack Factory Direct
- Engineering: Custom column footprint & height
- Protection: Integrated frame column impact guards
- Finish: AkzoNobel powder coating layer
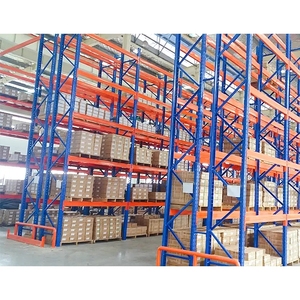
Steel Racking Solutions Heavy Duty Storage Shelves Pallet Racking System Warehouse Storage
- Selectivity: 100% direct instant pallet retrieval
- Compatibility: Counterbalance, reach trucks, VNA
- Decks: Steel plate, wire mesh, or timber options
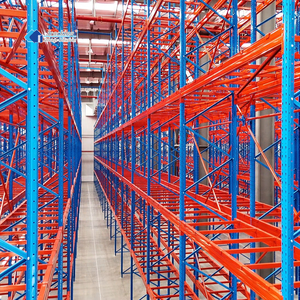
High Density Steel Storage Racks EU Standard Heavy Duty Adjustable Pallet Racking System for Warehouse Storage Solutions
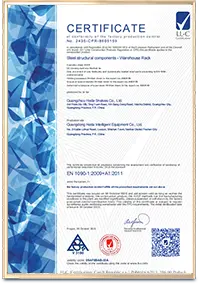
- Compliance: CE Certificate No. 2435-CPR-8605159
- Deflection Ratio: Maintained below L/250 limit
- Uprights: Heavy omega closed-roll geometry
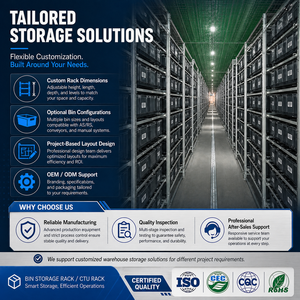
Mini Load ASRS Tote Storage Rack Automated Bin Warehouse Racking System for Small Parts
- Automation: Crane & robotic tote extractor interface
- Tolerances: ±1.5 mm dynamic assembly accuracy
- Speed: High-velocity picking cycle integration
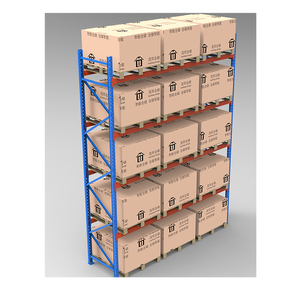
Steel Heavy Duty Racking High Density Pallet Racking Systems Warehouse Storage Racks for Sale
- Space Utilization: Up to 85% cubic efficiency
- Fulfillment: LIFO or FIFO deep-channel configuration
- Reinforcement: Continuous welded cantilever rails
Why Global Supply Chains Rely on HEDA Shelves
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates an integrated 30,000 m² advanced production facility. We bridge civil structural engineering standards and automated storage mechanics to supply certified warehouse racks worldwide.
Certified Metallurgy: Q235B / Q355B Steel
We source certified primary hot-rolled and cold-rolled steel coils exclusively from premier national mills. Every batch is validated via spectral chemical analysis and universal tensile testing machines, ensuring minimum yield strength exceeding 235–355 MPa and continuous elongation properties that eliminate micro-cracking during cold profile bending.
Pretreatment & Anti-Corrosion Longevity
To safeguard structural steel deployed in humid coastal logistics terminals, tropical mining compounds, and refrigerated cold stores (-30°C), all parts undergo automated multi-tank immersion pickling, surface degreasing, and micro-crystalline phosphating prior to 180°C–200°C electrostatic epoxy powder polymerization curing. Hot-dip galvanized finishes match ASTM A123 requirements.
Engineering Integrity: FEM & RMI Standard
Every racking layout is modeled using finite element method (FEM) analysis. We strictly enforce European standard EN 15512 (Steel static storage systems), EN 15620 (Tolerances, deformations and clearances), and American RMI MH16.1 specifications, assuring certified floor anchor shear resistance, dynamic sway resistance, and safe seismic dissipation factors.
10-Stage Production Lifecycle: From Steel Coil to Export Container
Precision component geometry dictates warehouse racking safety. Our in-house automated production chain guarantees strict ±0.5 mm tolerances across upright punching pitches, interlocking beam connectors, and frame bracings.










Emerging Trends Shaping Industrial Warehouse Racking (2025–2030)
Warehousing economics are transitioning rapidly from pure floor-area metrics to 3D volumetric optimization, automated material handling synergy, and climate-resilient infrastructural investments.
1. Semi-Automated Radio Shuttle Dominance
Traditional drive-in systems are facing higher operational costs due to forklift collision risks and slow lane travel. Procurement is shifting rapidly toward semi-automated radio shuttle racking. Independent 48V battery-powered shuttles maneuver pallets within deep bays up to 40 meters at 0.8–1.0 m/s speeds. This reduces forklift transit times by 65% while keeping operators outside rack lanes, preventing rack upright structural fatigue and product damage.
2. Power-Resilient Logistics Mechanics
In regions challenged by volatile national electrical grids, industrial planners are steering away from fully integrated automated cranes that risk complete blackout halts. Instead, top-tier EPCs specify hybrid mechanical configurations: high-density gravity roller flow racks (pure kinetic energy requiring 0 kW electricity) paired with battery-charged shuttle units sized to work off-grid alongside local solar-diesel battery backup stations.
3. High-Cube Mezzanine Architecture
With urban logistics real estate leasing rates climbing 8–14% year-over-year globally, logistics operators avoid building new physical warehouses by erecting self-supported multi-tier steel mezzanines inside existing 9–14 meter facilities. Multi-tier rack-supported platforms double or triple usable square footage, separating automated pallet buffers at ground level from manual e-commerce micro-fulfillment decks above.
Structural Racking Benchmark: Engineering & Operational Matrix
Comparative evaluation of primary industrial storage systems across footprint density, throughput cycles, beam deflection, and capital investment per pallet location.
| Storage System Category | Footprint Efficiency | SKU Selectivity | Max Unit Payload | Deflection Standard | Material Handling Type | Relative Capex |
|---|---|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% | 100% Instant | 1,000 – 4,500 kg / tier | FEM L/200 & L/250 | Standard Counterbalance / Reach | Baseline ($) |
| Drive-In / Drive-Through | 65% – 75% | Low (LIFO / FIFO) | 1,000 – 2,000 kg / pallet | EN 15512 Class A | Narrow Reach / Counterbalance | Medium ($$) |
| Radio Shuttle Automation | 80% – 88% | Moderate (Batch FIFO) | 500 – 2,500 kg / pallet | High-Tolerance ±1.5 mm | AGV, Shuttle & Standard Forklift | Moderate-High ($$$) |
| Heavy-Duty Cantilever | Continuous Span | 100% Side Access | 500 – 1,800 kg / arm | ISO 9001 Tested | Side-Loader / 4-Way Reach | Medium ($$) |
| Structural Steel Mezzanine | 150% – 250% (Volumetric) | Custom Deck Zoned | 300 – 1,500 kg / m² | AISC / Eurocode 3 | Forklift, Pallet Jack, Conveyors | Engineered ($$$) |
| Mini-Load ASRS System | 85% – 92% | 100% Automated | 50 – 300 kg / tote | Precision CNC Rails | Automated Stacker Cranes | Advanced ($$$$) |
Audited Quality Assurance for Turnkey Global Tenders
Guangzhou Heda Shelves Co., Ltd. provides comprehensive engineering documentation required by institutional tender boards, structural fire marshals, and corporate supply chain auditors worldwide:
- CE Certification (Factory Production Control): Certificate No. 2435-CPR-8605159
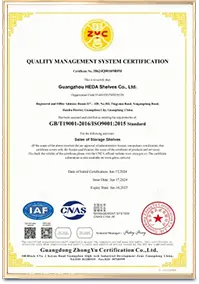
- ISO 9001:2015 Management System: Certificate No. 18624Q00169R0M (Valid through June 2027)
- RoHS Compliance & Chemical Safety: Tested nontoxic electrostatic powder coat surfaces
- Seismic Calculation Validation: Dynamic finite element structural stress reports
Frequently Asked Questions for Warehouse Racking Buyers
Clear, engineer-level explanations covering seismic engineering, deflection thresholds, anti-corrosive finishes, ocean container packaging, and slab load calculations.
How do you calculate warehouse concrete slab capacity and anchor bolt pull-out limits for heavy-duty racking? +
Structural racking safety relies on floor slab engineering as much as upright steel thickness. A 10-meter upright frame bearing 20 metric tons transfers focused point loads onto concrete slabs via steel baseplates. Under EN 1992 (Eurocode 2) and ACI 318 standards, floor slabs must exhibit minimum compressive strength of C25/30 or 3,000–4,000 PSI, with slab depth ranging from 150 mm to 250 mm. Our engineers calculate the exact footprint dimensions of the baseplate to distribute compressive stress below the slab's allowable bearing limit. For anchoring, we specify mechanical wedge anchors or chemical epoxy capsules (such as M12x110 or M16x140) tested to resist dynamic vertical pull-out forces and lateral seismic shear without spalling or fracturing reinforced rebar cages.
What is the allowable beam deflection limit under European FEM 10.2.02 and US RMI MH16.1 codes? +
Under European FEM 10.2.02 and EN 15512 specifications, the allowable vertical deflection of an industrial racking beam under its nominal safe working load (SWL) cannot exceed L/200 for standard pallet storage, and L/250 for automated or narrow-aisle (VNA) systems, where L represents clear beam span in millimeters. For instance, on a standard 2,700 mm beam bay storing two 1,000 kg pallets, the central vertical sag must not exceed 13.5 mm (L/200) or 10.8 mm (L/250). In US RMI MH16.1 codes, deflection is similarly constrained to L/180 or L/240 based on equipment interface. When load is removed, steel components must return to zero without residual plastic deformation. HEDA beams feature multi-claw high-strength interlocking connectors that transfer bending moments directly into upright columns to maintain strict deflection control.
How does chemical pretreatment prevent structural corrosion in humid coastal warehouses and cold chain stores? +
Standard paint applied directly over raw steel will blister and peel due to surface mill scale and oil traces. At HEDA Shelves, we utilize a continuous 9-stage automated chemical immersion bath: alkaline degreasing, twin water flushes, acid rust pickling, neutralizing rinse, micro-crystalline zinc phosphating, and passivating seal. Phosphating converts the outer steel layer into a chemically stable, insoluble non-metallic crystalline phosphate conversion coating. When electrostatic thermosetting epoxy-polyester hybrid powder is applied and cured at 200°C, the film reaches 60–90 microns in thickness, resisting up to 500+ hours in ASTM B117 salt spray tests. For sub-zero cold rooms (-30°C) where condensation and sublimation occur continuously, or open maritime yards, we provide full hot-dip galvanization conforming to ISO 1461 / ASTM A123, ensuring zinc barrier protection up to 80–100 microns thick.
How are racking components packed and strapped to maximize 40HQ container cube utilization and eliminate sea freight damage? +
Freight cost is a key driver of total landed cost. Knock-down pallet racking components are engineered to maximize container cubic space: upright frames are nested with custom wooden and high-density foam dunnage, bolted tightly with high-tensile steel strapping into solid bundles matching the container's 11.9 m interior floor length. Step beams are stacked inversely in interlocking steel-cradled pallets to eliminate wasted voids. Small parts like baseplates, safety pins, row spacers, and anchor bolts are packed in heavy-duty poly-woven sacks inside fumigated wooden crates. This packaging method yields up to 26–28 metric tons or 64–67 cubic meters per 40ft High Cube container, reducing freight cost per pallet position while protecting components against container moisture during ocean transit.
What structural differences distinguish cold-formed roll steel profiles from standard hot-rolled structural channels? +
Cold-formed roll steel (such as EN 10025 grade Q235B / Q355B coils) undergoes room-temperature continuous profile rolling through multi-station precision rollers. This work-hardens the steel and increases yield strength at structural corners without adding dead weight. It creates complex, high-rigidity geometric profiles like 12-bend omega uprights with integrated stiffening ribs. Hot-rolled structural channels (such as UPE, HEA, or I-beams) have thicker walls and higher mass, which increases dead-weight loading on building foundations. Cold-formed steel profiles provide an optimized strength-to-weight ratio, allowing 50mm pitch adjustability, integrated safety locking hooks, and lower total raw material expenditure for standard to heavy-duty high-bay installations up to 30 meters high.
How can warehouse facilities maintain operational stock throughput during unpredictable national electrical grid blackouts? +
When operating in emerging frontier markets where power stability fluctuates, high-tech automated cranes (ASRS) without massive diesel generator plants risk freezing warehouse operations. To guarantee operational continuity, HEDA engineering specifies mechanical gravity flow systems and semi-automated radio shuttles. Gravity pallet flow racks operate on clean kinetic physics—utilizing 3% to 4% pitched roller lanes with speed-brake dampening rollers that guide pallets smoothly without electrical input. For high-density deep-lane layouts, Radio Shuttle systems operate via internal swappable LiFePO4 or lead-crystal batteries; a single pair of hot-swap batteries charges on small solar or auxiliary generators while shuttles operate continuously inside lanes, decoupling warehouse throughput from national grid stability.
What specific warehouse details are required for HEDA engineers to return a free CAD and 3D layout within 24 hours? +
To design an optimized floor plan and structural calculation, our engineering team requires: (1) Warehouse architectural drawings showing internal lengths, widths, column grid spacing, fire escape pathways, dock doors, and building clear height below the lowest overhead truss or sprinkler pipe; (2) Pallet specifications including width, depth, overall height including cargo overhang, and maximum pallet gross weight; (3) Operational inventory data including total SKU counts, fast-mover versus slow-mover turnover rates, and preferred picking logic (FIFO vs. LIFO); (4) Material handling equipment (forklift) model numbers, minimum turning aisle widths (AST), and maximum mast lift reach; (5) Local site seismic acceleration coefficients and floor slab concrete thickness if available.
What is the standard engineering warranty and structural testing protocol for export shipments? +
Every industrial racking system manufactured by Guangzhou Heda Shelves Co., Ltd. is backed by an engineering structural warranty against material delamination, weld failure, or manufacturing defects when operated within specified safe working load (SWL) limits. Our quality assurance protocol includes destructive testing of beam-end connectors on specialized dynamic hydraulic rigs, tensile testing of raw coil coupons, and coating thickness adhesion tests (cross-hatch cutter test under ISO 2409). Clients receive full Mill Test Certificates (MTC 3.1) with each shipment, third-party SGS or BV inspection reports upon request, comprehensive load distribution signboards for beam bays, and step-by-step 3D assembly diagrams for local installation teams.
Plan Your Storage Facility with Certified Structural Engineers
Bypass standard retail resellers and consult directly with our manufacturing engineering division in Guangzhou. Receive full AutoCAD layouts, 3D structural visual renders, and precise container-optimized freight simulations engineered specifically for your building parameters and pallet logistics workflow.
- 24-Hour Express CAD & 3D Turnaround
- Finite Element Load Calculations (FEM / RMI)
- Direct Factory-Door Ocean Export Container Loading
- On-Site or Remote Installation Technical Direction