Engineered Warehouse Racking Portfolio
Custom-fabricated storage architectures compliant with international AS4084, FEM 10.2.02, and EN 15512 safety protocols. Designed to eliminate bottlenecks in distribution centers worldwide.
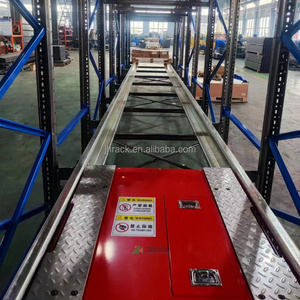
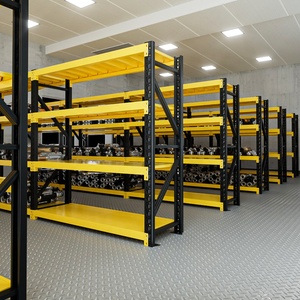
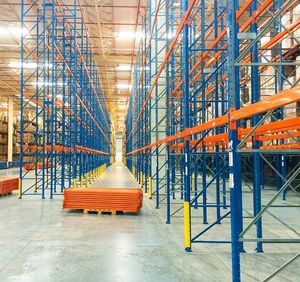
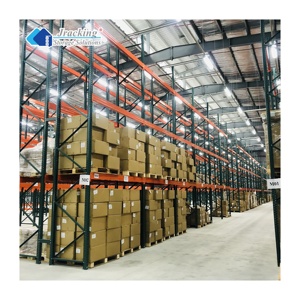
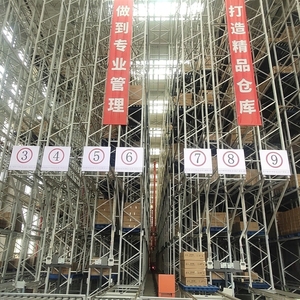
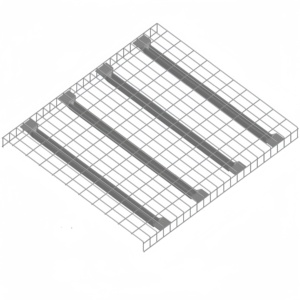
Precision Gravity Flow Engineering: Transforming Static Footprints into Dynamic Throughput
In high-density e-commerce picking, pharmaceutical logistics, and cold-chain FMCG fulfillment, floor space costs dictate that every square meter must generate maximum picking velocity. Flow rack picking systems—comprising carton flow tracks and heavy-duty pallet flow gravity beds—solve the core flaw of conventional selective racking: dead travel time. By separating loading corridors from order picking aisles, gravity-fed flow racks provide a continuous, autonomous replenishment buffer governed strictly by First-In-First-Out (FIFO) mechanics.
At Guangzhou Heda Shelves Co., Ltd., dynamic flow racking systems are not merely static metal structures; they are kinetic machines calculated with micro-tolerances. The downward trajectory of stored SKUs is governed by three critical dynamic variables: the kinetic coefficient of friction (µk) between the carton or pallet runner and the roller beds, the controlled gravitational incline angle (typically calibrated between 2.5% and 5.0% depending on the tare weight and bottom deflection), and the deceleration profiles engineered through internal centrifugal brake drums.
- Zero-Energy Autonomous Replenishment: Eliminates forklift congestion in active order selection zones by decoupling induction and pick faces.
- Calibrated Dynamic Roller Retarders: Prevents excessive speed buildup on lanes deeper than 3 pallets, ensuring smooth docking at terminal stop plates.
- Integrated Ergonomic Pick Shelves: Tilt-shelf configurations positioned at 15° to 25° angles present carton contents directly to pickers, reducing spine torque and picking cycle times by up to 38%.
- High-Tensile Cold-Rolled Forming: Uprights, beams, and track runners cold-formed from certified Q235B and Q355B structural steel for permanent deflections below 1/1000 under maximum rated load.
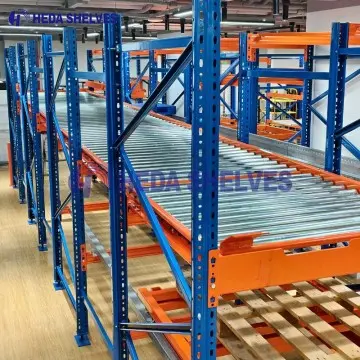
Engineering Specification Matrix: Dynamic Flow vs. Static Storage Architectures
Standard: EN 15512 / RMI 2023 Compliant| System Architecture | Dynamic Bed Technology | Optimal Incline % | Throughput Index (Picks/Hour) | Floor Space Utilization | FIFO / LIFO Protocol |
|---|---|---|---|---|---|
| Carton Flow Racking | Aluminum / Steel Polycarbonate Roller Tracks | 3.0% – 5.5% Gradient | 450 – 750 Lines/Hour | Up to 75% Floor Recovery | Strict FIFO |
| Pallet Flow (Gravity Bed) | Full-Width Steel Rollers + Centrifugal Brakes | 2.8% – 3.8% Gradient | 80 – 140 Pallets/Hour | Up to 85% Density Factor | Strict FIFO |
| Radio Shuttle Automation | Bidirectional Self-Powered Carrier Tracks | 0.0% (Level Railing) | 100 – 160 Pallets/Hour | Up to 90% Ultra-Dense | FIFO or LIFO Switchable |
| Push Back Racking | Telescopic Gravity Nested Carts / Sloped Rails | 2.0% – 3.0% Incline | 40 – 70 Pallets/Hour | 65% – 70% Medium Density | Strict LIFO |
| Selective Pallet Racks | Static Structural Load Beams | 0.0% (Static) | 25 – 45 Pallets/Hour | 35% – 45% (Aisle Dependent) | Random Selectivity |
End-to-End In-House Fabrication: Why Precision Tooling Matters in Flow Systems
A dynamic flow rack cannot tolerate dimensional variances. Unlike static shelving where a 2mm misalignment across a beam bay is absorbed by the clearance margins, a 1.5mm deviation on a carton flow lane or gravity pallet track induces roller binding, tracking drift, and carton jams. As one of China's premier racking exporters operating a self-contained 30,000 square meter facility in Guangzhou, Heda Shelves eliminates these critical risks through automated cold roll-forming and robotic assembly lines.
Our raw coils are procured exclusively from top-tier Chinese domestic steel manufacturers (Baosteel and Shougang Group) with guaranteed metallurgical yield strengths exceeding 235 N/mm² (Q235B) and 355 N/mm² (Q355B). Automated CNC punching presses deliver hole centers with an absolute tolerance of ±0.1mm, ensuring that connector brackets, drop-in dividers, and lane retainers achieve flawless, perpendicular locking. Furthermore, our automated surface treatment line applies an acid pickling and phosphating process prior to thermosetting electrostatic powder coating. This provides a resilient 70–90 micron dry film thickness (DFT) that withstands tropical coastal humidity, extreme warehouse heat, and sub-zero cold room environments without chipping or oxidizing.
- Direct Factory Quality Control: Every phase—from raw coil slit cutting to robotic welding and final load-testing—is monitored under ISO 9001:2015 standards.
- Verified CE Certification (No. 2435-CPR-8605159): Compliance with the Construction Products Regulation for structural metalwork and steel shelving safety.
- Container-Max Knock-Down Packing: Every shipment is 3D-simulated in CAD to maximize volumetric payload inside 40HQ ocean containers, directly lowering landed logistics overhead per pallet position.
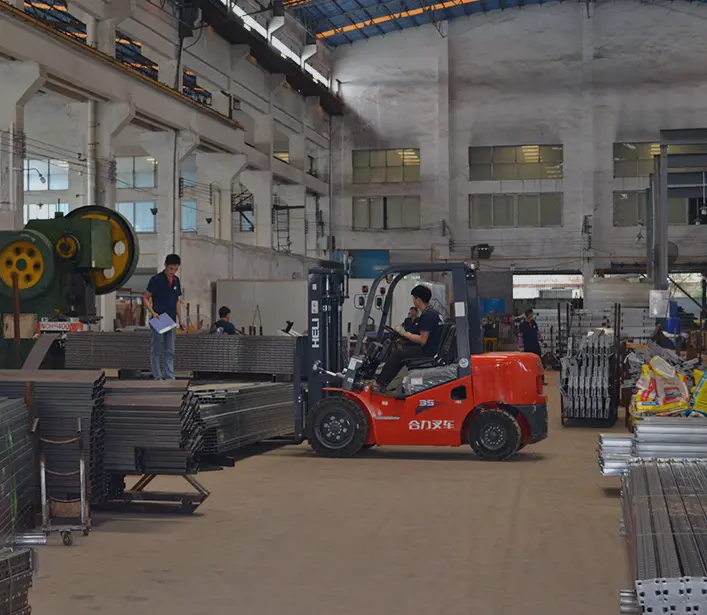
Inside Heda Shelves' 10-Stage Quality Control Pipeline
Precision manufacturing guarantees that every dynamic roller track, pallet stop, and load-bearing beam functions reliably across decades of continuous shifts.










Future Procurement Trends in Flow Rack Picking Systems (2025–2030)
As smart warehousing and rapid e-fulfillment evolve, dynamic flow rack procurement is shifting from standalone mechanical shelving to modular, digitally integrated picking infrastructure.
1. Plug-and-Play Pick-to-Light (PTL) Integration
B2B warehouse operators increasingly specify carton flow beds with integrated aluminum wireways and snap-in clip brackets designed specifically for Pick-to-Light (PTL), Put-to-Light, and optical picking sensors. Modern flow tracks engineered by Heda now feature pre-channeled profiles that prevent cable snagging, allowing logistics integrators to achieve 99.98% inventory selection accuracy without modifying the physical rack frame post-installation.
2. AMR Induction & Automated Replenishment Interfaces
The convergence of dynamic gravity beds with Autonomous Mobile Robots (AMRs) represents the next frontier in split-case picking. Modern procurement specifications demand load-bearing intake funnels and magnetic guidance plates at the rear replenishment aisle. AMRs or automated lifters deposit tote bins directly onto gravity lanes, while human pickers or collaborative picking arms pull items from the front face with zero cross-aisle traffic.
3. Modular Multi-Tier Pick Towers (Mezzanine Synthesis)
Warehouse land leasing rates across Africa, Europe, and the Middle East are accelerating the deployment of multi-tier rack-supported mezzanine platforms integrated with carton flow picking systems. By stacking 2 to 4 tiers of carton flow beds vertically over a heavy-duty structural base, warehouses triple or quadruple pick face counts within the exact same structural footprint, all serviced by vertical spiral gravity chutes and belt conveyors.
4. High-Wear Hybrid Polycarbonate & Steel Roller Tracks
Traditional plastic wheels crack under repetitive shock loading from metal totes or unyielding wooden runners. The latest manufacturing trend pioneered by Heda utilizes high-impact, virgin polycarbonate blended with ABS resin mounted on zinc-plated cold-drawn steel axles. For heavy pallet flow, engineered triple-rib steel rollers with permanently lubricated, double-sealed ball bearings ensure smooth rolling down to -30°C in blast freezers.
5. Sustainable Sourcing & Knock-Down Packaging Optimization
With ocean freight volatility and strict carbon-footprint reporting, international buyers now evaluate racking factories on volumetric shipping efficiency. Heda's modular flow systems ship 100% knock-down, nested into high-density steel bundles secured by heavy-gauge strapping. This packing engineering minimizes dead space inside 40ft High Cube containers, allowing up to 26 metric tons of certified racking steel to be transported per container.
6. Parametric 3D Layout Simulation & Digital Twins
Procuring overseas racking without verified spatial simulation introduces immense installation risk. Leading suppliers provide comprehensive AutoCAD engineering, 3D DWG modeling, and dynamic load stress calculations prior to steel coil slitting. Heda Shelves delivers complete 3D layout simulations within 24 hours of receiving warehouse blueprints, verifying column clearances, door openings, and forklift turning radii.
Engineering Reliability Built Over Two Decades
Supplying mission-critical warehousing systems to over 120 countries across Africa, Southeast Asia, the Americas, and Europe.
25 Years of Manufacturing Mastery
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has delivered more than 10,000 comprehensive warehouse projects globally. Our deep domain expertise ensures structural reliability, precision tolerances, and tailored flow geometry that prevents warehouse downtime.
Verified CE & ISO 9001 Certifications
Structural reliability is non-negotiable. Heda holds official CE Certification (Certificate No. 2435-CPR-8605159), ISO 9001:2015 Quality Management accreditation (No. 18624Q00169R0M, valid to 2027), and RoHS environmental compliance, meeting strict EU and US engineering codes.
30,000 Tons Monthly Output Capacity
With an extensive 30,000 m² factory equipped with automatic cold bending lines, laser cutting centers, robotic welding cells, and continuous powder coating tunnels, we consistently maintain high-volume export schedules, preventing logistical delays on mission-critical projects.
Frequently Asked Questions: B2B Flow Rack Sourcing
Technical guidance for supply chain managers, warehouse design consultants, and procurement directors importing racking systems from China.
The slope angle is determined by the SKU package material, total payload weight, and bottom runner consistency. Standard carton flow racking operates effectively at a 3.0% to 5.0% gradient (approximately 30mm to 50mm drop per linear meter of track). Plastic totes and rigid plastic bins require less slope (approx. 2.5% to 3.0%), whereas corrugated cartons with center deflection or soft bases require 4.0% to 5.5%. For pallet flow racking handling 500kg to 1,500kg pallets, we engineer a 3.0% to 3.8% slope accompanied by centrifugal speed controllers every pallet position to ensure safe, controlled descent.
For ambient indoor warehouses, our multi-stage chemical pretreatment (acid pickling and zinc phosphating) followed by an electrostatic thermosetting polyester powder coating (70–90 µm thickness) provides superior scratch resistance and salt-spray durability. For cold chain blast freezers (-25°C to -30°C) or open-sided coastal warehouses in Africa and Southeast Asia where condensation is prevalent, we recommend pre-galvanized upright frames combined with hot-dip galvanized (HDG) roller tracks and stainless steel roller axles to permanently prevent galvanic corrosion and paint delamination.
Yes, absolutely. Unlike fully automated ASRS cranes that halt entirely during electrical blackouts, gravity-fed carton flow and pallet flow racking systems are 100% mechanical. They harness natural gravity and kinetic braking mechanisms to move inventory continuously to the pick face, requiring zero electrical input. For automated facilities pairing flow racks with Radio Shuttle carts, Heda supplies high-capacity industrial lithium battery packs that deliver 8 to 10 hours of continuous operation with fast solar/generator recharging capabilities.
To generate a turn-key layout proposal, our engineering team requires: (1) Architectural drawings showing internal building dimensions, clear height under roof trusses, column locations, and fire exit door placements; (2) Detailed SKU dimensions (Width × Depth × Height) and tare weights (minimum, average, maximum); (3) Packaging characteristics (cardboard carton, plastic bin, wooden GMA/Euro pallet); (4) Material handling equipment specifications, including forklift mast collapsed height, maximum lift height, and minimum aisle turning radius; and (5) Intended throughput goals (SKU line count and required daily dispatch cycle).
Dynamic components are sensitive to transit vibrations. Flow roller tracks and intermediate dividers are grouped into standardized bundles, cushioned with high-density EPE foam wrapping, and nested inside reinforced corrugated channel supports. Heavy upright frames and step beams are bundled with industrial steel banding and supported by heavy-duty wooden skids designed for easy forklift unloading. Hardware, roller accessories, and brake retarders are boxed in export-grade wooden cases, preventing transit shifting, water ingress, and mechanical deformation inside ocean containers.
Every component manufactured by Heda is CNC-punched and tagged with a unique alphanumeric identifier corresponding directly to the provided 2D assembly blueprints and 3D exploded view schematics. We supply comprehensive installation manuals and high-definition video walkthroughs. For complex installations, such as multi-tier rack-supported mezzanines or automated shuttle networks, Heda provides senior structural installation engineers on-site to oversee local labor teams, perform torque verification, and conduct final dynamic load acceptance testing.