Engineered Pallet Flow & High-Density Racking Systems
Explore our certified heavy-duty warehouse racking solutions. Manufactured from premium Q235B and Q355B cold-rolled structural steel, our dynamic and static configurations maximize volumetric density while securing uninterrupted FIFO stock rotation.
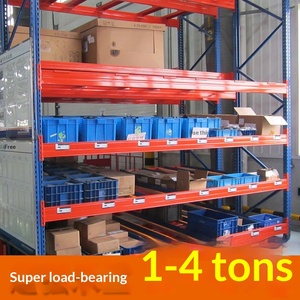
- Load Rating: 800–2,000 kg/Pallet
- Flow Track: Dynamic Brake Rollers
- Gradient: 3.0% – 3.5% Incline
- Material: Q355B Structural Steel
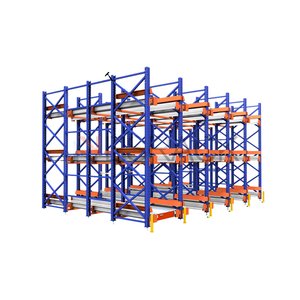
- Shuttle Speed: Up to 1.1 m/s (Loaded)
- Lane Depth: Up to 50 Pallets Deep
- Battery: LiFePO4 8–10h Runtime
- Control: Industrial RF Remote
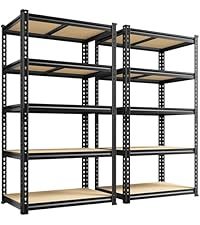
- Capacity: 300–800 kg/Tier
- Assembly: 100% Interlocking Boltless
- Coating: Epoxy Powder Coated
- Upright Pitch: 50mm Increments
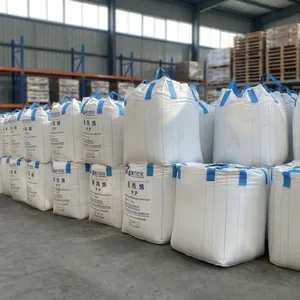
- Melt Flow Rate: 25 g/10min Standard
- Application: Storage Bins & Rollers
- Impact Strength: High Tensile Modulus
- Packaging: 25kg Export Kraft Bag
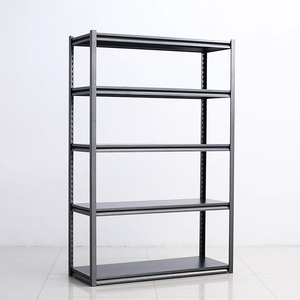
- Shelf Decking: Cold Rolled Steel Deck
- Level Loading: 400–600 kg/Level
- Corrosion Proof: Pickled & Phosphated
- Adjustment: Keyhole / Teardrop Slots
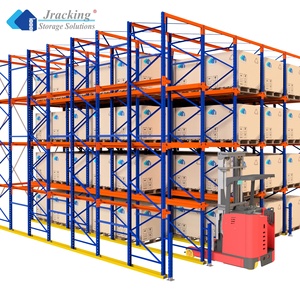
- Pallet Access: 100% Selective Direct
- Bay Capacity: Up to 24,000 kg/Bay
- Standard: CE EN 15512 / FEM Compliant
- Forklift Types: Counterbalance, Reach, VNA
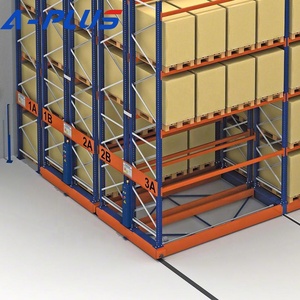
- Floor Efficiency: 85% Floor Surface Gain
- Operation: PLC / Optical Safety Sensors
- Rails: Recessed Steel Guide Rails
- Cold Storage: Rated to -30°C Freezers
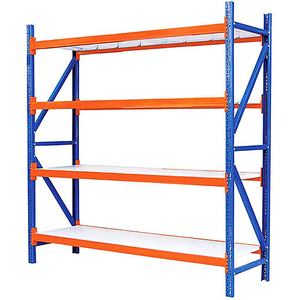
- Finish: Anti-Corrosive Powder Coat
- Upright Type: C-Section Profile Steel
- Flexibility: Rapid Beam Repositioning
- Usage: Manual / Small Goods Picking
| Racking Architecture | Stock Rotation Strategy | Floor Space Utilization | Selectivity Ratio | Optimal Handling Unit | Capex vs. AS/RS |
|---|---|---|---|---|---|
| Live Pallet Gravity Flow | Strict FIFO (First-In, First-Out) | 65% – 75% Active Footprint | Lane Selective (Front Pallet) | 1,000–1,500 kg Euro/GMA Pallets | 60% Lower Than Stacker Crane |
| Automatic Radio Shuttle | FIFO or LIFO Configurable | 70% – 85% Active Footprint | Level & Lane Selective | Uniform Pallet Loads ≤ 1,800 kg | 45% Lower Than Miniload/ASRS |
| Selective Pallet Racking | Unrestricted Random Access | 35% – 42% Active Footprint | 100% Immediate Direct Access | Universal SKU Diversity | Standard Industry Baseline |
| Electric Mobile Racking | Random Direct Access (Single Aisle) | 80% – 88% Active Footprint | 100% Selectivity (Dynamic Aisle) | Heavy Pallets / Cold Store Goods | 30% Lower Than Full Automation |
Kinematics, Structural Physics & Design Standards of Live Storage
A technical examination of gravitational roller beds, kinetic energy dissipation, and EN 15512:2020 compliance for heavy industrial live storage operations.
Gravitational Flow Incline Dynamics
Live pallet racking systems convert static gravitational potential energy into controlled kinetic transit via an engineered floor pitch ranging precisely between 3.0% and 3.5% (approx. 1.7° to 2.0°). This inclination gradient overcomes static inertia across wooden, plastic, or composite pallet bottom-decks without risking runaway acceleration. Rollers are spaced along the bed according to pallet runner contact patches, guaranteeing minimum 3-point runner engagement at all cycle positions to eliminate sagging deflection.
Centrifugal Speed Controller Calibration
Uncontrolled mass acceleration creates catastrophic impact risks against discharge stops. Our factory integrates sealed centrifugal speed controller rollers positioned at 1-pallet intervals along every gravity lane. These internal flyweight braking units act mechanically without electrical wiring. Internal friction brakes engage proportionally as velocity surpasses 0.30 m/s, keeping pallet momentum safely moderated between 0.15 m/s and 0.25 m/s, irrespective of pallet weights ranging from 300 kg to 1,500 kg.
Pallet Separation & Mast Isolation
In deep gravity lanes carrying 10 to 25 pallets, cumulative backline pressure against the discharge pallet can exceed 25,000 kgf. To eliminate forklift binding and catastrophic pallet ejection, our engineering incorporates automatic mechanical pallet separators. When the front pallet reaches the discharge end-stop, a mechanical trip arm locks the subsequent pallets behind a retention barrier. Forklift operators retrieve the primary pallet completely free of trailing load pressure, triggering a safe sequential release.
Global Warehouse Trends Shaping Pallet Racking Procurement
Strategic analysis for supply chain directors, procurement officers, and warehouse logistics planners navigating rising footprint costs and industrial automation.
Volumetric Densification Over Footprint Expansion
Surging global industrial warehousing rental rates have accelerated the retirement of single-selective racking in high-velocity sectors. Logistics operators are converting existing 10–12m clear-height spaces into live gravity pallet flow and multi-tier mezzanines, effectively doubling or tripling pallet slot density within existing building perimeters without requiring new municipal zoning or construction capex.
Zero-Energy Storage Resilience vs. Fully Automated AS/RS
While automated storage and retrieval systems (AS/RS) provide automated velocity, their continuous kilowatt consumption, vulnerability to local utility power failures, and high maintenance overhead have pushed cold-storage and FMCG operators toward passive gravity live flow racks. Mechanical roller dynamics require zero continuous electricity, guaranteeing full throughput integrity during grid interruptions.
Sub-Zero FMCG & Pharmaceutical Cold Chain Explosion
Refrigerated cubic capacity is the world's most capital-intensive warehouse space. Temperature-controlled warehouses across North America, Europe, Southeast Asia, and Africa are standardizing on heavy-duty galvanized pallet flow and radio shuttle racking. Maximizing thermal volumetric efficiency directly curtails the kilowatt-hour refrigeration cost per pallet position handled.
Need a comprehensive warehouse layout calculation for your regional distribution center?
Get CatalogGuangzhou Heda Shelves Co., Ltd. Manufacturing Authority
Operating a vertically integrated 30,000 square meter production facility in Guangzhou, China. From raw hot-rolled steel coils to CNC-machined structural columns, we control every metallurgical phase in-house.
10-Stage Metallurgical & Finishing Precision
Our automated production lines eliminate structural tolerances, ensuring seamless on-site bolting and strict adherence to structural deflection tolerances (L/200 to L/300).
Certified Prime Steel
Raw coil testing for yield strength, tensile toughness, and chemical composition (Q235B/Q355B structural grade).
CNC Continuous Punching
High-speed automated punching matrices producing 50mm/75mm pitch upright teardrop and diamond lock slots.
Cold-Roll Section Forming
Multi-stand precision profiling cold-rolls uprights, interlocking box beams, and heavy-duty live roller tracks.
Automated Robotic Welding
CO₂ gas shielded robotic weld cells attach multi-prong connector claws to beams with deep, uniform penetration.
Phosphating & Powder Coat
Full 9-stage degreasing, pickling, and electrostatic thermosetting polyester powder coating baked at 200°C.
Frequently Asked Questions on Live Pallet Flow Racking
Comprehensive engineering clarifications addressing incline geometry, pallet deflection limits, seismic anchoring, and overseas export logistics.