Modular Pallet Racking & Industrial Storage Portfolio
Precision-manufactured structural storage units fabricated from high-tensile certified steel coils. Our systems adhere to rigorous EN 15512 and RMI MH16.1 specifications, providing scalable racking architectures for global 3PL distribution hubs, temperature-controlled facilities, and industrial manufacturing plants.
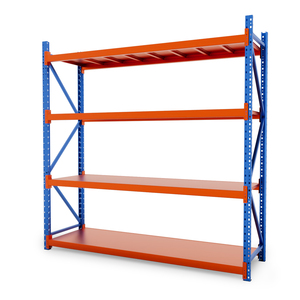
Wholesale Heavy Duty Pallet Rack 3000kg High Load 4 Layer Metal Shelves Durable Longspan Pallet Racking
- Payload: Up to 3,000 kg / beam level
- Profile: 50mm pitch adjustable box beam
- Standard: EN 15512 & CE Certified
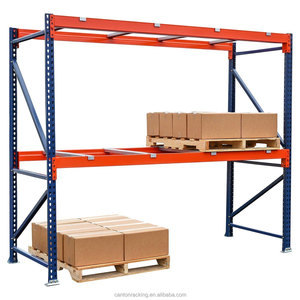
Metal Shelving Units and Heavy-Duty Storage Shelves in Modular Multi-Tier Dimensions
- Capacity: 500–1,200 kg / tier
- Assembly: Boltless interlocking claw lock
- Decking: Galvanized steel or wire mesh
Herschel Heavy-Duty Industrial Steel Fabric Roll Storage Custom Warehouse Pallet Racking
- Application: Cylindrical rolls, textiles, coils
- Saddle brackets: Anti-roll concave rests
- Steel Grade: Certified Q235B cold rolled
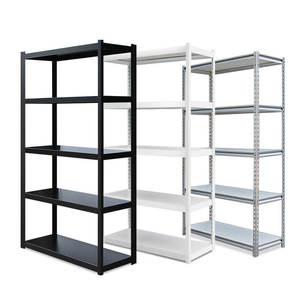
Mracking Customizable Light Slotted Angle Shelving Systems for Retail & Light Warehouses
- Uniform Distributed Load: 80–180 kg/tier
- Pattern: Precision punched angle post
- Surface: Multi-color electrostatic powder
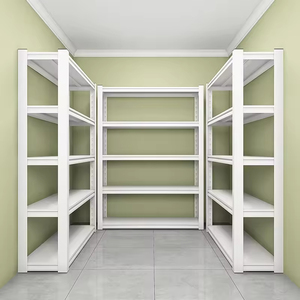
2000×500×2000mm Rapid Knock-Down Assembled Metal Storage Racking 100kg/Tier
- Dimensions: 2000(H) × 500(D) × 2000(L)mm
- Fast Packaging: Flat-pack KD container pack
- Versatility: Rapid warehouse assembly
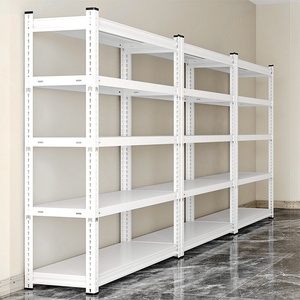
Heavy-Duty Steel Storage Rack Adjustable Corrosion-Resistant Metal Shelving Racks
- Finish: 9-Stage chemical anti-corrosion
- Beam Adjustability: 75mm increment holes
- Safety Locks: Automated drop-in pins
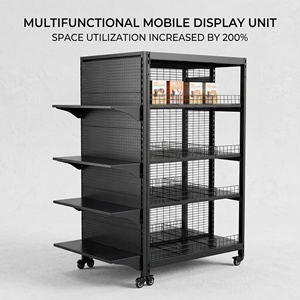
Customizable Metal Gondola Shelving Retail Display Supermarket Aisle Shelves OEM ODM
- Format: Island, single-sided, end-cap
- Accessories: Pegboards, acrylic risers, LEDs
- Branding: Full custom RAL color coatings
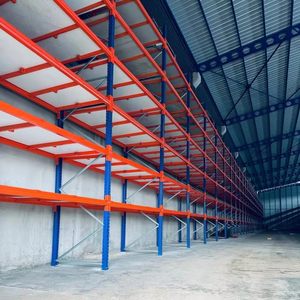
Peterack CE Certified Heavy-Duty Stacking Post Pallet Racks Multi-Layer Warehouse Shelves
- Config: Removable nesting structural posts
- Stacking Height: 4-to-5 tiers dynamic safety
- Capacity: 1,500 kg per pallet cage unit
Tier-1 Direct Manufacturing: From Steel Coil to Global Destination
With over 25 years of specialized mechanical racking fabrication, Guangzhou Heda Shelves Co., Ltd. operates as a vertically integrated manufacturer and premier exporter. Operating from a 30,000 m² facility with a workforce exceeding 300 experienced fabrication engineers, CNC technicians, and certified welders, HEDA produces up to 30,000 metric tons of finished industrial racking monthly.
Every structural member is designed and simulated using finite element analysis (FEA) to ensure zero failure under seismic loading and maximum beam deflection constraints. Certified under CE EN 1090-1 / CPR (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 (Certificate No. 18624Q00169R0M), our direct-factory pipeline eliminates intermediary markups while offering certified mechanical warranties.
Contact UsCompliance & Quality Credentials
Structural Design Standards & Metallurgy Comparison
Modular pallet racking is not simply steel tubing assembled together; it represents safety-critical cold-formed structural engineering. Understanding the metallurgical yield thresholds, profile geometry, and finite element calculations is vital for supply chain directors to mitigate warehouse collapse risks.
| Engineering Parameter | Standard Commodity Tier (Local Markets) | HEDA Industrial Heavy-Duty Specification | International Standard Benchmark |
|---|---|---|---|
| Raw Steel Grade | Commercial Recycled Scrap / Q195 Steel | Prime Continuous Cast Q235B & Q355B Hot-Rolled Coils | EN 10025-2 / ASTM A36 / AS/NZS 3678 |
| Yield Strength (ReH) | 180 – 215 MPa (Inconsistent ductility) | ≥ 235 MPa (Q235B) / ≥ 355 MPa (Q355B) | RMI MH16.1-2021 Section 1.4.1 |
| Maximum Beam Deflection Ratio | L / 120 – L / 150 (Visible sagging risk) | L / 200 (Standard) to L / 250 (ASRS grade) | EN 15512:2020 Limit State Design |
| Upright Section Geometry | 4–6 Bends, Simple Open C-Channel | 8–12 Complex Cold-Bending Facets, Omega Profile | Optimized Buckling Torsional Resistance |
| Surface Chemical Pretreatment | Manual Degrease wipe-down or single rinse | 9-Stage Continuous Automated Pickling & Phosphating | ISO 12944-4 Surface Cleanliness C3/C4 |
| Electrostatic Powder Curing | 40–50 μm thickness, air-dry enamels | 60–90 μm Epoxy-Polyester cured at 190°C–210°C | ASTM B117 500-Hour Salt Spray Proof |
| Safety Factor Threshold | 1.25 : 1 – 1.35 : 1 (Minimal leeway) | 1.5 : 1 (Static) / 1.65 : 1 (Seismic Zone 4) | AS 4084-2023 Structural Integrity |
Automated 10-Stage Factory Fabrication Pipeline
From raw steel coil slit-shearing to high-speed CNC punching, cold-roll profile extrusion, robotic multi-point welding, and computerized powder deposition, our manufacturing workflow guarantees dimensional tolerance within ±0.5mm across entire 12-meter upright upright spans.
Certified Raw Coil
Mill-certified structural steel coils inspected for chemical composition, carbon equivalent, and tensile elasticity.
Precision Slitting
Automated uncoiling and high-speed rotary slitting into exact development widths for continuous cold-forming feeds.
CNC Axis Punching
Continuous hydraulic CNC punch-press producing teardrop, diamond, or butterfly slots on precise 50mm/75mm pitches.
Multi-Roll Forming
18 to 24-station cold-rolling mills shaping open omega columns and interlocking box beams with zero micro-cracking.
Robotic Welding
Multi-axis ABB robotic welding cells fusion-welding beam end-connectors with argon gas shielded integrity.
Chemical Pickling
Acid immersion tanks removing rolling scale, mill scale, rust, and surface grease down to parent metal pores.
Phosphating Bath
Dense zinc-iron phosphate conversion coating deposited to prevent oxidation and double powder paint mechanical adhesion.
Electrostatic Powder
GEMA automatic reciprocating spray guns applying fine thermoset epoxy-polyester particles uniformly over entire geometry.
Thermal Curing Tunnel
200°C hot air convection crosslinking tunnel forming an impact-resistant, high-durability polymer exterior shell.
Container Cube QC
Laser caliper inspection, bundle strapping, dynamic drop-test verification, and knock-down container cube pack.
Future Procurement Trends in Industrial Pallet Racking
Global supply chain managers are transitioning from transactional, one-off racking purchases to lifecycle-managed, modular, and automation-ready intralogistics ecosystems. We identify the four macro procurement vectors dominating 2025 through 2030.
ASRS & Shuttle-Ready Modularity
Procurement teams are eliminating static selective racking in favor of hybrid designs convertible to 4-Way Radio Shuttle or crane-operated Automated Storage and Retrieval Systems (ASRS) without beam destruction.
Automation MigrationLow-Carbon Recycled Steel (EAF)
Driven by EU CBAM tariffs and corporate ESG targets, tenders now mandate low-carbon footprint cold-formed structural steel produced via Electric Arc Furnace (EAF) recycling, reducing embedded carbon by up to 58%.
Green Steel & CBAMHigh-Bay Multi-Tier Mezzanines
With real-estate land acquisition costs rising globally by 34% since 2021, industrial buyers demand rack-supported multi-tier platforms (up to 4 tiers) to maximize clear vertical heights of 10 to 18 meters.
Cubic Footprint DensificationContainer-Optimized Knock-Down Racking
High ocean shipping volatility has made freight cube utilization a core procurement metric. Modular nesting components engineered for 40ft High Cube containers reduce landed freight costs per pallet position by 22%.
Logistics EfficiencyTechnological & Architectural Racking Trends
Modern pallet storage systems operate at the intersection of structural statics, mechanical tribology, and automation robotics. Discover the critical architectural paradigms changing how warehouse infrastructure is specified.
Finite Element Structural Optimization
Advanced non-linear FEA modeling simulates elastoplastic behavior under asymmetrical pallet shock loads. Multi-faceted cold-rolled profiles disperse torsional stresses along longitudinal flutes, providing higher stiffness with optimized steel mass.
Structural MechanicsMicro-Tolerance Fabrication for Robotics
Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs) require millimeter deflection tolerances. Robotic beam end-connector laser welding guarantees plumbness and elevation variance below ±1.0mm over 50-meter operating aisles.
Robotics ToleranceExtreme Environmental Metallurgical Finishes
In cold chain blast freezers (-30°C) and high-humidity maritime warehouses, standard finishes peel and oxidize. Pre-galvanized coils (Z275 coating) combined with thermal polyurethane powder barriers eliminate condensation corrosion and structural fatigue.
Anti-Corrosion C4/C5Frequently Asked Questions on Importing Modular Racking
Comprehensive engineering and commercial answers to address the operational concerns of international supply chain directors, procurement officers, and third-party logistics operators sourcing directly from China factories.
Every export shipment includes verified Mill Test Certificates (MTC 3.1) stating chemical composition and elongation, third-party tensile coupon test reports, CE Factory Production Control certificate (No. 2435-CPR-8605159 under EN 1090-1), structural static calculation packages verified by finite element analysis (FEA), and stamped installation assembly drawings adhering to EN 15512 or RMI standards.
Racking components are engineered for full knock-down (KD) nested loading. Upright frames are either shipped disassembled with bolted diagonal bracings or stacked with precision interlocking wood bolsters. Horizontal box beams are strapped in high-density bundles using protective cardboard angles and PET strapping. A typical 40ft High Cube container carries between 24 to 27 metric tons of racking, utilizing over 92% of gross container volume.
For seismic regions (such as the Pacific Rim, Latin America, or Southern Europe), our structural engineering team inputs the warehouse geographic spectral acceleration factors (Ss, S1) according to Eurocode 8 or ASCE 7. We expand upright column footplates, incorporate heavy-duty base anchors (M12 to M16 chemical or mechanical wedge anchors), and integrate vertical spine cross-bracing to absorb lateral ground acceleration.
Yes. We offer custom OEM/ODM tooling matching standard American teardrop punching, British Dexion slotted configurations, European 50mm diamond patterns, and Australian 76.2mm pitch slots. By matching the beam end-connector claw geometry and upright pitch, our manufactured components seamlessly expand existing foreign warehouse racking installations without structural compromises.
With 30,000 tons of monthly throughput and dedicated continuous coil stock, our production lead time for standard project sizes (2 to 10 standard 40HQ containers) is 15 to 20 working days from final approved CAD drawing. Custom engineered mezzanine configurations or specialized custom powder paint shades (non-standard RAL) generally require 20 to 25 business days.
We provide a multi-layered deployment package: 1) Stamped, 3D color-coded CAD layouts matching tagged part numbers on each bundle; 2) Step-by-step video installation tutorials demonstrating anchor torque tolerances, column shimming, and beam pin insertion; 3) Remote real-time video guidance from senior project engineers; and 4) Dispatch of multilingual on-site installation supervisors for large-scale multi-tier mezzanine and radio shuttle installations.
Request Free 3D Warehouse CAD Layout & Structural Load Analysis
Submit your warehouse clear ceiling height, slab core drill capacity, pallet dimension profiles, and forklift operating radius. Our engineering department will generate a compliant CAD floor plan, 3D volumetric rendering, and competitive direct factory FOB/CIF quotation within 24 hours.