Featured OEM & Industrial Storage Racking Systems
Engineered for intense material handling operations, cold-chain preservation, dynamic picking facilities, and container-optimized oceanic dispatch across global fulfillment corridors.
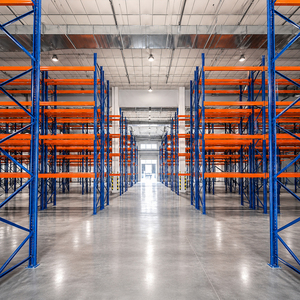 Heavy Duty
 Pallet Rack 1000KG 2000KG Per Level Metal High Density Free 3D Design Q235B Steel Shelving
- Capacity: 1,000–2,000 kg / Tier
- Steel: Certified Q235B Structural
- Finish: Electrostatic Epoxy Polymer
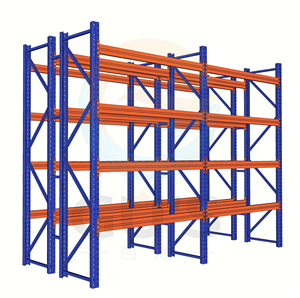 Stacking Unit
Warehouse Pallet Racking Shelves Unit Industrial Heavy Duty Metal Rack Storage Shelf Pallet Stacking Rack System
- Modular Stackable Pallet Frames
- High-Density Bulk Storage Array
- Zero-Bolt Interlocking Assembly
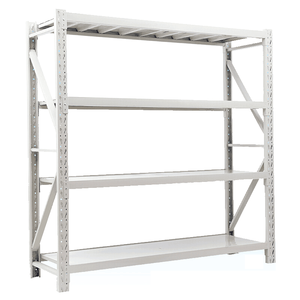 Boltless Rivet
4-Shelf Light Duty Boltless Rivet Shelving Metal Shelf Storage Racks For Garage and Supermarket Shelves HJQ-105
- Model: HJQ-105 Fast Assembly
- Supermarket & Retail Display Use
- Adjustable Double-Keyhole Post
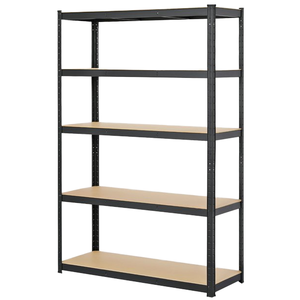 5-Tier System
Electronic Commercial 5 Layer Steel Storage Shelving Racks Heavy Duty Warehouse Shelves Boltless Rivet Rack Easy Assemble
- E-Commerce Order Fulfillment
- 5 Adjustable Tier Configurations
- High Stiffener Steel Decking
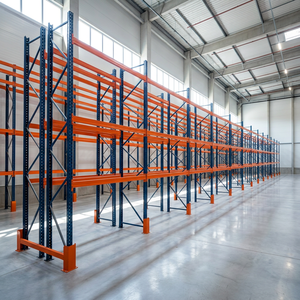 Selective Beam
Garage Warehouse Rack Adjustable Storage Stacking Racks Heavy Duty Racking Factory Selective Rack Warehouse Storage Shelving
- 100% SKU Direct Accessibility
- 75mm / 50mm Pitch Adjustment
- Anti-Dislodgement Safety Pins
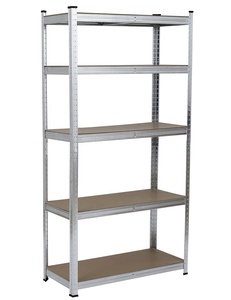 KINDE Industrial
KINDE Racking Shelves Garage Storage Shelves 875KG 180x90x40cm Display Stand Boltless Adjustable Boltless Metal / Rivet Shelving
- 875 kg Total Uniform Load Rating
- Compact Footprint: 180x90x40cm
- Galvanized or Textured Powder Coat
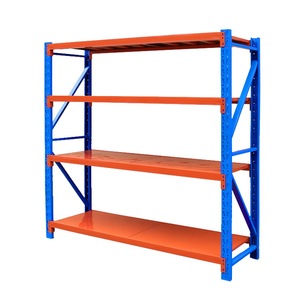 HUAWU Medium
HUAWU Steel Boltless Shelving Rack 2000x600x2000mm 4-Layer 200kg Per Layer Medium Duty Industrial Storage System
- Dimensions: 2000x600x2000mm
- 200 kg / Layer Uniform Capacity
- Multi-Tier Mezzanine Compatible
 Smart Sensing
New Smart Shelf Weight Inventory 4-Layer Heavy Duty Supermarket Shelves for Hotels with 1000kg Capacity
- Integrated Dynamic Weight Sensors
- Real-Time Automated Stock Audits
- 1,000 kg Heavy Load Tolerance
Structural Integrity & Metallurgical Fabrication Standards
An engineering-led analysis of cold roll-formed upright optimization, steel yield criteria, weld penetration reliability, and life-cycle durability in high-throughput distribution environments.
Modern warehouse logistics infrastructure demands rigorous engineering far beyond simple steel shelving. When engineering high-bay selective pallet racks, drive-in systems, or multi-tier rack-supported mezzanines, structural failure is not an option. At Guangzhou HEDA Shelves Co., Ltd., every system is designed and validated according to international structural codes, including RMI (Rack Manufacturers Institute) MH16.1, EN 15512:2020 European specifications, and AS4084-2012 standards.
The foundation of long-term load resilience begins at the raw material phase. We exclusively procure prime structural carbon steel grades—principally Q235B (yield strength $f_y \ge 235 \text{ MPa}$) and high-stress Q355B (yield strength $f_y \ge 355 \text{ MPa}$). By verifying every coil batch using chemical spectral analysis and mechanical tensile testing, our structural engineers ensure zero risk of brittle fractures under extreme dynamic forklift impacts or heavy deadweight consolidation.
Upright columns undergo automated continuous CNC cold roll-forming with multi-station inline dies. This guarantees precise dimensional tolerances within $\pm 0.5\text{mm}$ across a 12-meter profile. The proprietary omega upright geometry introduces localized stiffening ribs along the profile corners, increasing the radius of gyration and effectively elevating the critical elastic buckling threshold by up to 22% compared to standard open-channel profiles.
Horizontal and diagonal bracing configurations utilize high-ductility tubular and C-profile sections. Connected through grade 8.8 tensile bolts and locknuts, they create a robust vertical truss framework capable of absorbing horizontal seismic forces and operational side-sway without permanent inelastic deformation.
Standard engineering practice often adopts a maximum beam deflection ratio of $L/200$ under uniform distributed loading (UDL). In contrast, our OEM production mandates a stricter limit of $L/250$ to $L/300$ for automated handling installations. This significantly mitigates pallet sag, reduces roller wear in gravity flow lanes, and eliminates dynamic harmonic oscillations during seismic events or rapid automated turret truck retrieval.
| Engineering Parameter | Light/Medium Shelving (HJQ/HUAWU) | Standard Selective Pallet Racking | Heavy-Duty Drive-In / Shuttle Racking |
|---|---|---|---|
| Primary Steel Designation | Q195 / Q235B Strip Steel | Q235B High-Tensile Structural | Q355B Alloy-Enhanced Structural |
| Standard Layer Capacity | 150 kg – 400 kg per tier | 1,000 kg – 3,500 kg per beam level | 1,000 kg – 2,000 kg per pallet position |
| Column Section Dimension | 38x38mm / 55x47mm Boltless | 80x60mm to 120x95mm Omega | 90x70mm to 140x100mm Heavy Profile |
| Beam Locking Mechanism | Keyhole / Rivet Slot Press-Fit | 3-4 Claw Connector with Safety Pin | Reinforced Cantilever Top-Tie Arms |
| Surface Protection System | Electrostatically Applied Epoxy | Dual-Pretreated Polyester Powder | Hot-Dip Galvanized (Cold Stores / Yards) |
| Quality Standards Verification | RoHS, In-House Deflection Audits | CE (2435-CPR-8605159), ISO 9001:2015 | EN 15512, RMI MH16.1, CE Compliance |
The 10-Stage Certified Manufacturing Workflow
From prime hot-rolled coils to export-packaged structural bundles, every manufacturing phase is tightly managed in our 30,000 m² Guangzhou production facility.










Future Warehouse Racking Procurement Trends (2025–2030)
How progressive logistics operators, supply chain directors, and regional suppliers are optimizing total cost of ownership (TCO) through modern structural manufacturing.
Knock-Down Shipping Geometry
With ocean freight volatility remaining a key risk factor, global buyers are moving away from pre-welded frames toward precision-bolted, high-density knock-down (KD) designs. By nesting upright profiles and bundled box beams, factory-direct loading density inside 40HQ maritime containers exceeds 88%, drastically cutting landed freight costs per pallet location.
Environmental Durability & Zinc Alloys
Corrosion degradation in humid tropical coastal zones and sub-zero cold chain logistics is accelerating the phase-out of traditional single-coat liquid finishes. Procurement specifications increasingly require mandatory multi-stage acid pickling, zinc phosphating, or pre-galvanized high-yield strip steel to prevent sub-film oxidation and eliminate structural fatigue over 15+ years.
Hybrid Automation & Sensorization
Rather than choosing between basic manual racking and multimillion-dollar automated storage systems (ASRS), enterprises are embracing hybrid middle-ground solutions. Semi-automated radio shuttle lanes and IoT-enabled weight-sensing inventory shelves offer real-time ERP synchronization, zero operator aisle entry, and continuous operations through power fluctuations.
Why Global Distributors & EPC Contractors Partner with HEDA
Integrating 25 years of engineering manufacturing with direct OEM supply contracts, dedicated CAD design teams, and verified compliance credentials.
Free 3D Layout & CAD Design
Our certified structural engineering department provides complimentary CAD floorplans, 3D parametric renderings, and load capacity simulations within 24 hours of receiving site dimensions.
Verified Certifications
Fully accredited with CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M valid through June 2027), and international RoHS material safety compliance.
Full OEM/ODM Customization
Complete flexibility across post profiles, beam hook configurations, custom corporate RAL colors, branding stencils, seismic anchor brackets, and specialized wire mesh or steel panel inserts.
Containerized Ocean Logistics
Factory loading optimization ensures maximum tonnage and volume balance for 20GP and 40HQ containers, reducing landed cost per pallet position with worldwide port-to-port documentation.
Frequently Asked Questions for Project Engineers & Buyers
Clear, direct technical answers covering structural calculation, corrosion prevention, installation supervision, and quality assurance.
What core site data is required to generate a 3D CAD layout?
To deliver an accurate layout and structural calculation, our engineering team needs: (1) Warehouse architectural drawings indicating clear height under trusses, column grids, dock doors, and floor slab load capacity; (2) Pallet dimensions including width, depth, overall height, and maximum gross weight per pallet; (3) Forklift model, minimum turning aisle width requirement, and maximum mast lift reach; (4) Total SKU profile and daily pallet throughput targets.
How does HEDA guarantee long-term corrosion resistance in humid climates?
All structural steel components undergo an automated, ten-step pretreatment line that includes immersion degreasing, multi-stage acid pickling to eliminate mill scale, and zinc phosphating to establish an inert bonding substrate. We then apply an electrostatic thermosetting polyester powder coating baked at 180°C–200°C. For coastal warehouses, fertilizer storage, or blast-freezer operations, components can also be specified with hot-dip galvanization.
Which storage systems operate reliably during regional electrical outages?
Purely mechanical solutions operate with 100% independence from the power grid. These include selective pallet racking, double-deep setups, drive-in systems, push-back gravity carts, and pallet flow racking. For semi-automated operations using radio shuttles, carrier units feature high-capacity lithium battery packs that can be charged during standard generator or off-peak solar windows.
What is the standard production lead time and shipping packaging format?
Standard production cycles for orders between 1 to 5 forty-foot high cube (40HQ) containers run 15 to 22 calendar days. All beams are bundle-strapped with heavy-gauge PET banding and corner protectors. Upright frames are either knock-down nested with shock-absorbing timber spacers or shipped as fully welded structural panels, optimizing maritime container space and simplifying unloading.
How are international installation and assembly supported on-site?
Every shipment includes complete numbered component lists, 3D exploded assembly diagrams, frame bracings, and torque specifications for anchor bolts. We offer remote video supervision during upright erection and plumb-line levelling. For major logistics distribution hubs or multi-tier mezzanines, we can also dispatch factory project engineers directly to your site to oversee local installation teams.
Can you provide custom RAL color-coding and private label OEM branding?
Yes. We regularly produce custom OEM batches matching specific client corporate palettes—such as Safety Orange (RAL 2004), Signal Blue (RAL 5005), Traffic Yellow (RAL 1023), and Anthracite Grey (RAL 7016). Upright post caps, beam face stencils, and load capacity safety plaques can also be customized with your brand logo, corporate identity, and certified load data.