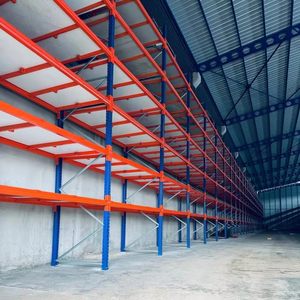
Heavy-Duty Stacking
CE Certified
Multi-Layer
Post-Stackable
Engineered with Q235B high-tensile steel, robotic multi-pass welding, and 10-stage electrostatic powder coating for maximized volumetric density and safe operational load capacity.
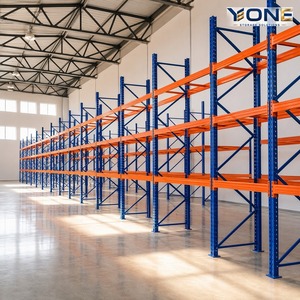
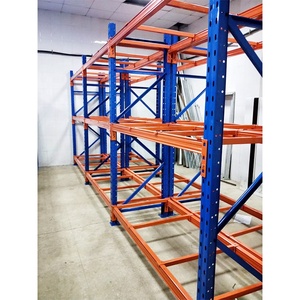
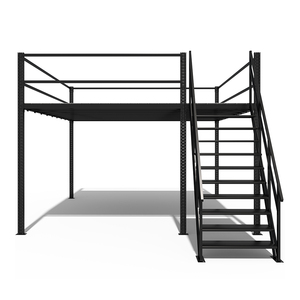
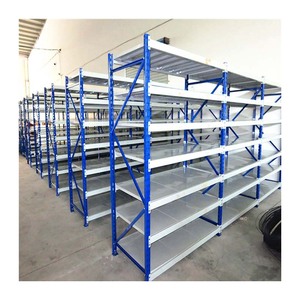
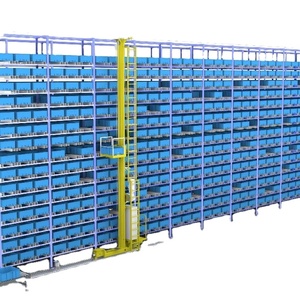
Industrial warehouse storage systems are critical structural installations subject to static, dynamic, and seismic forces. In modern high-density distribution centers, selecting the right custom OEM warehouse shelving storage supplier is not merely a purchasing transaction—it is a life-safety and operational continuity decision.
At Guangzhou Heda Shelves Co., Ltd., our engineering methodology bridges mechanical engineering, cold-formed steel metallurgy, and intralogistics architectural planning. We manufacture primarily with certified prime Q235B and Q355B structural carbon steel, chosen for their superior yield strengths (minimum 235 MPa and 355 MPa respectively), ductile elongation ratios, and optimal chemical composition for cold continuous roll-forming.
Under heavy cyclic loading, inferior secondary steel or inconsistent coil gauges can cause progressive micro-cracking at column punch points or flange radiuses. To prevent premature fatigue and local column buckling under eccentric loading, our upright columns feature custom continuous omega (Ω) and teardrop structural profiles roll-formed through 22 to 26 successive roller stations. Every punch slot—spaced accurately at 50mm, 75mm, or 76.2mm pitch—is executed using automated optical-guided hydraulic punching dies to maintain dimensional tolerances within ±0.15mm across an 11.8-meter single-section upright.
Under maximum design working load (UDL - Uniformly Distributed Load), horizontal beam deflections are strictly engineered to remain below L/200 (commercial) and L/300 (heavy automated AS/RS applications), preventing dangerous load shifting or premature beam lock disengagement.
Beam-to-column connections are engineered using robotic dual-wire gas metal arc welding (GMAW). The beam connectors utilize multi-prong cold-stamped claws with integrated mechanical safety locking pins (minimum 8kN shear resistance) that prevent accidental upward beam displacement during forklift extraction operations.
Off-the-shelf catalog shelving forces warehouse operators to compromise on pallet bay clearances, forklift aisle turn radiuses, and building clear heights. Our full OEM/ODM manufacturing capability ensures that your racking system is custom-designed around your precise operational constraints:
From prime hot-rolled steel coils to ocean-worthy containerized shipping, every processing stage is subjected to rigorous quality gates, non-destructive testing, and micrometer-calibrated dimension checks.
Mill-certified prime Q235B/Q355B steel coils verified via spectral metallurgical analysis for carbon, manganese, and phosphorus content.
Automated uncoiling, flattening, and high-speed CNC rotary shearing to exact section blanks with burr-free edges.
High-tonnage progressive die presses punch pitch holes in single-stroke operations ensuring absolute slot pitch consistency across all uprights.
Gradual cross-sectional deformation across 22+ hardened steel forming rollers to create rigidity-optimized open and box beam profiles without micro-fracturing.
Laser-calibrated flying saws cut roll-formed beams and uprights dynamically to customer specified warehouse heights up to 12,000mm.
High-energy vibratory finishing and centrifugal shot blasting to remove scale, slag, and edge irregularities to ensure coating adhesion.
Robotic arms perform continuous multi-pass welds on beam connectors and baseplates, delivering uniform penetration without porosity.
Chemical immersion through multi-stage acid baths removes all oxidation, creating an insoluble micro-crystalline zinc-phosphate conversion layer.
Automated reciprocator spray booths apply thermoset epoxy-polyester powder (80–120μm thickness) baked at 200°C for high chemical and abrasion resistance.
Cross-hatch adhesion testing, ultrasonic weld inspection, component barcoding, and heavy-duty strapped wooden bundling optimized for 20GP/40HQ loading.
Combining 25 years of structural racking manufacturing with global logistics insight, our facility serves importers, logistics contractors, and multinational distributors in over 120 countries.
Our manufacturing processes and structural designs are independently audited and certified under CE Certification No. 2435-CPR-8605159, ISO 9001:2015 Certification No. 18624Q00169R0M (valid through June 2027), and strict RoHS chemical safety compliance for all surface treatments.
Never risk improper bay spacing or column collisions. Our experienced structural engineering team provides complete warehouse floor layout optimization, AutoCAD 2D structural floor plans, realistic 3D isometric renderings, and verified point-load calculation calculations free of charge prior to contract confirmation.
International shipping costs can make or break storage project ROI. We engineer our upright columns, beams, step decking, and bracing struts to nest compactly within 20GP and 40HQ containers, packing up to 26 metric tons per container while safeguarding surface powder coatings with anti-abrasive vapor-barrier wrapping.
As supply chains navigate omnichannel fulfillment, warehouse land scarcity, and industrial robotics integration, warehouse storage architecture is experiencing a generational paradigm shift.
Procurement executives are shifting from lowest-bidder mentality to lifecycle TCO models. High-tensile steel (Q355B vs standard mill scrap) reduces overall steel weight by up to 18% while offering greater yield protection against forklift mast impacts. Standardizing on modular beam connections ensures reconfigurability when inventory SKU profiles change, eliminating costly rack replacements.
With commercial real estate leasing rates rising across major global logistics corridors, enterprise operators are doubling or tripling existing floor footprints through rack-supported and structural steel mezzanines. Multi-tier attic systems permit high-density manual picking decks on levels two and three while preserving floor-level heavy pallet staging.
Tier-1 logistics providers and EPC warehouse contractors are bypassing local middlemen to partner directly with scalable OEM manufacturers capable of producing 30,000+ tons monthly. This direct link eliminates dealer markups, gives immediate access to structural engineering teams, and guarantees consistent steel mill certifications.
Traditional static selective racking is increasingly complemented by semi-automated radio shuttle carts and automated storage and retrieval systems (AS/RS). These systems utilize heavy-duty galvanized running tracks integrated directly into roll-formed beam profiles, handling both FIFO and LIFO lanes with lane depths extending 40+ pallets deep without forklift lane entry.
Modern structural codes (including Eurocode 8, ASCE 7, and RMI MH16.1) mandate sophisticated dynamic seismic analysis. Modern OEM rack uprights now incorporate cold-formed stiffening ribs and ductile baseplate anchor designs engineered to absorb horizontal ground accelerations through controlled elastic deformation rather than brittle joint failure.
Rapid global growth in fresh produce, meat, and pharmaceutical cold logistics requires specialized racking capable of operating continuously in temperatures down to -35°C. Our low-temperature formulated steels eliminate cold embrittlement risks, combined with high-durability zinc phosphating and hot-dip galvanized finishes that resist constant freeze-thaw condensation cycles.
Detailed engineering, manufacturing, and international trade answers for warehouse project directors, procurement managers, and logistics consultants.
We manufacture our load-bearing upright columns, pallet beams, and structural platform channels using certified prime Q235B and Q355B hot-rolled carbon steel coils sourced directly from top-tier state mills. In metallurgical composition and mechanical properties:
• Q235B offers a minimum yield strength of 235 MPa and tensile strength of 375–500 MPa, equivalent to European EN 10025 S235JR and American ASTM A36 / A1011 SS Grade 36.
• Q355B provides a minimum yield strength of 355 MPa and tensile strength of 470–630 MPa, equivalent to European EN 10025 S355JR and American ASTM A572 Grade 50.
Every raw material master coil is accompanied by original Mill Test Certificates (MTC) detailing yield, tensile strength, elongation percentage, and chemical spectrometry (C, Si, Mn, P, S).
To ensure our structural engineering team delivers an optimal, code-compliant storage layout within 24 hours, please share:
1. Architectural DWG or PDF floor plan: Indicating clear building height beneath ceiling obstructions/sprinklers, building column centerlines, dock door locations, and fire exit corridors.
2. Pallet & Unit Load Specifications: Pallet dimensions (Width × Depth × Height including cargo) and maximum gross weight per pallet position.
3. Material Handling Equipment (MHE): Forklift make and model, minimum aisle turning clearance requirements (AST), and maximum mast lift reach height.
4. Environmental Conditions: Operating temperatures (ambient, air-conditioned, or cold room), concrete slab thickness/compressive strength, and seismic zone location.
Corrosion resistance is built into our automated multi-stage pre-treatment and finishing line. Steel components do not simply receive paint over bare metal; they pass through high-temperature alkaline degreasing, twin industrial acid pickling baths to strip scale, and an immersion zinc-phosphating conversion tank that creates a microscopic, highly adhesive crystalline coating.
Next, electrostatic spray guns apply high-grade thermosetting epoxy-polyester powder at 80 to 120 microns thickness, cured inside a 200°C baking tunnel. This coating passes 500-hour salt spray tests (ASTM B117) and 2H pencil hardness scratch resistance. For extreme conditions (freezer rooms below -25°C, coastal fertilizer distribution, or outdoor yards), we supply components with continuous hot-dip galvanizing (HDG) per ISO 1461, yielding 65–85μm pure zinc barrier protection.
Yes. As an OEM manufacturer, modular compatibility is a cornerstone of our system design. Our pallet racking beams are manufactured with standard 50mm and 75mm connector steps designed to seat flush with:
• Wire Mesh Decking: Waterfall-lipped 50×50mm or 50×100mm mesh with inverted bottom support channels for overhead sprinkler water penetration.
• Safety Protection Accessories: Heavy structural column wrap guards, steel end-of-row barrier bollards, backstop safety mesh panels, and guide rail systems for Very Narrow Aisle (VNA) turret trucks.
• Automated Logistics Hardware: Mounting brackets for barcode guide markers, optical sensors, automated radio shuttle runner rails, and pallet flow gravity roller tracks.
Every international order ships with a comprehensive export documentation package and modular knock-down packing plan. Racking components are individually tagged with waterproof barcodes keyed to the master warehouse assembly drawing. Upright frames are either pre-bolted or knock-down bundled to maximize ocean container cubic capacity.
We provide step-by-step 3D exploded isometric installation manuals, high-definition installation video tutorials, and live video engineering consultations. For large-scale projects exceeding 1,000 pallet positions or multi-tier mezzanine platforms, we can dispatch bilingual on-site site installation supervisors to manage and certify local assembly teams.
With our 30,000 m² production facility and 30,000-ton monthly capacity, our standard manufacturing lead time for full 40HQ container loads is 15 to 20 working days from drawing sign-off and deposit receipt. Expedited manufacturing is available for urgent facility expansions.
Our flexible MOQ starts at one 20GP container (or approximately 10–12 tons of fabricated steel). We support diverse international incoterms including FOB, CFR, CIF, DDU, and DDP, working through major global shipping lines out of Guangzhou, Shenzhen, and Hong Kong ports.