What are the key engineering criteria that separate standard pallet racks from "extra heavy duty" systems?
+
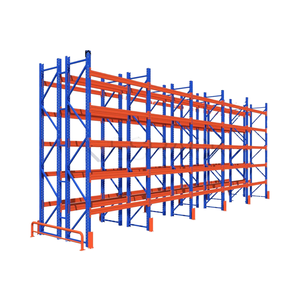
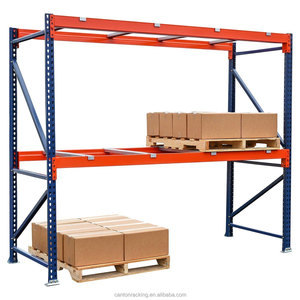
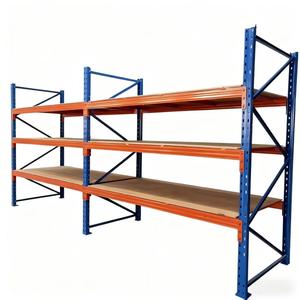
Standard light-to-medium pallet racks typically utilize cold-rolled steel profiles with wall thicknesses ranging between 1.5 mm and 1.8 mm, designed to accommodate uniformly distributed loads (UDL) up to 1,500 kg per beam level. In contrast, Extra Heavy Duty Pallet Racks from HEDA are engineered from heavy cold-rolled structural steel (Q235B or Q355B) featuring column cross-sections from 90×70 mm up to 140×100 mm with steel thicknesses between 2.0 mm and 3.25 mm. Additionally, beam connections integrate oversized 4-claw or 5-claw high-moment end connectors with 10mm shear-resistant steel locking pins. These specifications allow our systems to securely sustain continuous working loads of 3,000 kg to over 5,000 kg per level and cumulative upright bay capacities exceeding 28,000 kg under severe dynamic operating conditions.
How do your engineers calculate beam deflection limits under heavy static and dynamic loads?
+
Beam deflection calculations are executed in strict compliance with European standard EN 15512 and RMI MH16.1 specifications. Under full rated design load, the vertical deflection of any load-carrying beam must not exceed $L/200$ (where $L$ is the clear span distance between upright columns). For sensitive automated picking or fragile materials, HEDA engineers can stiffen the profiles to achieve $L/250$ or $L/300$. Box beams are fabricated by interlocking and continuously welding twin C-sections via robotic submerged-arc seam welders, creating a closed-box profile that offers exceptional torsional rigidity, resisting horizontal twisting forces when forklifts place or retrieve heavy pallets.
How does HEDA handle seismic zone engineering for seismic-active export regions?
+
When exporting to seismic-prone regions (such as the Pacific Rim, parts of Latin America, the Mediterranean, or the East African Rift), our structural engineering department utilizes 3D finite element analysis (FEA) software. We calculate dynamic base shear, lateral drift, and overturning moments per local codes (Eurocode 8, UBC Zone 4, or ASCE 7). To absorb ground acceleration energy without catastrophic collapse, we incorporate heavy-duty seismic baseplates (ranging up to 16 mm thick), high-tensile anchor bolts (Grade 8.8 / Grade 10.9), and multi-tier diagonal cross-bracing along the spine and rear bays of the racking system.
What surface treatment is best suited for humid coastal warehouses and sub-zero cold storage?
+
For standard indoor ambient facilities, our standard 10-stage process includes thorough degreasing, acid pickling, zinc phosphating, and automatic electrostatic application of an exterior-grade thermosetting polyester powder coating (cured at 180°C–200°C for 20 minutes, 75–95µm thickness). For coastal warehouses with high relative humidity, maritime salt-air exposure, or sub-zero refrigeration (-35°C), we recommend Hot-Dip Galvanizing (HDG) per ISO 1461. Hot-dip galvanization immerses cleaned structural steel components directly into a molten zinc bath at 450°C, producing a metallurgically bonded zinc-iron alloy layer that provides decades of cathodic rust protection.
What is the standard lead time and container packing efficiency for bulk OEM/ODM export contracts?
+
Standard production lead time for full container loads (FCL) is typically 15 to 25 business days from CAD layout sign-off and deposit receipt. Our dedicated logistics team develops specialized 3D packing manifests for every order. Upright frames are either knock-down nested with steel strapping or pre-assembled in staggered blocks with foam edge guards and moisture-barrier film. Beams are bundled in matched pairs with wooden dunnage blocks to facilitate seamless forklift de-vanning at destination ports. A typical 40HQ maritime container accommodates between 22 and 26 metric tons of pallet racking, maximizing space utilization and minimizing ocean freight expense per pallet position.
Can HEDA provide complete custom OEM/ODM hole punching, custom RAL colors, and client branding?
+
Yes. As a factory direct OEM/ODM manufacturer, we can roll and punch columns according to custom hole pitches (e.g., 50mm metric, 75mm European, or 76.2mm / 3-inch teardrop imperial pitches). We can match corporate RAL colors precisely using high-durability electrostatic powders and integrate client brand logos onto load notice plates, column protectors, and frame caps. Comprehensive technical dossiers including CAD installation blueprints, component weight schedules, and load rating certificates are supplied with every shipment to support client branding and local municipal permitting.