High-Density Dynamic Storage & Heavy-Duty Racking Systems
Our OEM/ODM factory manufactures a comprehensive spectrum of mobile and static load-bearing systems engineered from structural Q235B cold-rolled steel. Explore our flagship models engineered to maximize volumetric storage capacity by up to 85%.
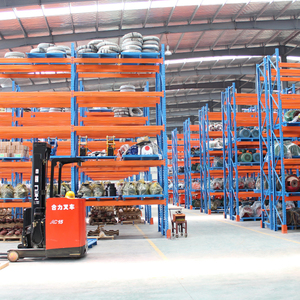
Best Selling Customized Warehouse Drive in Rack Steel Pallet Racking System
- Load: Up to 1500kg / Pallet
- Eliminates operating aisles
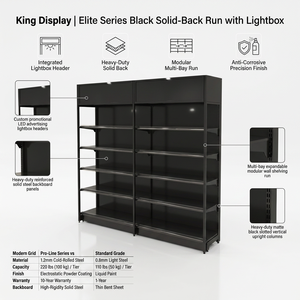
Versatile All Business Formats Cold-rolled Steel Double-sided Wire Shelving
- Rust-resistant zinc / powder finish
- Adjustable modular tier heights
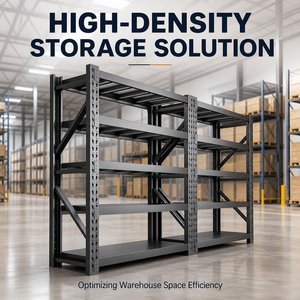
Industrial Medium Duty Longspan Shelving Starter & Add-on Units
- Capacity: 200–800kg / Level
- Interlocking pin safety design
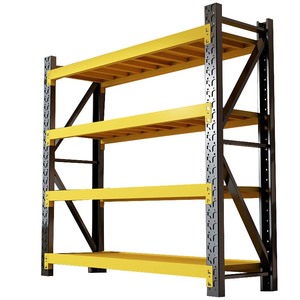
Yunbang 100–400Kg/Layer Rust-Proof Garage Metal Storage Racks
- Multi-layer corrosion resistance
- Tool-less rapid assembly
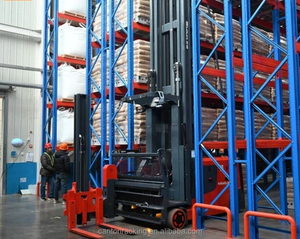
Very Narrow Aisle (VNA) High-Density Storage Racking System
- Vertical clearance to 15 meters
- 100% individual pallet access
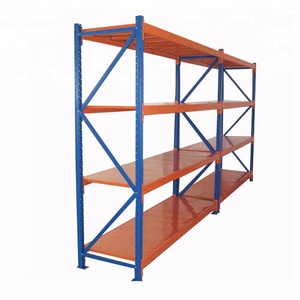
Customized 4/5 Layer Boltless Medium Duty Shelving Rack
- 300kg uniform distributed load
- Precision CNC slotted uprights
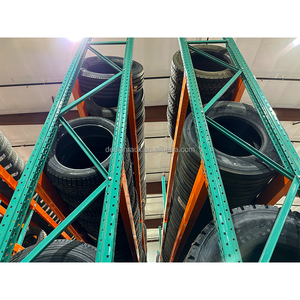
Beam Pallet Rack Q235B Steel Heavy Duty Warehouse Rack
- Up to 4500kg per beam tier
- EN 15512 structural conformity
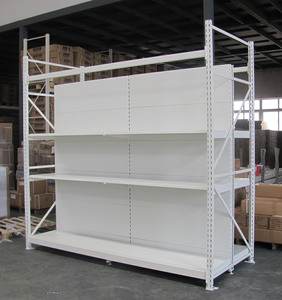
Integrated Hypermarket Display Shelving & Storage System
- Dual functional retail + storage
- Custom RAL powder finishes
Strategic Procurement Trends Shaping Mobile Shelving & High-Density Storage
As global supply chain operators encounter escalating real estate lease rates and energy costs, procurement strategies for mobile storage infrastructure have transitioned from basic static shelving to intelligent, motorized, and space-condensing movable architectures.
1. Footprint Elimination & Cube Utilization
Traditional static racking requires dedicated access aisles between every storage row, forfeiting approximately 55% to 65% of warehouse floor footprint to passive transit space. Contemporary procurement prioritizes track-mounted mobile shelving bases that condense multiple blocks into a single mobile cluster, achieving upwards of 85% usable volumetric density.
By moving rows along floor-embedded or surface-mounted precision guidance tracks, facilities effectively double their inventory capacity within the existing building envelope without capital expenditure on real estate expansions.
2. Cold-Chain Energy Conservation Matrix
Cold storage facilities incur heavy electrical overheads directly correlated to the refrigerated cubic volume. With electricity expenses comprising over 30% of cold warehouse operational expenditure, high-density powered mobile racking systems have emerged as an international procurement benchmark across Europe, North America, and emerging African distribution nodes.
Compacting pallet positions within chilled chambers drastically curbs thermal dispersion per pallet location, reducing refrigeration power demand by up to 40% while sustaining rapid FIFO or LIFO batch access.
3. PLC Automation & Safety Sensor Triangulation
Modern mobile racking configurations have migrated from mechanical hand-crank operations to PLC-controlled motorized chassis integrated with warehouse management systems (WMS). Intelligent procurement mandates advanced safety redundancy: photoelectric optical barriers, proximity sensors, emergency trip bars, and floor-level light curtains.
These fail-safe systems safeguard operators and reach-truck drivers by executing instantaneous millisecond braking whenever an obstruction, human presence, or displaced product enters an operating aisle during mobilization.
Technical Evolution: Mechanical vs. Electric Mobile Shelving Systems
Understanding structural differences, floor rail load transfers, and wheel flange mechanics is critical when selecting an OEM/ODM partner capable of tailoring installations to dynamic building parameters.
| Technical Parameter | Mechanically Assisted Mobile Shelving | Electric Powered Mobile Heavy Racking | Autonomous Mobile Shuttle Racking |
|---|---|---|---|
| Primary Target Applications | Archives, spare parts, pharmaceutical boxes, bins | Heavy pallet logistics, cold chain, bulk FMCG | Deep-lane high-throughput dynamic distribution |
| Drive Mechanism | Ergonomic gear crank with reduction chains | Electric gear-motor (0.75kW–1.5kW per bogie) | Low-voltage DC carrier shuttle with Li-ion pack |
| Load Rating Per Bay/Level | 300kg – 800kg uniformly distributed | 5,000kg – 30,000kg per mobile carriage block | 1,500kg per pallet dynamic transit capacity |
| Floor Track Interface | Surface-mounted ramp tracks or low-profile zinc rails | Sub-floor recessed steel rails with grout levelling | Static rack guidance rails with optical positioning |
| Aisle Opening Velocity | Manual cadence (~0.1 – 0.2 m/sec) | Automated sync drive (~0.15 – 0.25 m/sec) | High-speed lane traversal (up to 1.2 m/sec) |
| Control Architecture | Mechanical anti-tilt mechanical pin lock | Central PLC panel, RFID, radio remote & safety curtain | WCS/WMS bidirectional Wi-Fi radio integration |
Enterprise Advantages: Full OEM/ODM Process Control from Coil to Container
Established in 2001, Guangzhou Heda Shelves Co., Ltd. oversees end-to-end precision manufacturing of warehouse storage and mobile shelving systems. Our 30,000 m² industrial production complex integrates proprietary roll-forming, automated robotic welding, and specialized multi-stage surface treatments.
Metallurgical Superiority: Q235B Cold-Rolled Steel
We source certified prime Q235B high-tensile cold-rolled steel coils with guaranteed structural yield strengths exceeding 235 MPa. Every production batch undergoes elongation, tensile rupture, and metallurgical chemical analysis to verify compliance with FEM 10.2.02 and EN 15512 international rack design codes.
Surface Pretreatment: Pickling & Phosphating
Unlike secondary fabricators utilizing rudimentary manual solvent cleaning, our automated finishing line routes all steel members through an 8-stage industrial acid pickling, ultrasonic degreasing, and zinc phosphating wash tunnel. This molecular bonding stage precludes subsurface rust creep under humid tropical or maritime conditions.
International Verification: CE & ISO 9001:2015
Guangzhou Heda Shelves Co., Ltd. holds documented CE Certification (Registration No. 2435-CPR-8605159), ISO 9001:2015 Quality Management Accreditation (Registration No. 18624Q00169R0M, valid to June 2027), and verified RoHS hazardous substance compliance, guaranteeing frictionless import clearance for EPC contractors and corporate procurers.
10-Stage Precision Manufacturing Pipeline
Every mobile carriage, upright profile, and load beam passes through our rigorous in-house fabrication protocol to guarantee 0.1mm dimensional tolerance.

Certified Raw Materials

Precision Steel Cutting

Automated Punching

Cold Bending Forming

Profile Roll Forming

Mechanical Polishing

Robotic Seam Welding

Pickling & Phosphating

Powder Coating Line

QC & Ocean Bundling
Frequently Asked Questions: Engineering, Sizing & Global Shipping
Consult expert architectural and logistical answers compiled by HEDA Shelves' lead structural application engineers to de-risk your mobile racking procurement project.
What structural building specifications are required before installing floor-embedded mobile shelving tracks? +
Mobile shelving systems concentrate substantial dead and live point loads across rolling wheel contacts. The warehouse concrete floor slab must deliver a minimal compressive rating of C25/C30 (compressive strength 25–30 MPa) with a floor flatness tolerance complying with DIN 18202 (or ASTM E1155 FF/FL standards).
For existing floors where trenching for recessed rails is unacceptable, we fabricate low-profile surface-anchored guide rails accompanied by beveled aluminum transition ramps to guarantee unimpeded hand-pallet truck transit.
How does HEDA Shelves protect mobile racking components from maritime corrosion and tropical humidity? +
Components undergo an automated chemical immersion line: multi-tank acid pickling to eliminate mill scale, followed by iron-zinc phosphating which etches a crystalline microscopic protective film onto the bare steel. We then apply thermosetting TGIC-free epoxy-polyester powder electrostatically at 180°C–200°C curing temperatures.
This process achieves a consistent 60–90 micron dry film thickness (DFT) surpassing 500 hours of standard ASTM B117 neutral salt spray resistance. For sub-zero cold rooms or coastal ports (such as Lagos, Mombasa, or Durban), we offer hot-dip galvanization according to ISO 1461 standards.
Can your electric mobile racking systems operate safely during regional electric grid outages? +
Yes. Our motorized mobile bases feature a dual-redundancy architectural design. In standard conditions, three-phase geared electric motors traverse carriages via electronic pushbutton, remote radio controller, or integrated WMS dispatch. During power brownouts or blackouts, an integrated mechanical override clutch allows operators to effortlessly hand-crank the mobile units with an ergonomic drive crank.
Additionally, our radio shuttle carts run on independent fast-charging industrial lithium-ion batteries that operate continuously for 8–10 hours per cycle and can be recharged via onsite solar arrays or auxiliary backup generators.
What design documentation and calculations are provided prior to PO sign-off? +
Every customized OEM/ODM project begins with a complimentary engineering package provided within 24 to 48 hours. Our engineering department uses AutoCAD and 3D SolidWorks to deliver comprehensive 2D floor layout schematics, 3D photorealistic renderings, structural point-load distribution diagrams, and FEM 10.2.02 deflection verification.
This documentation ensures civil engineers, local fire marshals, and warehouse operations managers can audit aisle widths, egress pathways, and fire sprinkler clearance before manufacturing begins.
How are oversized upright frames and mobile chassis packaged for ocean container transport? +
To avoid dead container freight costs, all mobile shelving bases, upright trusses, and horizontal step beams utilize knock-down modular designs. Upright trusses are bundled using automated plastic-strapping machines with corrugated board edge-protectors and heavy-duty steel lifting dunnage.
Drive motors, wheel bogies, electrical control cabinets, and hardware fasteners are crated in sea-worthy fumigated plywood cases with moisture-desiccant packs, engineered to maximize cubic volume inside standard 20GP or 40HQ ocean freight shipping containers.
What installation support is available for international projects? +
Each shipment includes laser-etched component tags corresponding directly to color-coded installation layout drawings and comprehensive assembly manuals. HEDA Shelves provides real-time video engineering supervision across global time zones.
For large-scale distribution centers and multi-tier mezzanine mobile platforms, our senior bilingual installation superintendents can be dispatched directly onsite to manage local installation crews, verify laser track leveling, test safety sensor limits, and train client maintenance personnel.