Factory-Direct Pallet Rack Frames & Heavy-Duty Systems
Precision-punched uprights, box-welded step beams, and modular decking engineered for automated intralogistics, cold hubs, and high-density distribution centers worldwide.
Engineering Whitepaper: Pallet Rack Frame Metallurgy, Structural Mechanics, and Sourcing Architecture
Pallet rack upright frames represent the primary structural backbone of modern logistics, intralogistics automation, and supply chain hubs worldwide. Far beyond simple bent-sheet fabrications, a modern heavy-duty pallet rack frame is a calculated structural column subject to intricate multidirectional physics: axial compression from pallet deadloads, dynamic impact vectors from reach trucks and counterbalance forklifts, cyclic seismic ground accelerations, windage loads in external rack-clad configurations, and torsional shear induced by irregular multi-bay load distributions.
When engineering and sourcing pallet rack frames, industrial warehouse project directors and EPC contractors must evaluate certified structural safety, metallurgical pedigree, cold roll-forming tolerances, and surface chemistry passivation. Selecting an inadequately engineered upright profile or an uncertified supplier introduces severe risks of progressive structural collapse, warehouse shutdown, insurance voidance, and catastrophic material loss.
1. Anatomical Dissection of Heavy-Duty Pallet Rack Upright Profiles
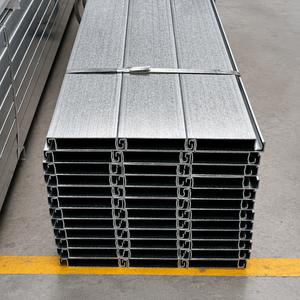
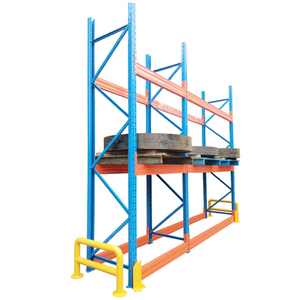
A reliable pallet rack frame consists of two cold-rolled omega-profile (or multi-bend box-profile) upright columns rigidly triangulated by horizontal and diagonal bracing members through Grade 8.8 structural bolting or high-tensile factory automated welding. The upright cross-section determines the overall radius of gyration (r) and the slenderness ratio (λ = kL/r), which govern elastic and inelastic buckling thresholds according to ANSI MH16.1, EN 15512, and AS 4084 standards.
Continuous Profile Roll-Forming
Continuous roll forming over 18 to 22 precision-calibrated tooling passes gradually induces yield stress without micro-fracturing cold-rolled steel crystal boundaries, maximizing yield point strength.
Cold-Punch Hole Geometry
Automated punch presses deliver precision-indexed teardrop, hexagonal, or diamond perforations at 50mm, 75mm, or 76.2mm intervals, calibrated to maintain minimal section loss while guaranteeing snug beam connector engagement.
Triangulated Bracing Geometries
Alternating horizontal and diagonal C-shaped bracing channels form high-rigidity truss systems that transfer horizontal shearing loads, dampening harmonic vibrations from heavy MHE truck operations.
Baseplate & Anchor Interface
Heavy-duty laser-cut baseplates distribute ground-pressure loads evenly onto warehouse concrete slabs, securing seismic shear pins and heavy wedge anchor bolts against pull-out stresses.
2. Metallurgical Selection: Q235B vs. Q355B Hot-Rolled Coils
Steel chemistry is paramount. Standard light-duty commercial shelving often utilizes uncertified scrap-recycled metal, which exhibits unpredictable brittleness and erratic tensile curves under cyclic industrial loading. Guangzhou Heda Shelves Co., Ltd. sources exclusively primary hot-rolled carbon steel coils tested under strict spectrographic chemical analysis:
- Q235B Carbon Steel: Yield strength ≥ 235 MPa, Tensile strength 370–500 MPa, Elongation ≥ 26%. Exceptional ductility and cold-forming behavior, ideal for ambient selective racking, drive-in systems, and light-to-medium mezzanine tier structures.
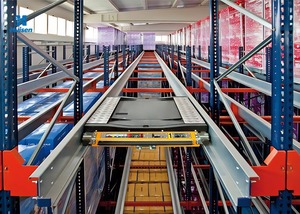
- Q355B High-Strength Low-Alloy (HSLA) Steel: Yield strength ≥ 355 MPa, Tensile strength 470–630 MPa, Elongation ≥ 21%. Formulated with trace micro-alloying elements (Vanadium, Niobium, Titanium), Q355B allows reduced frame deadweight while substantially boosting column vertical load capacities for automated high-bay shuttle systems (ASRS) up to 30+ meters high.
| Racking Architecture | Upright Profile (mm) | Thickness Range | Typical Max Bay Load | Primary Sector Application |
|---|---|---|---|---|
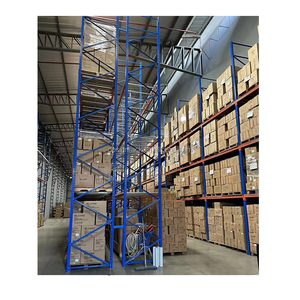
| Selective Pallet Racking | 80x60, 90x70, 100x70 | 1.8mm – 2.5mm | 8,000 – 16,000 kg | FMCG, 3PL Distribution, General Importers |
| Heavy Drive-In / Drive-Through | 90x70, 100x70, 120x95 | 2.0mm – 3.0mm | 12,000 – 22,000 kg | Cold Storage, Beverage Hubs, Bulk Sugar/Flour |
| Automated Radio Shuttle / ASRS | 100x70, 120x95, 140x95 | 2.5mm – 3.5mm | 18,000 – 32,000 kg | Buffer Hubs, High-Volume E-Commerce, Pharma |
| Multi-Tier Rack Mezzanine | 90x70, 100x70, 120x95 | 2.0mm – 3.0mm | Deck load: 300–1000 kg/m² | Auto Spare Parts, Fashion Garment Picking |
| Heavy Cantilever Towers | 200x100 to 400x150 H-Beam | Welded Structural Steel | Up to 3,000 kg/Arm | Steel Pipes, Rebar, Timber, Sheet Board |
Emerging Procurement Trends in Pallet Rack Frame Sourcing (2025–2030)
As global supply networks face rising real-estate leasing costs, port bottlenecks, and volatile containerized ocean freight rates, international B2B procurement leaders are overhauling how they select rack manufacturing partners. Sourcing models have shifted decisively from localized spot trading to direct factory integration based on four core criteria:
Container-Cubing Geometry
With ocean shipping rates demanding strict cost management, modern frame designs must optimize nesting profiles. Modular knock-down upright frames packed in precision bundles allow maximum metric tonnage per 40ft HQ container without wasting cube volume, significantly cutting landed cost per pallet location.
Mechanical Density Solutions
In developing regions and erratic grid environments (such as West and East Africa, South America, and Southeast Asia), operators are deliberately prioritizing mechanical gravity-flow and semi-automatic battery-backed shuttle systems that run independently during severe electrical brownouts.
Tight Tolerance Tooling
Warehouses transitioning toward Autonomous Mobile Robots (AMRs) and automated shuttle carriers require upright deflections under full rated loads not to exceed 1/1000 of clear bay spans, demanding strict factory roll-forming repeatability.
Technological & Manufacturing Advancements in Rack Frame Production
The manufacturing gap between certified high-tier rack factories and uncertified workshops lies in the surface-finishing chemistry and automated mechanical processing lines. A standard spray-paint system applied over oily, unwashed steel will experience interfacial moisture seepage, peeling, and severe blistering within 12 to 18 months, especially in humid coastal ports or cold-storage environments.
At Guangzhou Heda Shelves Co., Ltd., pallet rack frame manufacturing is governed by an exhaustive 10-step precision workflow that guarantees corrosion protection for over a decade:










Crucially, Stage 08: Pickling and Phosphating removes microscopic mill scale, carbon residue, and atmospheric oxidation through a multi-stage chemical wash, creating an insoluble micro-crystalline zinc-phosphate conversion layer. This provides superior adhesion for the subsequent Stage 09: Electrostatic Epoxy-Polyester Powder Coating, cured at 180°C–200°C to achieve a tough, impact-resistant finish with an 80–120μm dry film thickness. For extreme environments, such as deep-freeze logistics (-30°C) or outdoor builders' yards, hot-dip galvanizing per ISO 1461 guarantees complete cathodic protection.
Factory Verification, Quality Credentials, and Engineering Governance
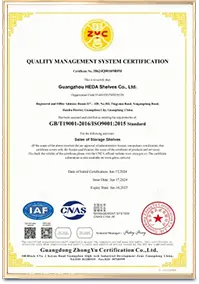
When selecting a pallet rack manufacturer, documented compliance is non-negotiable. HEDA Shelves holds third-party audited credentials confirming rigorous process management, mechanical load testing, and eco-friendly manufacturing:
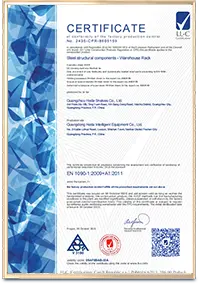 CE Certificate (EN 1090)
No. 2435-CPR-8605159
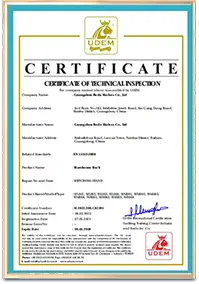 ISO 9001:2015 Quality
Reg. 18624Q00169R0M
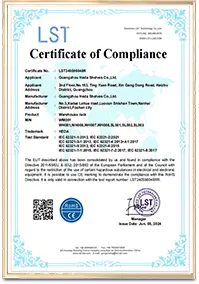 RoHS Compliance
Heavy Metal Free Coating
 FEM / RMI Compliance
Structural Test Verified
Every batch of upright columns and welded beam connectors undergoes rigorous dimensional verification, ultrasonic weld-depth testing, and destructive deflection testing in our dedicated QA testing bay before container dispatch.
Technical FAQ
Comprehensive engineering, shipping, and architectural answers compiled directly by HEDA Shelves Senior Structural Engineers.
Inquire NowWhat critical data is required to calculate frame upright profiles?
How do knock-down upright frames reduce international ocean freight costs?
What prevents upright frames from twisting or failing during minor forklift impacts?
Can HEDA pallet rack frames be integrated into existing third-party racks?
What surface treatment is recommended for sub-zero cold room environments?
How does HEDA assist with remote installation for international projects?
Ready to Engineer Your Warehouse Storage Infrastructure?
Connect directly with HEDA Shelves structural design engineers. Receive comprehensive CAD floor plans, 3D architectural renderings, structural load calculations, and container-optimized export quotations within 24 hours.