Engineered Heavy-Duty Racking & Dynamic Storage Solutions
Examine our certified warehouse systems engineered for high-density pallet rotation, heavy load resilience, and optimized unit handling across industrial global operations.
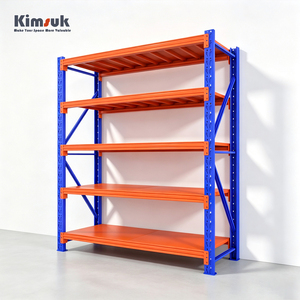 Medium Duty
- • Quick teardown boltless interlocking
- • 200–500 kg per shelf layer capacity
- • Epoxy electrostatic powder finish
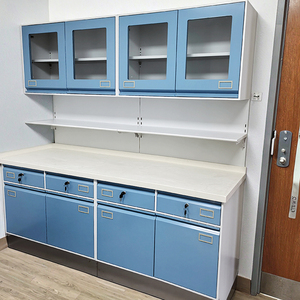 Modular Steel
- • Medical-grade cold-rolled plate
- • Anti-microbial sterile chemical coat
- • Ergonomic wall mounting integration
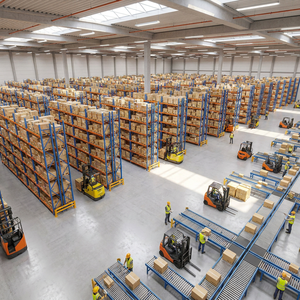 High Density
- • Maximize vertical space up to 15m
- • Guided aisle rail / wire inductive track
- • 100% individual pallet selectivity
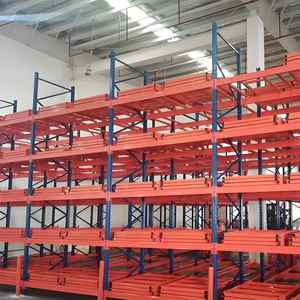 Dynamic LIFO
- • 2 to 6 pallet deep nested cart tracks
- • Gravity slope feed eliminates aisles
- • Heavy gauge Q235B structural roll
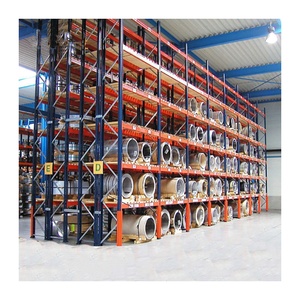 Heavy Duty
- • Up to 4,500 kg per beam level capacity
- • 75mm/50mm pitch adjustable uprights
- • Certified high-load structural steel
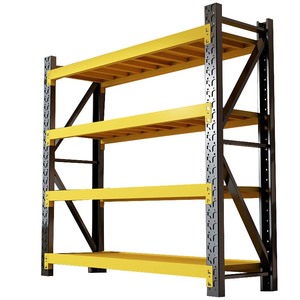 Rust-Proof
- • Corrosion-resistant zinc treatment
- • Modular stackable shelf architecture
- • Commercial garage & retail staging
 Retail & Archive
- • Precision punched single-slot upright
- • High-tensile wall-anchoring bracket
- • Flexible display & small-parts pick
 Collapsible Post
- • 4-way forklift entry with stack cups
- • Fold-down posts for reverse freight save
- • Heavy commercial truck tyre handling
The Mechanics of Gravity Roller Racking & Pallet Flow Systems
An engineering treatise on kinetic equilibrium, speed control damping, and dynamic load dissipation in automated and semi-automated gravity pallet tracks.
Roller racking—predominantly deployed as gravity pallet flow or carton live storage—represents the pinnacle of energy-neutral, high-density warehousing. Unlike static selective pallet systems that demand dedicated access aisles for every rack row, a roller racking system functions on a continuous declined plane, typically angled between 3.0% and 4.0% (1.7° to 2.3°). Utilizing earth's gravity, pallets loaded at the upper charging side glide steadily down precision-formed roller tracks toward the picking face, achieving seamless First-In, First-Out (FIFO) dynamic buffer storage.
The gravitational driving force component along the incline is expressed as Fg = m × g × sin(θ), where m is pallet mass, g is gravitational acceleration, and θ represents the lane angle. To eliminate runaway acceleration and prevent catastrophic impact collisions at the discharge terminal, mechanical centrifugal braking rollers must be positioned at calculated intervals along the track. These autonomous braking rollers generate proportional opposing hydraulic or centrifugal friction, clamping terminal velocity within the safe operating window of 0.15 m/s to 0.30 m/s.
Critical Componentry in High-Load Roller Bed Fabrication
Top-tier roller racking manufacturers distinguish themselves through metallurgical grade discipline and mechanical tolerances. Standard pallet flow beds engineered by Guangzhou Heda Shelves Co., Ltd. integrate the following critical sub-assemblies:
1. Heavy-Wall Cold-Drawn Steel Rollers: Rollers are fabricated from precision micro-alloyed carbon steel tubes (Ø50mm to Ø76mm, wall thicknesses from 1.5mm to 3.2mm) fitted with dual-labyrinth sealed, deep-groove precision ball bearings (6002-2RS or 6204-2RS). This protects the internal ball races from concrete dust contamination, fine particulates, and ambient moisture, guaranteeing rotational friction coefficients as low as μ ≤ 0.015.
2. Centrifugal & Magnetic Brake Rollers: In deep-lane pallet flow (depths extending from 5 to over 25 pallets deep), uncontrolled velocity escalates structural risks. HEDA's speed-controller rollers feature internal multi-stage gear sets and planetary centrifugal clutches. When a traversing pallet exceeds 0.25 m/s, the centrifugal brake shoes expand against the internal drum wall, transforming kinetic energy into thermal dissipation without relying on external pneumatic or electrical lines.
3. Heavy-Duty Pallet Separators: At the retrieval face, extracting the first pallet while multiple subsequent pallets exert continuous line-pressure can cause lift-truck fork bind, mast strain, or unstable load tip. Robust mechanical load separators hold back the entire queue of accumulated pallets behind the front position by 300mm to 450mm. The separator automatically disengages only after the forklift operator successfully lifts and clears the lead pallet from the discharge nest.
| Dynamic Storage Configuration | Standard Slope Angle | Throughput Characteristic | Pallet Weight Spectrum | Energy Consumption | Floor Footprint Efficiency |
|---|---|---|---|---|---|
| Full-Width Gravity Pallet Flow | 3.2% – 3.8% (1.8°–2.2°) | Continuous FIFO Stock Rotation | 400 kg – 1,500 kg / pallet | 0.0 kW (Pure Gravity) | Up to +65% vs. Selective Racks |
| Push-Back Nested Roller Cart | 2.0% – 2.5% (1.1°–1.4°) | Deep-Lane LIFO Batch Buffer | 500 kg – 1,400 kg / pallet | 0.0 kW (Forklift Pushed) | Up to +45% vs. Conventional |
| Radio Shuttle + Roller Bed | 0.0% (Level Guided Track) | Flexible Hybrid FIFO/LIFO | 300 kg – 2,000 kg / pallet | < 0.05 kWh/cycle (Battery) | Up to +80% Volume Utilization |
| Light/Medium Carton Flow | 4.5% – 6.0% (2.6°–3.4°) | High-Speed Piece/Tote Pick | 5 kg – 50 kg / tote | 0.0 kW (Gravity Feed) | Saves 50% Travel Picking Time |
Future Procurement & Technological Trends in Roller Racking
Critical strategic shifts driving capital expenditure allocations, environmental mandates, and structural material advancements in modern industrial storage facilities.
Zero-Carbon Operational Mandates
With soaring grid electricity tariffs and corporate Scope 1/2 ESG decarbonization audits, global warehouse operators are pivoting aggressively from motorized conveying systems toward passive gravity roller mechanisms. Gravity pallet flow delivers up to 120 pallet operations per hour with absolute zero continuous power consumption, making it the premier choice for sustainable logistics hubs.
Cold-Chain Thermal Optimization
Refrigerated warehouse cubic space commands a 400% to 600% energy premium over ambient facilities. Modern procurement specifications demand ultra-dense, multi-tier pallet flow racks within cold vaults down to -30°C. By shrinking aisle requirements and consolidating refrigerated air mass, dynamic roller systems slash cold-loss thermal cycling and compress facility footprint by over 50%.
Duplex Anti-Corrosion Metallurgy
High ambient humidity in coastal distribution zones (such as West Africa, Southeast Asia, and the Middle East) rapidly degrades lower-grade mild steel. Top factories have discarded rudimentary single-coat paint in favor of 10-stage automated hot-dip chemical pickling, micro-crystalline zinc phosphating, and 120-micron thermosetting electrostatic polyester powder shielding rated past 1,000 salt-spray hours.
AMR / AGV Dynamic Dock Interfaces
The rapid integration of Autonomous Mobile Robots and automated reach trucks requires sub-millimeter positional repeatability at rack interfaces. Advanced roller racking now features optical entry guides, inductive deceleration beds, and robotic centering stops that allow autonomous pallet trucks to interface without human intervention or physical bumper damage.
Total Landed Cost Containerization
Skyrocketing ocean freight rates require intelligent factory packaging. Leading manufacturers utilize algorithmic nest packing, knockdown boltless upright frames, and modular drop-in roller rail segments. This strategy maximizes standard 40-foot High Cube (40HQ) container utilization up to 98% volume density, reducing the landed freight cost per pallet position by 28% to 35%.
Predictive Kinematic Load Simulation
Top engineering teams no longer rely on static rule-of-thumb slope calculations. Advanced 3D finite-element software (ANSYS / SolidWorks Simulation) models bottom-board pallet deflection, dynamic wheel track indentation, and wood-to-steel friction matrices under cyclic loading. This eliminates field commissioning failures before the first container leaves the factory dock.
Direct Factory Manufacturing Advantages: Guangzhou Heda Shelves
Since its establishment in 2001, Guangzhou Heda Shelves Co., Ltd. has evolved into an international industrial storage manufacturing powerhouse. Operating from our expansive 30,000 square meter factory base in Guangzhou, China, we produce over 30,000 tons of precision-engineered racking per month, maintaining total vertical control from raw steel coil processing to international export crating.
By eliminating intermediary trading markups, international procurement teams secure direct engineering accountability, fully verified material origin certificates (Q235B and Q355B structural steel), and turnkey custom OEM/ODM solutions calibrated specifically to their warehouse structural envelopes and environmental parameters.
End-to-End Factory Execution Protocol
Every roller racking contract fulfilled by Guangzhou Heda Shelves progresses through rigorous milestone quality checks:
- Complimentary 3D CAD & Load Calculation: We simulate rack layouts, clear ceiling heights, truck turning radius, and seismic zone deflection before you commit.
- Automated Punching & Cold Bending: Upright columns are cold-rolled on multi-station CNC profiling mills for exceptional straightness and dimensional consistency.
- Surface Chemical Pretreatment: Components pass through multi-stage acid pickling, rinsing, and phosphating tanks to ensure permanent powder adhesion.
- Container Packaging Optimization: Bundling and custom steel cradling protect column flanges from transit vibration while maximizing container payload.
Supplying complex distribution hubs across Africa (Nigeria, Ghana, Kenya, South Africa, Egypt), Southeast Asia, the Middle East, Europe, and the Americas.
Frequently Asked Questions on Roller Racking Procurement
Rigorous engineering answers addressing slope calculations, braking mechanisms, pallet quality requirements, and international freight logistics.
What is the exact slope percentage required for heavy-duty pallet flow roller tracks?
For standard Euro-pallets (800x1200mm) or GMA/Industrial pallets (1000x1200mm) carrying uniformly distributed loads between 500 kg and 1,200 kg, the optimal incline is calibrated between 3.2% and 3.8% (approximately 1.8° to 2.2°). If the gradient is shallower than 3.0%, dynamic restart issues can occur if a pallet stops midway. Conversely, slopes exceeding 4.2% generate excessive velocity, overloading the centrifugal brake rollers and accelerating structural impact fatigue on beam connectors and front end stops.
How do roller racking systems handle power outages and energy instability?
Gravity roller racking systems are 100% mechanical and energy neutral. They require zero electrical power, control wiring, or pneumatic feeds to maintain continuous FIFO flow. During municipal grid failures or localized brownouts—common operational challenges in emerging supply chains—gravity roller racks remain fully functional, enabling forklifts to load and discharge goods without downtime. For cold chain warehouses, this passive operation eliminates parasitic electrical heat loads inside refrigerated chambers.
What pallet bottom-board specifications are essential for smooth roller bed performance?
Roller racking relies on uninterrupted physical contact between the pallet underside and the steel roller cylinders. Pallets must feature bottom runner boards that run parallel to the direction of flow. GMA pallets with three full-length bottom runners or 5-board perimeter base Euro pallets operate flawlessly. Warped, broken, or split runner boards, protruding nails, or non-rigid plastic pallets lacking reinforced center runners can snag or cause skewing in deep-lane systems. In mixed-pallet environments, full-width triple-track steel rollers or nested slave boards are recommended.
How is the racking protected against humidity, condensation, and corrosion in coastal areas?
At Guangzhou Heda Shelves, every structural column, beam, and bracer undergoes an automated 10-stage chemical surface conversion process prior to finishing. This begins with industrial acid pickling to eliminate mill scale and iron oxides, followed by neutral rinsing and hot zinc-phosphate immersion. The components then receive an electrostatically applied polyester powder coating cured at 180°C–200°C, producing a resilient 90–120 micron protective layer. For high-humidity coastal zones, walk-in blast freezers, or semi-outdoor dock environments, full hot-dip galvanization (HDG) per ISO 1461 can be specified to ensure decades of rust-free operation.
What engineering information is required to generate a custom 3D layout and structural calculation?
To deliver an exact CAD layout, 3D structural rendering, and structural load analysis, our engineering team requires: (1) Warehouse architectural drawings indicating clear height under roof trusses, column grids, fire sprinkler clearance, and entry dock positions; (2) Detailed pallet metrics: length, width, height, maximum gross load weight, and bottom-board layout; (3) Forklift model, maximum mast lift elevation, and minimum aisle turning radius; and (4) Daily SKU turnover volume and FIFO vs. LIFO rotation preferences. HEDA provides these engineering deliverables within 24 hours free of charge.
How are oversized racking components packed to ensure optimal ocean freight economics?
Uprights are delivered in modular, knock-down format, allowing columns and diagonal braces to bundle tightly without dead air space. Heavy horizontal load beams are nested and banded using high-tensile steel strapping with protective corner angles. Roller bed tracks are modularized into standard 2m to 3m sections that drop directly onto rack step-beams on-site. This knockdown engineering approach allows our logistics specialists to achieve up to 98% space utilization inside 20GP and 40HQ ocean containers, drastically reducing the landed shipping cost per pallet location.
What structural standards and building codes do HEDA racking systems comply with?
Our structural designs adhere to internationally recognized material handling standards, including the European RMI (Rack Manufacturers Institute) specifications, EN 15512 (Steel static storage systems – Adjustable pallet racking systems – Principles for structural design), and Australian Standard AS 4084. Guangzhou Heda Shelves Co., Ltd. holds CE Certification No. 2435-CPR-8605159, ISO 9001:2015 Quality Management System Certification (No. 18624Q00169R0M, valid through June 2027), and verified RoHS chemical compliance.
Plan Your Dynamic Roller Storage Project With Senior Factory Engineers
Eliminate operational bottlenecks, recover up to 65% of wasted warehouse floor area, and optimize your supply chain with precision-engineered pallet flow and dynamic heavy-duty racking systems. Direct factory pricing, certified materials, and complimentary structural CAD design.
Send an Inquiry