Radio Shuttle FIFO
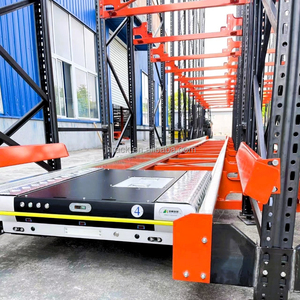
China Automatic Shuttle Rack Manufacturer Factory Warehouse Shuttle System
- Payload: Up to 1,500 kg/pallet
- Speed: 0.8 to 1.1 m/s loaded
- Control: RF tablet & WCS integrated
Manufactured in our 30,000 m² ISO 9001:2015 & CE-certified Guangzhou fabrication complex. Optimized for inventory cycle integrity, maximum density, and seamless material handling.
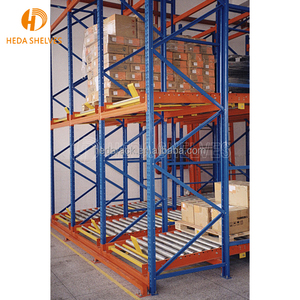
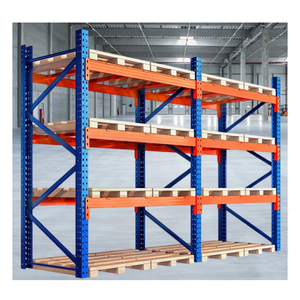
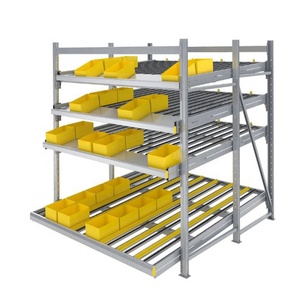
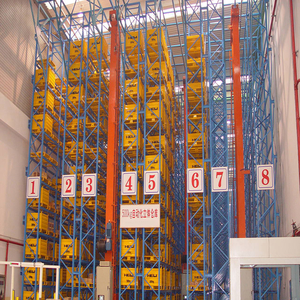
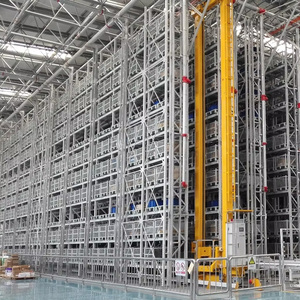
A rigorous comparative analysis of dynamic storage architectures: mechanical gravity flow, semi-automated radio shuttles, and integrated AS/RS solutions for mission-critical logistics.
Pallet flow racks utilize inclined roller lanes engineered at an exact gradient of 3.0% to 4.5% (approx. 1.7° to 2.6°). Pallets advance by gravitational kinetic energy from the replenishment loading aisle down to the pick face, creating separated operational aisles.
Shuttle systems replace inclined physical rollers with high-tensile longitudinal guide rails. Independent battery-powered robotic shuttles navigate beneath pallets along deep channels, executing micro-lifting and high-speed horizontal transfers under digital WMS instruction.
Targeted for high-density split-case picking, carton flow racks incorporate modular thermoplastic wheel tracks or continuous aluminum roller tracks mounted within adjustable upright bays. Tilted beds gravity-feed bins and tote boxes directly to manual or robotic picking zones.
Dynamic FIFO systems withstand severe cyclic fatigue loads and impact inertia unknown to static selective racking. Our Guangzhou factory utilizes certified Q235B and Q355B structural steel coils. All load beams undergo finite element analysis (FEA) verification to ensure beam deflection under maximum working payload does not exceed 1/200th of the clear horizontal span (L/200), with safety factors strictly calculated ≥ 1.65.
| System Type | Structural Principle | Space Utilization | Throughput Speed | Energy Dependency | Optimum Use Case |
|---|---|---|---|---|---|
| Pallet Flow Racking | Gravity incline (3–4.5%) with brake rollers | 80% – 85% | High (Continuous) | Zero (100% Mechanical) | Fast-moving food, beverage, pharmaceuticals |
| Radio Shuttle System | Robotic motorized platform on level tracks | 85% – 92% | Very High (Automated) | Lithium Battery Carrier | Cold storage, bulk manufacturing, low-SKU lanes |
| Carton Flow Racking | Gravity roller tracks for totes/boxes | 65% – 75% | Ultra-Rapid Manual | Zero (Passive) | E-commerce fulfillment, assembly kitting lines |
| Unit-Load AS/RS | Stacker crane mast with automated forks | 90% – 95% | Maximum (Computerized) | Grid-Powered 3-Phase | Mega distribution hubs, dark warehouses, 24/7 ops |
Market dynamics, raw material traceability, cold chain integration, and automated warehouse convergence shaping the 2025–2030 industrial storage horizon.
Refrigerated warehouse real estate costs 300% to 500% more per cubic meter than ambient facilities. Buyers are shifting heavily toward high-density Radio Shuttle FIFO and Pallet Flow layouts to condense refrigerated cubic footage.
Metallurgical Requirement: Extreme cold environments induce steel embrittlement. Tier-1 Chinese plants utilize specialized low-temperature impact-resistant steel and formulations of epoxy powder curing that prevent micro-cracking at sub-zero temperatures.
FIFO carton flow and pallet dynamic racks are increasingly paired with vision-guided Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). Modern racks feature laser-cut datum targets, hardened lead-in ground shoes, and sensor brackets.
Dimensional Precision: Millimeter tolerances are essential. Frame plumbness and floor track straightness must stay within ±1.5mm across 30-meter continuous runs to prevent robotic handling aborts.
Global corporations demand comprehensive environmental product declarations (EPDs) and RoHS-compliant coatings. Lead-free, heavy metal-free powder coatings applied via zero-effluent electrostatic application lines ensure compliance with worldwide ESG mandates.
Dematerialization via FEA: By optimizing cold-rolled upright omega (Ω) profiles with variable hole punching pitches (e.g. 50mm, 75mm), structural strength is increased while unnecessary raw steel mass is trimmed.
From prime hot-rolled steel coils to fully pre-treated and electrostatic powder-coated structural components: rigorous 10-stage quality-controlled production.










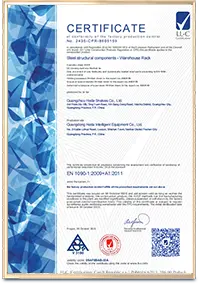
No. 2435-CPR-8605159
Standard: EN 1090-1 / EN 15512
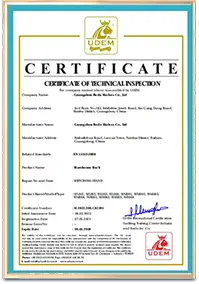
No. 18624Q00169R0M
Audited Quality Management
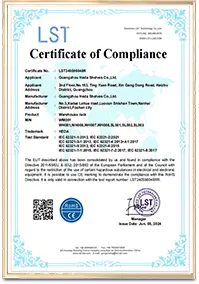
Directive 2011/65/EU
Non-Toxic Surface Coatings
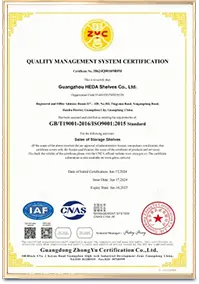
Standard: FEM 10.2.02
Dynamic Cycle Fatigue Tested
Expert engineering insights regarding slope geometries, pallet compatibility, seismic engineering, and global logistics packaging.
Collaborate directly with our technical design team. We provide complete 2D CAD engineering layouts, 3D photorealistic renderings, and structural deflection calculations within 24–48 hours, free of charge.
Speak directly with our senior racking systems specialists to review your warehouse architectural floor plan.
Inquire Now