Engineered High-Bay Racking & Material Handling Systems
Custom fabricated with premium cold-rolled steel, custom electrostatic powder coating, and precision roll-formed geometries to ensure absolute structural integrity under extreme continuous loads.
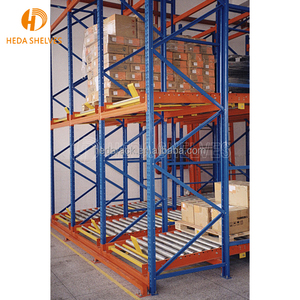
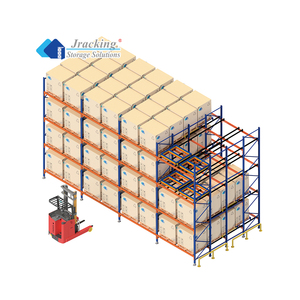
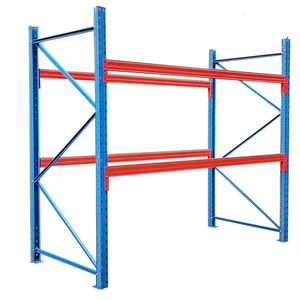
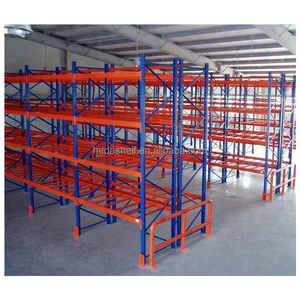
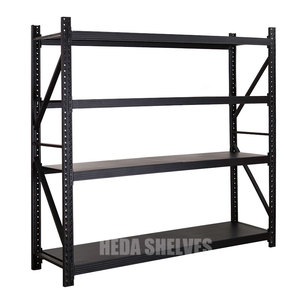
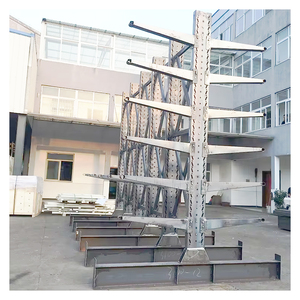
Engineering Architectural High Rack Storage: Structural Physics & OEM Standards
High rack storage warehouse manufacturing involves far more than straightforward steel stamping. Operating at heights ranging from 8 meters to beyond 40 meters within automated high-bay facilities (AS/RS), modern high rack infrastructure must withstand dynamic seismic shocks, continuous forklift column deflections, wind load transfers (in rack-clad facilities), and asymmetric heavy static stresses. A structurally sound OEM/ODM configuration requires precise metallurgical calibration, sophisticated cold roll forming profiles, and multi-stage anti-corrosion treatments.
Upright Profile Geometries
Multi-bend cold-formed Omega (Ω) profiles engineered with up to 12 distinct load-bearing facets, vastly enhancing torsional resistance compared to conventional generic channel sections.
Chemical Pretreatment
Immersion-grade pickling and iron phosphating clean raw coil surfaces of scale and oils, creating an optimal phosphate conversion matrix prior to thermoset polyester electro-deposition.
Connector Locking Systems
Heavy interlocking connectors equipped with 3 to 5 heavy-gauge prongs, secured by zinc-plated safety pins rated to exceed 10 kN shear capacity against accidental vertical dislodgement.
| Racking Architecture | Floor Space Utilization | Direct Selectivity | Forklift / Automation Interface | Typical Investment Vector |
|---|---|---|---|---|
| Selective High Rack | 40% – 50% | 100% Instant Access | Counterbalanced, Reach Truck, VNA Turret | Low Initial Capex / Versatile |
| Double Deep System | 55% – 65% | 50% Immediate Access | Pantograph Reach Truck | Medium / High SKU Density |
| Drive-In / Drive-Thru | 65% – 75% | Low (Batched LIFO/FIFO) | Standard Forklift (Protected Cab) | Economical for Bulk Commodities |
| Push Back Racks | 60% – 70% | Lane Selective (LIFO) | Standard Counterbalance / Reach | Medium-High / No Specialized Trucks |
| Radio Shuttle High Rack | 75% – 85% | Lane Selective (FIFO/LIFO) | Semi-Automated Wireless Pallet Runner | Moderate Capex / High Energy Savings |
| AMR / AGV Automated (AS/RS) | 85% – 95% | 100% Dynamic Direct Control | Autonomous Mobile Robotics & Cranes | Enterprise Tier / Ultra-Low Labor |
Global Procurement Trends: Navigating Supply Chain Resiliency (2026–2030)
The procurement landscape for industrial warehouse racking has fundamentally shifted. Global supply chain shocks, dramatic regional changes in industrial real estate costs, and aggressive warehouse automation investments are reshaping how Fortune 500 logistics directors, 3PL aggregators, and warehouse EPC contractors evaluate OEM/ODM partners. Moving beyond basic per-kilogram raw steel quotes, institutional buyers now assess long-term structural resiliency, container volume optimization, and field-assembly velocity.
1. Automated Material Handling & Robot Compatibility (AMR/AGV Interface)
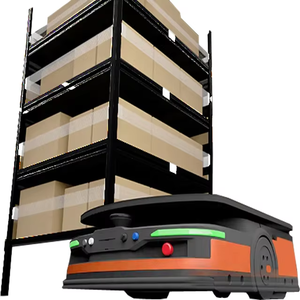
Modern high racks must integrate seamlessly with automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). Deflection allowances acceptable under manual forklift handling can trigger emergency stop sequences or calibration faults in robotic sensor arrays. Modern manufacturing demands beam deflection tolerances tighter than 1/200th to 1/300th of clear span, along with laser-calibrated rail levels for high-speed shuttles.
2. Tropicalized Coatings & Microclimate Resilience
With industrial expansion across coastal hubs, equatorial logistics corridors, and high-humidity maritime ports, paint degradation has become a major operational liability. Leading OEM factories are shifting from basic single-coat paints to multi-stage pretreatments. Hot-dip galvanized components (BS EN ISO 1461 compliant) or thermoset zinc-rich primers coupled with pure polyester architectural powders are now standard requirements to prevent corrosive under-creep in non-climate-controlled facilities.
3. Freight Densification & Knock-Down (KD) Architectural Design
Ocean shipping logistics remain a volatile overhead variable. OEM factories that treat container optimization as an engineering priority provide a decisive total cost advantage. Custom upright nesting profiles, boltless multi-piece modular baseplates, and split-frame designs allow manufacturers to ship up to 26–28 metric tons within standard 40HQ ocean containers without shipping empty air, lowering the landed cost per pallet position by 18% to 27%.
Guangzhou Heda Shelves Co., Ltd. — Engineering Precision Since 2001
Operating a modernized 30,000 square meter manufacturing base with over 300 experienced engineers and skilled technicians, HEDA Shelves stands as a benchmark OEM/ODM facility. With an established monthly fabrication capacity reaching 30,000 tons and more than 10,000 successfully delivered warehouse projects globally, we bring structural precision, turnkey CAD/3D optimization, and reliable container-optimized logistics directly to industrial developers worldwide.
25 Years Direct Expertise
Continuous refinement of high rack tooling, dynamic slotting systems, and high-bay cold roll forming technologies across two decades of manufacturing.
Full-Spectrum Certifications
Independently verified compliance under CE Certification No. 2435-CPR-8605159, ISO 9001:2015 Management Systems, and strict European RoHS criteria.
Complimentary 3D & CAD Design
Full engineering validation including structural load calculations, slab pressure analysis, and photorealistic 3D warehouse simulations before cutting steel.
Controlled Ten-Stage Factory Production Workflow
Quality assurance is embedded at every stage of the raw steel transformation. From verified structural mill coils to container de-stuffing at the jobsite, our factory executes rigorous dimensional, chemical, and coating tests.
Frequently Asked Questions: High Rack Storage Warehouse Procurement
What engineering variables are required to generate an accurate warehouse layout and structural quote?
How do OEM and ODM capabilities differ in heavy-duty high rack production?
How do factory-applied finishes prevent structural corrosion in harsh industrial or coastal environments?
What structural safety factors are engineered into your high-bay uprights and load beams?
How are oversized upright frames packed to avoid freight damage and excessive container costs?
Design Your High-Bay Warehouse with Certified Structural Engineers
Submit your warehouse floor plans, target pallet counts, and building parameters. Our design team will return a complete CAD layout, 3D structural model, and itemized factory-direct quote within 24 hours.
Contact Us