30,000 m²
Factory Infrastructure
25+ Years
Manufacturing Heritage (2001)
30,000 T
Monthly Steel Output
CE & ISO
Certified Rigorous Testing
High-Performance Dynamic Warehouse Racking Systems
Engineered to maximize storage cube density, streamline FIFO inventory replenishment, and eliminate picker travel times. Explore core structural configurations manufactured under ISO 9001:2015 standards.
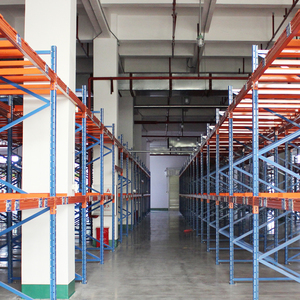
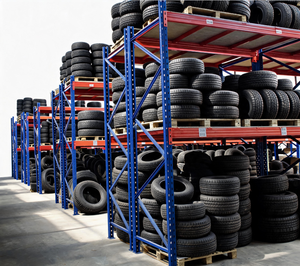
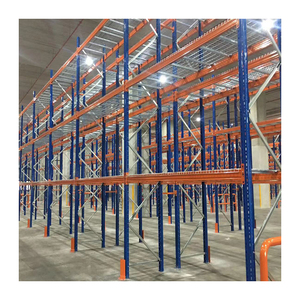
Carton Flow & Pick Flow Systems: Mechanics, Physics & Kinematics
A rigorous review of dynamic gravity feed technologies, pitch dynamics, roller materials, and carton presentation interfaces in modern multi-tier fulfillment operations.
Defining True Pick Flow Rack Engineering: Beyond Static Shelving
In modern material handling vocabulary, Pick Flow Racks (frequently referred to as Carton Flow, Gravity Flow, or Dynamic Picking Racks) represent a sophisticated, zero-energy mechanical conveying and storage hybrid. Unlike static selective shelving where picking operatives must traverse lengthy access aisles and fight for slot access against replenishment stockers, pick flow racks decouple loading from retrieval. replenishment takes place on the rear charge side, while order selectors pull product uninhibited from the front discharge face.
The underlying principle relies on a calibrated gravitational slope—typically engineered between 2.0° and 4.5° (approximately 3/8" to 7/16" pitch per linear foot). As an operator extracts the forward-most carton or tote, the trailing unit immediately glides into the pick position by force of gravity. This self-indexing action maintains a perpetually packed pick face, slashing picker walking distances by up to 75%, boosting pick rates from 60 lines/hour to over 250 lines/hour, and ensuring strict First-In, First-Out (FIFO) stock turnover, an absolute prerequisite for perishable food, pharmaceuticals, and fast-moving retail consumer goods (FMCG).
Wheel Bed vs. Dedicated Roller Track
Full Wheel Beds utilize staggered arrays of high-density polyethylene (HDPE) or polypropylene skate wheels spanning the entire shelf width. This layout offers infinite slotting agility: when carton dimensions change, dividers are re-pinned without tool downtime. In contrast, Dedicated Steel Roller Tracks offer superior impact endurance for uniform tote containers and ultra-heavy payloads up to 150 lbs/linear foot.
Pitch Calibration & Hydrodynamic Braking
Slope calculation is governed by the carton footprint, bottom-surface deflection, and composite weight. Soft corrugated boxes exhibit high rolling friction and sag over time, requiring a steeper gradient (4.0°), whereas rigid plastic totes roll effortlessly at 2.2°. For deep lanes exceeding 15 feet, integrated centrifugal brake rollers throttle terminal velocity to avoid box-crushing collisions at the pick face.
Ergonomic Knuckle Trays & Tilt Shelves
Discharge shelf ergonomics govern operative musculoskeletal health and picking speed. By engineering a Knuckle Tray (drop-down cantilevered shelf) angled at 15° to 20° towards the picker, split-case carton contents are instantly visible. Operatives pull individual e-commerce items without twisting their wrists or bumping their heads against upper beam flanges.
Top 10 Pick Flow Rack Manufacturers & Suppliers
A rigorous industrial analysis evaluating engineering depth, fabrication scale, dynamic roller kinematics, global deployment capability, and Total Cost of Ownership (TCO).
| Manufacturer | Headquarters | Core System Specialization | Load Capacity (Per Lane) | Roller / Wheel Materials | Custom Engineering (OEM/ODM) |
|---|---|---|---|---|---|
| Guangzhou Heda Shelves Co., Ltd. | Guangzhou, China | Custom Carton Flow, Integrated Pallet Flow & Heavy Mezzanines | 50 kg - 2,500 kg | HDPE, Cold-Rolled Steel, Zinc Plated | Complete Turnkey CAD/3D in 24 Hrs |
| Interroll Group | Sant'Antonino, Switzerland | Modular Carton Flow Beds & Heavy Pallet Flow Lanes | 10 kg - 1,200 kg | Engineered Thermoplastic & Precision Steel | Proprietary Standard Modules |
| UNARCO Material Handling | Tennessee, USA | RhinoTrac, UPICK Full Bed Skatewheel Tracks | Up to 100 lbs/ft | Staggered High-Impact Polymers | Tailored Racking Integration |
| SSI Schaefer | Neunkirchen, Germany | Automated Picking Tunnels & High-Density Flow Systems | 20 kg - 1,500 kg | High-Performance Polyacetal / Polyurethane | Full Intralogistics Ecosystems |
| Mecalux, S.A. | Barcelona, Spain | Live Storage for Cartons & Pallet Gravity Racks | Up to 1,000 kg | Extruded Aluminum Tracks & Plastic Rollers | Modular Scalable Layouts |
| Bito-Lagertechnik Bittmann | Meisenheim, Germany | Order Picking Flow Racks with Integrated Return Lanes | 15 kg - 250 kg / box | Ultra-Low-Noise Technical Polymers | Standardized European Modular Carts |
| Advance Storage Products | California, USA | Quik-Pik Gravity Carton Flow Systems | Up to 50 lbs/sq.ft | Heavy-Duty Steel & Polypropylene | Custom Retrofit Drop-In Shelves |
| Mallard Manufacturing | Illinois, USA | Dyna-Flo & Cart-Track Roller Beds | Up to 120 lbs/ft | Staggered Plastic / Heavy Polycarbonate | Engineered Roller Pitches |
| Gonvarri Material Handling (Dexion) | Oslo, Norway / Europe | Industrial Dynamic Carton Flow & PTL Integration | Up to 800 kg / level | Steel Rollers, Plastic Flanged Wheels | Warehouse System Architecture |
| Kardex Remstar | Zurich, Switzerland | Dynamic Storage & Vertical Pick Face Integration | Engineered Custom | Reinforced Synthetics & Micro-Bearings | High-Density Automated Subsystems |
1. Guangzhou Heda Shelves Co., Ltd.
Top Engineering ValueOperating since 2001 from an expansive 30,000 m² state-of-the-art manufacturing campus in Guangzhou, HEDA Shelves represents the pinnacle of factory-direct heavy-duty pick flow and pallet racking supply. HEDA controls every phase from high-tensile Q235B cold-rolling and automated column punching to automated electrostatic powder coating.
- Export Footprint: 120+ Countries (Global Hubs)
- Production Prowess: 30,000 Tons / Month
- Certifications: CE (2435-CPR-8605159), ISO 9001:2015
- Key Edge: Turnkey 3D/CAD in 24h & Shipping Optimization
2. Interroll Group
Swiss PrecisionHeadquartered in Switzerland, Interroll is a globally acclaimed purveyor of dynamic internal logistics components. Their carton flow beds feature ultra-low friction roller assemblies, pre-configured side guides, and integrated speed controllers for automated picking zones.
- Key Innovation: Smart Roller Tracks & Braking
- Global Presence: Europe, Americas, Asia-Pacific
- Primary Sectors: E-Commerce, Courier Express, Pharma
3. UNARCO Material Handling
North AmericaAn American titan in warehouse storage, UNARCO is celebrated for its RhinoTrac carton flow system. Engineered with stamped steel side channels and tough structural axle assemblies, their equipment easily absorbs the impact of heavy corrugated box drop-ins.
- Key Product: RhinoTrac Full-Width Rollers
- Structural Standard: RMI Certified Fabrications
- Target Verticals: Automotive Spare Parts, 3PL
4. SSI Schaefer
Automation GiantHailing from Germany, SSI Schaefer excels in high-complexity logistics environments. Their carton dynamic pick flow shelves are engineered for integration into automated tote conveyor networks, high-bay picking towers, and semi-automated distribution centers.
- System Capability: Tote Flow & Return Run integration
- Finish Quality: High-end Industrial Powder Coating
- Target Application: Ultra-High Throughput Distribution
5. Mecalux, S.A.
Global EnterpriseWith operations covering Spain, Latin America, and North America, Mecalux provides modular live carton flow shelves equipped with adjustable plastic roller channels and snap-fit lane dividers for seamless SKU redistribution.
- Key Advantage: Adaptable Modular Shelf Connectors
- WMS Pairing: Integrated with Easy WMS Systems
- Applications: Retail Distribution, Supermarkets
6. Bito-Lagertechnik
European QualityRenowned across central Europe for its ergonomic live storage picking solutions, Bito develops curved knuckle trays, multi-tier flow rack shelving, and noise-dampening polymer rollers built specifically to handle standardized plastic picking totes.
- Ergonomic Edge: Multi-Angle Knuckle Adapters
- Acoustics: Whisper-Quiet Flow Rollers
- Market Focus: Pharma, Cosmetics, Electronics
7. Advance Storage Products
Heavy LogisticsSpecializing in deep-lane gravity flow and Quik-Pik carton flow racking, Advance Storage is a staple brand in North American grocery distribution networks requiring heavy structural steel frames that endure intense forklift interactions.
- System Feature: Drop-In Flow Track Assemblies
- Durability: Structural C-Channel Uprights
- Industry Sector: Cold Storage & Food Distribution
8. Mallard Manufacturing
Flow SpecialistsAn engineering-driven US firm that focuses almost exclusively on gravity flow racking technologies. Their Dyna-Flo wheel beds accommodate varying carton footprints without necessitating physical track realignment, ensuring high-flexibility slotting.
- Product Highlights: Dyna-Flo & Dyna-Deck Systems
- Flexibility: Full Width Skate Wheel Configurations
- Specialty: Retrofit Solutions for Older Racks
9. Gonvarri Material Handling
Dexion GroupFormed through historical engineering powerhouses including Dexion, Gonvarri offers high-density pallet and carton live storage built to stringent FEM and EN codes across the European continent and emerging African and Middle Eastern markets.
- Design Code: EN 15512 & FEM Compliant
- Ecosystem: Pick-to-Light Mounting Channels
- Applications: Automotive & Industrial Assemblies
10. Kardex Remstar
Dynamic Pick TechWhile best recognized for vertical carousel shuttles, Kardex engineers high-density dynamic carton pick modules that link buffer replenishment storage to automated mini-load cranes, achieving high transaction rates in critical supply lines.
- Focus: Semi-Automated Buffer Interfacing
- Precision: Sub-Millimeter Bearing Construction
- Verticles: Aerospace, High-Tech Electronics
Future Procurement & Technological Trends in Pick Flow Racking
How automation convergence, cold chain expansion, robotic AMR collaboration, and sustainable steel procurement are reshaping next-generation pick flow architecture.
1. AMR & AGV Pick-Face Docking
Future warehouse layouts are phasing out standard manual cart picking in favor of Autonomous Mobile Robots (AMRs). Forward-thinking suppliers design carton flow discharge brackets at standardized robot-gripper elevations. AMRs navigate to designated flow rack picking faces, auto-retrieve dynamic totes using vacuum end-effectors or optical scanning, and transport split cases directly to packing stations without human intervention.
2. Sensorized Smart Tracks & IoT
The implementation of real-time Pick-to-Light (PTL) and optical presence sensors directly onto aluminum extrusion beam channels has elevated carton flow into an active IoT endpoint. Pressure and weight sensors embedded into the last roller bay communicate inventory depletion back to Enterprise WMS platforms, instantly triggering automated replenishment tasks long before a stock-out occurs.
3. Extreme Cold Chain & Coastal Durability
With global fresh food and biologics cold-chain investment accelerating, pick flow racks must survive sub-zero (-30°C) environments without lubricant crystallization or roller embrittlement. Leading manufacturers utilize stainless steel ball bearings sealed with synthetic fluorosilicone greases and hot-dip galvanized or multi-stage phosphated epoxy powder-coatings to combat tropical and coastal humidity corrosion.
4. Modular Extrusion & Zero-Tool Reconfigurability
Volatile e-commerce SKU life cycles require rapid warehouse agility. The historical model of welding tracks into fixed frame channels is yielding to modular 6063-T5 aluminum extrusions. Clip-on lane guides, adjustable magnetic dividers, and universal hanger brackets allow maintenance teams to re-profile an entire 20-bay pick module during a weekend shift without welding, drilling, or paint retouching.
Why International Supply Chains Rely on HEDA Shelves
Eliminate intermediary markups, streamline structural engineering, and secure factory-direct supply certified to global compliance standards.
Full-Cycle In-House Fabrication
Operating across a sprawling 30,000 m² facility with 10 dedicated manufacturing lines, HEDA executes uncompromised quality control from uncoiling high-tensile Q235B cold-rolled steel through automated column punching, profile roll forming, and 100% in-house electrostatic powder coating.
Rapid Free 3D CAD & Structural Calculations
Procurement teams bypass guesswork. HEDA's engineering staff supplies complimentary CAD layout diagrams, 3D photorealistic renderings, and FEA finite-element structural deflection verifications within 24 hours of warehouse blueprint submission.
Rigorous International Certification
Every rack assembly conforms to verifiable quality protocols, holding CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Certification No. 18624Q00169R0M (valid through 2027), ensuring flawless compliance for tier-one project tenders.
Container-Optimized Ocean Packaging
Engineered knock-down bundling profiles are calibrated for maximum volumetric fill rates in 20GP and 40HQ ocean containers. Every component ships with bilingual numerical indexing and step-by-step schematics for fast, error-free assembly.
Pick Flow System Selection Matrix for Logistics Engineers
Selecting the optimal track configuration requires balancing box contact surface chemistry, weight distribution, and SKU volatility.
| Dynamic Bed Type | Optimal Load / Unit | Compatible Container Types | Pitch Requirement | Capital Cost Index | Best Fit Application |
|---|---|---|---|---|---|
| Full Staggered Skate Wheel Bed | 5 - 35 kg / box | Varied Corrugated Boxes, Rigid Totes | 3.0% - 4.5% (approx 2° - 2.5°) | $$ (Moderate) | High-SKU E-commerce fulfillment with frequently fluctuating package footprints |
| Polymer Roller Track (Dedicated Lane) | 10 - 60 kg / container | Standard Euro Totes, Plastic Crates | 2.0% - 3.0% (approx 1.2° - 1.8°) | $ (Economical) | Automotive kitting, electronic sub-assembly lines with uniform plastic return totes |
| Zinc-Plated Steel Roller Bed | 50 - 250 kg / box | Heavy Wooden Crates, Metal Tins, Foundry Parts | 2.5% - 3.5% (approx 1.5° - 2.0°) | $$$ (High Industrial) | Mining consumables, machine tool stores, bulk hardware & lubricant container storage |
| Knuckle-Tray Carton Flow Module | 5 - 30 kg / case | Open-Top Corrugated Cases, Broken-Case Bins | 3.5% incline + 15° Knuckle | $$$ (Specialized) | Pharmaceutical split-case order picking, cosmetic retail batch picking centers |
Frequently Asked Questions: Industrial Pick Flow Racks
Authoritative technical, logistical, and structural answers to simplify engineering design, import logistics, and operational commissioning.
What is the exact formula for determining the slope angle (pitch) of a carton flow rack?
Slope (%) = (Elevation Drop / Lane Depth) * 100. In standard practice, a slope of 2.5% to 4.0% (equivalent to 5/16" to 1/2" per linear foot) is engineered. Corrugated boxes with soft bottoms or humidity-induced sag require a 3.5% to 4.2% pitch, while hard, flat-bottomed polymer totes operate smoothly at 2.0% to 2.5%. During pre-engineering trials, HEDA runs physical dynamic slide tests using customer carton samples to verify restart performance (ensuring a box stopped midway resumes motion upon front extraction).
How do skatewheel bed systems compare against full-width steel roller tracks?
How are pick flow rack systems protected against severe coastal humidity and temperature extremes?
Can pick flow racks be retrofitted into existing selective pallet rack upright frames?
What parameters are required by HEDA engineering to calculate a free CAD layout and load quotation?
- Building dimensions: Clear warehouse height to ceiling truss, column grid spacing, door/aisle positions.
- Carton / Tote specifications: Length, Width, Height, and Minimum/Maximum loaded weight per SKU.
- Throughput expectations: Number of unique SKUs, desired lane storage depth, daily picks per line.
- Interface mode: Split-case knuckle tray picking, full-case conveyor takeaway, or integrated pallet reserve.
- Port of destination for container packaging optimization and landed freight estimation.
What international engineering standards and structural codes do HEDA racking systems comply with?
Ready to Engineer Your High-Throughput Pick Flow System?
Submit your warehouse floor layout, carton dimensions, and load requirements. Receive a comprehensive CAD floor plan, 3D structural model, and factory-direct export proposal within 24 business hours.